Solution Finder
SOLUTION FINDER

Ihr Wegweiser durch die
Rösler-Produktwelt

Mit nur wenigen Klicks finden Sie die richtige Maschine fĂŒr Ihre Belange!

Ergebnisse: 237 Artikel

A Holistic Look at Automated Blasting in the Modern Metal Fabrication Shop

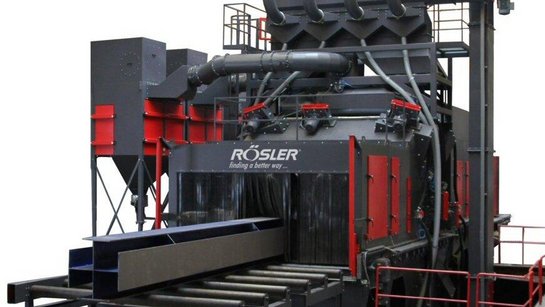
Written by Rosler CEO Bernhard Kerschbaum, this article was originally published in The Fabricator . Modern metal fabrication operations aren’t like the fab shops of old. Many are clean, well lit, with employees working in fresh, filtered air. Yes, some operations in fabrication are, well, just plain dirty—and manual blasting is a prime example. The work isn’t pleasant, requires protective gear, and if the booths aren’t maintained or set up properly, they can constrain workflow in a serious way. Options in blasting automation abound, but before diving into all that technological wizardry, try laying some groundwork by answering a fundamental question: What must the blasting operation accomplish? Shot Blasting Versus Shot Peening Shot blasting (or just “blasting” if using a different media other than shot) prepares a metal surface while shot peening aims to change the metal’s properties (see Figure 1 ). Certain aerospace applications require precise levels of stress relief (or other changes to material properties), and they use specialized shot-peening technologies to achieve it. Precision shot peening of landing gears is a prime example, with the process optimizing surface stresses, eliminating microcracks and the stress risers around them. Most metal fabricators employ blast cleaning for the vast majority of their applications, cleaning and preparing a metal surface for the next manufacturing step, usually painting. If a beam or plate isn’t blasted correctly, paint won’t adhere properly. However, some fabrication operations do employ a kind of peening—not as precise as high-end peening applications, but it’s peening nonetheless, with the media impacting the surface and causing compressive stresses that aim to change the material’s properties. Imagine fabricating a bowl that will be used in a high-vibratory setting. The welds within those bowls need a certain amount of stress relief, and shot peening helps accomplish this. To ensure adequate stress relief for the welds, the application might choose to use large shot, which can have a peening effect that penetrates deeper into the surface. Alternatively, the operation might choose to use the same shot that it uses for blast cleaning applications, though extending the cycle time to achieve the required peening effect within the part. When to Blast? Again, the majority of fabricators need to prepare a workpiece surface for a downstream operations like painting—so, they’re blasting (not peening). The higher quality the end finish is, the more important surface preparation becomes. Put another way, a high-quality, highly consistent coating requires a high-quality surface preparation. An automotive car panel requires very different surface prep compared to a structural beam. Where in the manufacturing sequence does it make the most sense to blast? Are cut plates being blasted to prepare them for downstream processes, or will the completed fabrication be blasted after bending and welding? Applying blasting to incoming material might seem counterintuitive, especially if welds need to be blasted anyway. After all, most operations that employ blasting do so just before it enters the final coating process. Still, blasting needn’t always occur at the end of the value stream. Sometimes, cleaner material coming into the shop can help downstream processes like cutting and welding, and it might help streamline the final finishing operation significantly. Some operations might choose to automate the blasting of incoming material yet keep the final blasting of welds manual, before the work enters the final coating process. The operation isn’t entirely automated, but because incoming material is clean, overall throughput rises dramatically, and time and labor required for manually blasting the fabricated parts is significantly reduced. Coating also doesn’t necessarily need to occur at the very end of production. For instance, some shipyards blast incoming plate, prime them with a weldable primer, then weld. Afterward, the work is blasted again—but only the welded seams. For large workpieces especially, such a manufacturing sequence helps streamline the overall operation significantly. Blasting Variables The industry has various standards (such as those from SSPC and NACE) to help fabricators assess the surface condition of material. The cleaner the material, the less aggressively you need to blast it, and the less aggressive blast media you need to use to achieve the desired finish. When working with plate with significant rust, shot might need to be larger, or the application might call for grit, which is angular. Round shot usually produces a finer finish than grit, but grit might be required to produce a rougher surface profile for adequate adhesion for a thick coat of paint. FIGURE 1. For fabricators requiring shot peening, for weld stress relief or any other application involving a change in material properties, maintaining the proper mix of media is critical. Fractured and undersized media must be continuously and consistently removed from the peening system. Consider the condition of raw stock and the final finish required—that is, what’s delivered versus the final surface finish you need to achieve before the product ships. The difference between the incoming and outgoing material quality determines the blasting throughput. The greater the difference in quality (that is, very rough to a fine finish), the longer the blasting will take. Some applications also might require several blasting stages, the first to clean and another secondary stage, using finer blast media to dial in the surface’s paint adhesion characteristics. “Speed” in blasting can be defined several ways. First, how much shot needs to hit the surface at a given time, and how often the shot needs to strike to remove rust and prepare the surface as needed? The more rust a workpiece has, the more shot it will require. One turbine might throw 500 lbs./min. of shot at a slow-moving workpiece, to ensure enough shot strikes the surface enough times to create the surface finish needed. Alternatively, a system can have multiple blast wheels, positioned one after the other, that throw (altogether) 1,500 lbs./min. to the surface, which allows parts to travel three times as fast. There’s a limit to this, of course. Throw too much shot, and the shot media begins to ricochet within the system, which in turn creates all sorts of inconsistencies. Thrown at a high enough volume, the blast media itself loses its effectiveness. Several variables control blast intensity. An operation can adjust the feed valves to control how much media flows onto the turbine. Alternatively, an operation might slow the turbine speed, so the blast media itself hits the part at a slower velocity. An application has an optimal exit velocity; too low, and the media isn’t effective (for instance, it fails to knock off surface rust); too high can cause other issues, like warping, especially for very thin workpieces. Another variable involves blast media size distribution. Automated systems have recycling systems that separate the blast media from the removed rust and debris. The recycling system itself is extremely critical; if it’s not operating properly, the blast media won’t be consistent, which can lead to paint adhesion and other challenges. Shot becomes smaller and smaller as it’s recycled. The blast media recycling system must be monitored to ensure enough fresh shot or other media is added to the mix, and that the screening system (which evacuates fine particles) is working properly. The procedure isn’t complicated. Operators essentially take a blast media sample and send it through several specially designed sieves, so they can see the coarseness distribution and any debris or contaminants that might be present. Anatomy of a Blast Machine Blast machines carry the parts through the blast stream, collecting as little media as possible on the part while also exposing every surface that needs to be blasted. The blast stream the turbine throws has a “hot spot” near the center, an area where the blast media carries the most energy. This in turn governs the optimal position of the turbines (see Figure 2 ). For instance, a blast machine that processes plate requires even distribution of blasting across the surface, and if those hot spots in each blast stream don’t overlap, the plate might end up with “stripes” in areas exposed to less blast media. These basics form the foundation of any blast machine design. A popular design for metal fabrication includes roller-type machines, where widely spaced rollers (see Figure 3 ) carry plate or beams into a machine, where it’s blasted from multiple directions. Placement of the turbine is key (see Figure 4 ). Some machines might place blast turbines a certain distance away to accept, for example, various beam geometries. The arrangement might not be as efficient for plate as a machine with turbines placed closer to the work, but the arrangement does offer flexibility—that is, the system can process both flat plate and beams of various shapes and sizes. FIGURE 2. Turbines emit overlapping blast streams to ensure all workpieces receive sufficient coverage. Again, when the work is blasted plays a role too. That flexible machine might blast raw plate to clean and prepare it for downstream processing, then blast the assembly after welding. A shop might employ this strategy because of blast media access issues (that is, a machine’s blast media can’t access all surfaces of the assembled product), or because welding requires clean surfaces that the blasting process produces. Alternatively, the company might choose to “blast twice”—both incoming stock and welded products—because it’s still the fastest, most efficient way to process the work. Cleaning raw stock as it comes in streamlines downstream operations. And because parts were already cleaned, blasting of the welded assembly takes less time. Which machine a fabricator chooses depends on the application requirements, including the part geometry. Flat parts or beams might be adequately blasted on a roller-type machine, while booms, buckets, or other complex shapes might call for a hanger-type or spinner-hanger-type machine. A bucket sent through a roller machine might start accumulating shot on its surface, which prevents the shot from hitting the surface with sufficient energy. In this case, a spinner-hanger blast machine, where a ring of blast turbines around a hung part that’s spinning, might be able to access all surfaces while still allowing the spent shot to fall from the part. The manual blast room’s principal benefit is operator access. The operator can blast all surfaces and brush off accumulated shot as needed. An automated system might not have this flexibility. At the same time, blast media from a turbine within an automated machine has much more energy than blast media from a manual gun. That energy can reduce the media buildup significantly. So, while a manual operator might be able to blast complex, challenging geometries, he also might have to brush off accumulated media more frequently. (Note: manual touchup blasting can be integrated into an automatic blast machine, such as a hanger-type machine. In that case, the operator suits up and blasts the part with a manual blast wand inside of the disabled blast machine.) On the other end of the spectrum, some blasting technologies offer complete automation—and not just of the entire blasting process. Some plate and beam blasting systems connect directly to a painting system (see Figure 5 ). Again, these help minimize the required surface prep later in the value stream. At the steel supplier or at the fabricator itself, beams and plates are blasted then immediately coated with a weldable primer. Such systems also can come with a cleaning station before blasting—especially useful for structural fabricators that store their material outside. That station removes the loose debris (like dirt, snow, and leaves) before the beams enter the blasting station. After blasting, the work passes through a cleaning station with brushes and air blowers, which remove any remaining shot or other debris before the pieces flow to painting and drying. Throughput for these systems depends on the material condition entering the machine as well as the painting requirements like thickness, consistency, and curing time. Designers of such systems have optimal throughput in mind. If curing time takes longer, then the blasting system could be altered to run slower (slower turbines, less media, or a combination of both). At the same time, not every workpiece need be sent through the painting system. For instance, a fabricator that cambers beams or forms plates downstream wouldn’t want to paint those pieces upstream, so those workpieces that undergo those processes could simply be blasted and then quickly sent through the idle painting system, then on to cambering or forming. Again, it’s about overall throughput, not the “local efficiency” of a specific blasting or painting process. Yes, blasting might take a little longer when coupled with painting, and the painting system might not be used for every beam. But linking painting directly to blasting boosts overall flow and minimizes work-in-process—both of which represent huge time savings. The result: The shop blasts and paints more material in less time using fewer resources. About the Entire Value Stream In applications with widely varying or complex part geometries, a fabricator might choose to partially automate blasting, with a machine blasting 80% or more of the material surface and a manual operator blasting the remaining 20%. Automating the entire process is, of course, ideal for many applications—but not all. The idea is to implement automated blasting where it can be most effective. In other situations, the operator might need only to blow blast media off. Certain hanger-type systems, for instance, have a designated cleaning station where operators, for parts that require it, can perform a final cleaning before the part moves on to the next stage (see Figure 6 ). FIGURE 3. Widely spaced rollers carry plate, beams, or similar workpieces through into the machine. The aim is to streamline the entire value stream, and this extends up to material purchasing. A fabricator could buy more expensive material that requires less blasting or no blasting at all, or it could buy less expensive material that requires significant blasting and surface preparation. However, what if the welds require blasting regardless of material quality? As long as application requirements can be met, it might make more sense to purchase the less expensive raw stock, spend more time blasting, and yet (thanks to less expensive material) save money overall. A high-volume fabricator might even choose to bring an automated blasting and painting line in-house, not only because it increases throughput, but also because it allows the operation to purchase less expensive material and gain greater control over material surface quality—depending, of course, on the final application requirements. Some structural beam processing operations have effectively automated their entire flow, from blasting to cutting, painting, then loading directly onto trucks. In at least one European structural steel fabricator, one operator sits in an air-conditioned room and controls the entire operation. His main job is to monitor equipment and flag maintenance personnel should a problem arise—be it extra vibration on a blast turbine (detected through sensors), a blade vibration issue at the band saws, or anything else. Developing such systems didn’t occur overnight, and it didn’t happen by analyzing specific processes in isolation. Considering the entire value chain is key, including linkage with enterprise resource planning as well as the potential of AI-driven predictive maintenance. When this happens, fabricators often find they can take automation to new heights. FIGURE 4. A blast machine's turbine wheels (three of them just above the work entrance) are placed to accept a variety of workpiece geometries. FIGURE 5. In this setup, beams or plates are blasted, cleaned, then flow directly to painting for a weldable primer. FIGURE 6. Some systems offer automated blasting together with a manual cleaning station.

Partnership Provides Excellent Finish for Deep-Drawn Medical Components

Deep-drawn functional components are increasingly being utilized in the production of medical and pharmaceutical products. To meet the strict standards for manufacturing and quality management in the field of surface finishing, Hubert StĂŒken GmbH & Co. KG has relied on mass finishing solutions and consumables from Rosler for more than 30 years. Founded in 1931, Hubert StĂŒken GmbH & Co. KG is a family-owned business with manufacturing operations at five locations in Europe, Asia, and the United States. Its product range includes stamped and bent parts, plastic-coated components, and complex assemblies. Rosler works with StĂŒken Medical , the company’s medical business division which focuses on medical and pharmaceutical engineering, to meet the increasing demand for deep-drawn metal components. Andreas Hellman, Manager of the ISO 13485-certified business division, explained, “Components used in the field of medical and pharmaceutical engineering must meet strict quality standards. The same strict standards apply also to the actual production operations. For this reason, we have pooled the required know-how for the development and production of such precision components at StĂŒken Medical.” The Situation Among other items, this division produces complex housings and assemblies, valves, extremely precise micro parts, and primary packaging. These components are made from metals suitable for deep drawing, including stainless steel, aluminum, and titanium. To meet the strict quality standards in the medical and pharmaceutical industry, the company utilizes multi-stage cleaning systems and operates two class 7 cleanrooms. Its research and development department, located at the corporate headquarters in Rinteln, Germany, continuously explores the possibilities to expand the range of processes and materials. “For many of our customers, we are a development partner,” Hellmann said. “To perfectly adapt new products to their intended use, we are not only working with our customers but are also cooperating with partners from various technological sectors.” The Solution When it comes to issues around surface finishing that can be resolved by mass finishing, the company has relied on Rosler’s experience and know-how for more than 30 years. “Our long partnership is based on the excellent quality and reliability of Rosler equipment and consumables,” Hellmann said. “This helps us to ensure that the required results are achieved in a consistent manner.” Dirk Schulz, Project Engineer at StĂŒken, agreed. “When it comes to the joint development of finishing processes, we especially value Rosler’s flexibility and expertise,” he said. “In this respect, our access to the Customer Experience Center in Untermerzbach is extremely valuable. “Rosler also supports us with documentation and equipment details required for machinery and processes that must be qualified and validated in line with ISO 13485,” Schulz said. At its manufacturing locations around the world, this deep-drawing specialist uses 15 rotary vibrators and 10 centrifugal disk finishing machines for its finishing operations. StĂŒken Medical also operates 18 process water centrifuges for eco-friendly and reliable cleaning and recycling of the process water. Rotary vibratory machine with work pieces in the media mix The Requirements The deep-drawn components are generally characterized by an extensive degree of material shaping, complex geometries, and extremely small dimensions requiring high dimensional accuracy and especially demanding specifications for deburring , edge radiusing , and polishing of external and internal work piece areas. Equally challenging are the surface roughness and surface quality requirements. “On the one hand, we must ensure that all pieces within a work piece batch receive the same high-quality surface finish. On the other hand, the work pieces must not be damaged or deformed,” Schulz said. “Last but not least, after completion of the finishing process, the work pieces and media must be reliably separated. A carry-over of the work pieces and/or media into the next batch must be prevented at all costs,” he added. In conjunction with polishing jobs, the work piece surface must frequently be marked with a UDI code. Fully meeting these specifications requires finishing processes that are precisely tailored to the respective work pieces as well as carefully adapted equipment and consumables. Conducting special feasibility studies is often required to determine system parameters. Deep drawn component made by StĂŒken The process for radiusing the edges of 0.8 in (20 mm) stainless steel housings for a medical device was developed in close cooperation with StĂŒken. This delicate housing’s large surface area in combination with extremely thin walls posed a challenge. To remove sufficient material at the edges, a high processing intensity that could be tightly controlled was required to prevent any deformation. The Cooperation The Customer Experience Center at Rosler is equipped with ultra-modern machines capable of running a wide variety of different finishing processes and conducting trials to define the most suitable equipment technology under actual production conditions. During such development processes, the processing bowl of standard machines must be frequently modified, sometimes involving substantial engineering changes. For this project, the comprehensive mass finishing experience at StĂŒken was a valuable source of ideas. To guarantee a reliable and complete separation of the finished work pieces from the media, the finishing equipment for StĂŒken Medical required a few changes in the separation process. Another goal of processing trials is the determination of the optimal media shape and type ( ceramic or plastic ) for the finishing task at hand. In order to achieve consistently good surface finishes, very often the media must have extremely tight dimensional tolerances. Deep drawn component made by StĂŒken All ceramic and plastic media are produced at Rosler in compliance with the highest ecological standards. With over 15,000 different products, the media, compounds, and process water cleaning agents Rosler offers are by far the largest range of mass finishing consumables in the world. A key factor in the development of successful finishing processes is the perfect interplay between the right equipment technology and the right consumables (media and compound). Generally, the best results are achieved by close cooperation with the customer. The Rosler Way Decades of experience and the ability to design, service, and maintain machines as well as provide the consumables and accessories required to get the finish you require make Rosler a well-rounded, single source for surface finishing expertise. Contact us to discuss your mass finishing needs.

Interlinked Mass Finishing and Cleaning Systems Half Processing Time

Because of a positive experience with four continuous flow washing machines operating at its headquarters, VIA OberflĂ€chentechnik (VIA) decided to work with Rosler for a comprehensive mass finishing and cleaning operation. The resulting interlinked system meets the most demanding cleanliness specifications while achieving significant cycle time reductions and cost savings and providing a high degree of operational flexibility. The Situation Headquartered in Lennestadt, Germany, VIA sought an integrated solution for de-oiling, mass finishing, and deep cleaning of stamped and formed parts. Since its founding in 1996, the job shop company has been one of the leading work piece cleaning specialists in Europe. Its three production locations process automotive and other components. An in-house laboratory ensures that the treated work pieces are in full compliance with the specified cleanliness demands. Depending on the stringency of the customer requirements, some products are even packed in a dedicated cleanroom. After extensive cleaning trials with pilot production runs, VIA received a large order from an automotive supplier for volume cleaning of clutch carriers. The company's existing cleaning and mass finishing capacities were no longer sufficient and had to be further expanded. Rosler mass finishing system The Solution “Right from the project start, it was clear that we would purchase a new mass finishing system from Rosler," said Kai Lechner, Manager at VIA. "We were not certain about buying the water-based cleaning systems from the same supplier, but after inspecting a fully automatic combined mass finishing/cleaning system that has been successfully running at an automotive supplier for several years, we decided to purchase the complete package from one supplier, namely Rosler," he said. Utilizing the Rosler team as the single supplier and integrator for the interlinked system provided numerous benefits. Since Rosler not only produces the finishing equipment, but also the washing systems, our extensive experience in integrating robotics allowed us to provide a turnkey solution for VIA. Based on prior successful partnerships with Rosler, VIA also knew we had the expertise and experience to be responsible for the process, minimizing the need for coordinating with different vendors and providing one point of contact for a complex project. VIA's new line consists of two cleaning units, a linear continuous flow vibratory inline system , and an automatic process water cleaning system ; all supplied by Rosler. The company also purchases its grinding media as well as all cleaning and finishing compounds from Rosler. “For us, it is a lot easier to deal with one partner who takes care of everything including service and maintenance," Lechner said. The Process For the de-oiling stage, the clutch carriers are manually placed on the feeding conveyor of the compact spray-rinse washing machine. During the 6-second cycle, they pass through two separate cleaning zones and one blow-off station. Filtration units and a coalescence separator increase the clean liquid systems' uptime utilized in the initial step. A single media is used in the various cleaning processes which allows the work pieces to be directly transferred into the mass finishing machine without a drying step. Deburring and edge radiusing take place in the linear continuous flow vibrator, type R 650/6600 DA. Process water used in the machine is continuously cleaned by an integrated Z1000 centrifuge equipped with fully automatic sludge discharge. A vibratory separation unit transfers work pieces from the mass finishing machine to a feeding conveyor and the deep cleaning unit parts washing system. To ensure that the work pieces meet the stringent cleanliness requirements of no metallic particles > 600 ”m, the carriers are manually positioned prior to entering the deep cleaning unit. Work pieces then pass through a cleaning zone followed by a rinsing and passivation zone. In these zones, the parts are sprayed with a cleaning solution from above and below. The pressure and volume of the water flow from the upper and lower spray nozzles can be separately adjusted, and the various parameters can be stored as individual programs in the equipment controls. After passing through a drying zone, the work pieces are discharged. Process Advantages The operational flexibility of the system allows VIA to utilize the different modules in any conceivable combination. The combined cleaning/finishing system also allows the processing of other work pieces with similar size and shape. Compared to the pilot production's cleaning process and its numerous manual operations, the new system cuts the processing time in half. “A big advantage is that after an unplanned delivery stop by the customer, we can resume production much more quickly and can supply the OEM with cleaned work pieces in extremely short lead times,” Lechner said. The interlinked equipment concept also yielded considerable cost savings by reducing the required manpower for operating the system. It also greatly improved the working environment for employees since they no longer need to move the part bins between different machines, saving them time and effort. Decades of experience and the ability to design, service, and maintain machines as well as provide the consumables and accessories needed to get the finish you require make Rosler a well-rounded, single source for surface finishing expertise. Contact us to discuss your mass finishing needs.

Herzensangelegenheit Mitarbeiter-Ehrung – Rösler feiert endlich wieder im großen Rahmen

Im Jahr 1982 wurde Helmut Kohl Bundeskanzler der Bundesrepublik Deutschland, in Erlangen wurde das erste Retortenbaby des Landes geboren, und das US-Nachrichtenmagazin „Time“ wĂ€hlte den Computer zur „Maschine des Jahres“. Alles entscheidende Ereignisse, die den Lauf der Welt maßgeblich beeinflusst haben. FĂŒr Maria Zillig und Thomas Eberth war das Jahr 1982 aber noch aus einem anderen Grund besonders einschneidend: Es war das Jahr, in dem sie ihre Ausbildung zur Industriekauffrau und zum Industriekaufmann begonnen haben. Und zwar bei der Rösler OberflĂ€chentechnik GmbH in Memmelsdorf / Untermerzbach beziehungsweise Hausen. Dort arbeiten sie auch heute noch. Ganze 40 Jahre spĂ€ter. Genauso wie ihr Kollege Detlef Griebel, der ebenfalls seit 1982 bei „seinem“ Rösler beschĂ€ftigt ist. Einem Unternehmen so lange die Treue zu halten ist alles andere als selbstverstĂ€ndlich. Deshalb hat die Rösler OberflĂ€chentechnik GmbH diese, und 39 weitere langjĂ€hrige Mitarbeiter, jetzt im feierlichen Rahmen fĂŒr ihre lange Unternehmenszugehörigkeit geehrt. FĂŒr den GeschĂ€ftsfĂŒhrenden Gesellschafter Stephan Rösler ist die jĂ€hrliche Ehrungsfeier eine echte Herzensangelegenheit. In diesem Jahr ist sie es gleich aus mehreren GrĂŒnden: Nachdem die Ehrungen in den letzten Jahren aufgrund der Corona-BeschrĂ€nkungen nur im kleinen Kreise stattfinden konnten, darf in diesem Jahr zum ersten Mal wieder im großen Rahmen gefeiert werden: Im neuen Rösler Betriebsrestaurant, welches 2021 am Standort Memmelsdorf / Untermerzbach eröffnet wurde. Bei der feierlichen Ehrung der verdienten Mitarbeiter bekam Stephan Rösler in diesem Jahr UnterstĂŒtzung von seinen beiden GeschĂ€ftsfĂŒhrerkollegen Volker Löhnert und Oliver GrĂŒn. Letzterer wurde selbst fĂŒr seine zehnjĂ€hrige Betriebszugehörigkeit ausgezeichnet. Die Rösler OberflĂ€chentechnik GmbH gratuliert 
 zum 40-jĂ€hrigen BetriebsjubilĂ€um: im Werk Memmelsdorf: Maria Zillig und Thomas Eberth. Beide sind dem Unternehmen nicht nur im selben Jahr, sondern als Lehrlinge auch am gleichen Tag beigetreten. Im Werk Hausen wird Detlef Griebel fĂŒr vier Jahrzehnte Treue geehrt. 
 zum 25-jĂ€hrigen BetriebsjubilĂ€um: Eduard Fischer, Andreas Hentschel, Mario Jakob, Ralf MĂŒller, Waldemar Riwe, Folkert Rothe, Steffen Schwab, Jens Siebensohn, Gerald Weiß, Katja Wohnig, Uwe Zörkler – alle tĂ€tig im Werk Memmelsdorf – sowie Ernst Hoffer, Peter Leipert, Rainer Schindhelm und Alexander Schröder im Werk Hausen. 
 zum 10-jĂ€hrigen BetriebsjubilĂ€um: im Werk Memmelsdorf: Norbert Wolf Dicker, German Gerstenlauer, Tim Gleichmann, Susanne Henkel, Christian Höhn, Martin Hopf, Kevin Kern, Kathrin Knöferl, Wolfgang Kroner, Marcus Mannel, Andreas Merz, Marco Schmittwolf, Arno Schneider, Holger SchwĂ€mmlein, Dominik Sperlich, RenĂ© StĂŒllein, Sven Trier, Udo Weierich, Jennifer Weinland und Katja Weis sowie Katrin Fuchs, Oliver GrĂŒn, Ingrid Vetter und Yvonne Wagner im Werk Hausen. Nach langjĂ€hrigem verdienstvollen Einsatz wurden Reiner Allert, Gerhard Edelmann, Uwe Fleischmann, Herwig Heiser, Imelda Hellmuth, Carola Jankowski, Wolfgang Panzer, Fredi Spangel, Martin Trutz, Theo Wirsching sowie Oswald Zöttlein in den Ruhestand verabschiedet. Kurs halten im Krisenjahr: Rösler hĂ€lt an langfristigen Zielen fest Es war ein schwieriges Jahr mit vielen UnwĂ€gbarkeiten – dieses Fazit zog der GeschĂ€ftsfĂŒhrende Gesellschafter der Rösler OberflĂ€chentechnik GmbH, Stephan Rösler, in seinem traditionellen Weihnachtsgruß an die Belegschaft. Man sei in den ersten drei Monaten gut gestartet, der Ukraine-Krieg habe dann aber vieles verĂ€ndert – und die aufgrund der Corona-Krise ohnehin schon schwierige Lage an den BeschaffungsmĂ€rkten zusĂ€tzlich verschĂ€rft. Weitere Schwierigkeiten wie die Kostenentwicklung blieben aktuell, obendrauf kam noch die Energiethematik. Das im MĂ€rz 2022 abgelaufene GeschĂ€ftsjahr konnte die Rösler OberflĂ€chentechnik GmbH zwar erfreulich mit einem unkonsolidierten Gruppenumsatz von rund 273,9 Mio. € und somit einem Gruppenplus von rund 16 Prozent abschließen und so die durch die Pandemie verursachte Umsatzdelle aus dem vorangegangenen GeschĂ€ftsjahr hinter sich lassen. Die Prognosen fĂŒr das laufende GeschĂ€ftsjahr geben aber ein uneinheitliches Bild ab: So werden die Verfahrensmittel, Ersatzteil- und Serviceleistungen zwar weiterhin auf stabilem Niveau nachgefragt. Das NeumaschinengeschĂ€ft gestaltet sich allerdings schwieriger: Der russische Markt ist durch die Embargobestimmungen weggebrochen, außerdem ist durch die weltwirtschaftlichen Rahmenbedingungen insbesondere bei Großprojekten eine ZurĂŒckhaltung bei Investitionen festzustellen. Aus diesem Grund wird der Auftragseingang im Neumaschinenbereich zunĂ€chst unterhalb der Planungen liegen. Auch aufgrund einer Vielzahl getroffener Maßnahmen habe die Rösler OberflĂ€chentechnik GmbH die zahlreichen Herausforderungen bisher aber „ganz gut bewĂ€ltigt“, so Stephan Rösler weiter. An seiner langfristigen Ausrichtung gemĂ€ĂŸ der Firmenphilosophie Mission & Vision wolle das Unternehmen festhalten, zudem habe man 2022 trotz aller Schwierigkeiten einige wegweisende Projekte auf den Weg gebracht. Beispielsweise die Rösler Innowelt, ein umfassendes Konzept zur Umstrukturierung und Modernisierung fast des kompletten BĂŒrobestandes am Standort Memmelsdorf / Untermerzbach. Langfristig erhoffe er sich auch durch zahlreiche Produktneu- und Weiterentwicklungen, die die Rösler Firmengruppe in den letzten Monaten auf den Weg gebracht habe, weitere StĂ€rke, so Stephan Rösler. Im abgelaufenen GeschĂ€ftsjahr wurden ca. 5,6 Mio. € am Standort Memmelsdorf investiert und auch im laufenden Jahr werden weitere Investitionen in zukunftsorientierte Projekte an den deutschen Produktionsstandorten erfolgen. Seinen Mitarbeitern dankte der GeschĂ€ftsfĂŒhrende Gesellschafter fĂŒr die tatkrĂ€ftige UnterstĂŒtzung und LoyalitĂ€t im vergangenen Jahr. Trotz aller Schwierigkeiten konnte allen BeschĂ€ftigten das Weihnachtsgeld in voller Höhe ausgezahlt werden. Ein starkes Zeichen zum Ende eines Jahres, das aus vielerlei GrĂŒnden getrost als sehr schwierig bezeichnet werden darf.
Drahtgurt-Durchlaufstrahlanlage

Im Fertigungstakt der Spritzgussmaschine effizient zu grat- und staubfreien Duroplast- und Thermoplast-Komponenten

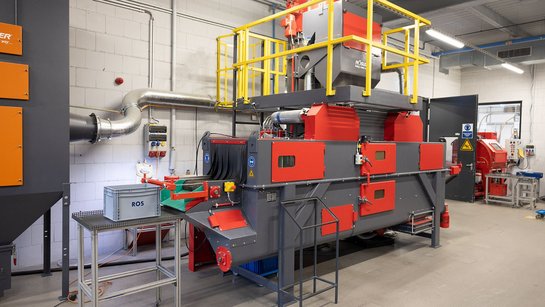
Die Verarbeitung von Kunststoffen hat bei der 1926 als Presswerk Ros gegrĂŒndeten Ros GmbH & Co. KG eine fast 100-jĂ€hrige Tradition. Inzwischen ist das Familienunternehmen in dritter Generation ein High-End-Partner fĂŒr technisch anspruchsvolle Spritzgussteile aus Duroplasten, Thermoplasten inklusive Polyphenylensulfid (PPS). Entwicklung, Werkzeugbau und Fertigung befinden sich am Unternehmenssitz in Coburg, produziert wird darĂŒber hinaus im thĂŒringischen Ummerstadt. FĂŒr die Entfernung der verfahrensbedingt entstehenden Grate arbeitet das Unternehmen seit 2006 mit Strahlanlagen von Rösler. Ausbau der StrahlkapazitĂ€t „Dass wir 2021 an beiden Standorten unsere StrahlkapazitĂ€t erweitern mussten, lag einerseits an einem erhöhten Aufkommen von Kunststoffkomponenten, die Metallteile substituieren, beispielsweise von Thermomanagementsystemen fĂŒr die Automobilindustrie. Sie ermöglichen, Gewicht einzusparen und dadurch CO2-Emissionen zu verringern. Andererseits haben wir großvolumige neue AuftrĂ€ge fĂŒr die Herstellung duroplastischer Formteile, unter anderem von einem großen GartengerĂ€tehersteller, erhalten“, berichtet JĂŒrgen BĂ€r, zustĂ€ndig fĂŒr die technische Planung im Bereich Industrial Engineering bei Ros in Coburg. Nach GesprĂ€chen mit vier Herstellern von Strahlanlagen entschied man sich fĂŒr die Drahtgurt-Durchlaufstrahlanlage RSAB 470 und das Wendebalken-Strahlsystem RWS 1200 von Rösler. „Ausschlaggebend waren die guten Erfahrungen mit den vorhandenen Anlagen, die kompakte Bauweise und solide Konstruktion sowie die umfangreiche Erfahrung des Unternehmens im Bereich Strahlen von Kunststoffteilen“, merkt JĂŒrgen BĂ€r an. „Außerdem benötigten wir die Durchlaufstrahlanlage sehr schnell und Rösler bot uns an, die Maschine aus deren Customer Experience Center kurzfristig zu liefern.“ Prozesssicheres und energieeffizientes Entgraten im Tempergestell Die flexible Hochleistungsanlage RSAB 470 wird am Standort Coburg fĂŒr das kontinuierliche Entgraten von Spritzgussteilen aus Duroplasten und dem Hochleistungsthermoplast PPS-GF eingesetzt. Nach der Bearbeitung erfolgt eine Temperbehandlung, fĂŒr die die Teile auf spezielle Gestelle gesteckt werden. Um den manuellen Aufwand fĂŒr das Teilehandling zu minimieren und das lose Auflegen der Teile auf den Drahtösengurt der Strahlanlage zu eliminieren, passte Rösler das Standard-WerkstĂŒcktransportsystem an den Workflow bei Ros an. Dies ermöglicht, die Tempergestelle direkt nach dem Spritzgießen mit den Teilen zu bestĂŒcken, auf den Vorrichtungen zu entgraten und dem Tempern zuzufĂŒhren. FĂŒr ein prozesssicheres und reproduzierbares Strahlergebnis verfĂŒgt die Anlage ĂŒber vier fĂŒr die Kunststoffbearbeitung entwickelte Turbinen, die ĂŒber und unter dem Gurt platziert sind. Sie applizieren das Strahlmittel – ein Polyamid-Korn mit 1 mm KantenlĂ€nge – stark beschleunigt von oben und unten auf die Teile. Im Gegensatz zur ĂŒblicherweise mit Druckluft betriebenen Injektorstrahltechnik arbeitet die Turbinenstrahltechnik mit den verwendeten Elektroantrieben erheblich energieeffizienter. „Möglichkeiten, Energieeinsparungen umzusetzen, fordert nicht nur unsere Zertifizierung nach DIN EN 50001, eine Verringerung des Energieverbrauchs ist auch unter Nachhaltigkeits- und Kostenaspekten heute dringend nötig“, ergĂ€nzt JĂŒrgen BĂ€r. Eine StrahlmittelĂŒberwachung mit automatischer Nachdosierung gewĂ€hrleistet, dass das Strahlmittel immer in optimaler QualitĂ€t eingesetzt wird. Das Antistatiksystem mit automatischer Nachdosierung, die Strahlkammerabsaugung, eine zweistufige Abreinigung der Teile in der Auslaufzone der Anlage sowie die effektive Strahlmittelaufbereitung mit Siebvorrichtung und Kaskadenwindsichtung tragen ebenfalls dazu bei, dass die Teile bedarfsgerecht entgratet und sauber aus der Anlage kommen. Da durch die bei Ros eingesetzten Werkstoffe und das Polyamid-Strahlmittel explosionskritische StĂ€ube entstehen können, wurden die Anlagen mit speziellen, ATEX-konformen Filtersystemen ausgestattet. Einzelteile nachhaltig vollautomatisch entgraten Die Wendebalken-Strahlanlage RWS 1200 , mit der die StrahlkapazitĂ€t im Werk Ummerstadt erweitert wurde, kommt fĂŒr Bauteile aus PPS-GF mit einem HĂŒllkreis von bis zu 163 mm zum Einsatz. Passend zum Fertigungstakt der Spritzgussmaschine werden jeweils vier WerkstĂŒcke gleichzeitig in der vorgegebenen Zeit von 40 Sekunden entgratet. Die Anlage verfĂŒgt dafĂŒr ĂŒber zwei Bereiche, die jeweils mit vier Satelliten ausgestattet sind. Diese Konstruktion ermöglicht, dass parallel zum Entgratprozess die Be- und Entladung erfolgen kann. Unproduktive Nebenzeiten werden minimiert. FĂŒr einen energieeffizienten Betrieb appliziert eine Turbine Strahlmittel von oben auf die Teile auf den rautenförmig angeordneten Satelliten, die nicht nur rotieren, sondern auch in einer teilespezifisch festlegbaren Winkelstellung stoppen können. In Bereichen, die durch das Strahlmittel der Turbine geometriebedingt nicht erreicht werden, sorgen InjektorstrahldĂŒsen mit DruckĂŒberwachung an einer vertikal verfahrbaren Einheit fĂŒr eine prĂ€zise Entgratung. DafĂŒr lassen sich die DĂŒsen zusĂ€tzlich zur Hubbewegung ĂŒber ein Wegmesssystem exakt vor den Teilen platzieren, wobei sowohl oszillierend als auch punktuell gestrahlt werden kann. „Um hier den Druckluftverbrauch zu minimieren, arbeiten wir mit teilespezifischen Bearbeitungsprogrammen“, berichtet JĂŒrgen BĂ€r. Ausgestattet ist die RWS 1200 darĂŒber hinaus mit einer automatischen Nachdosierung fĂŒr das Strahlmittel und das Antistatikmedium, einer Strahlkammerabsaugung und Strahlmittelaufbereitung. Das Familienunternehmen ROS Bereits seit 1926 steht das Familienunternehmen ROS GmbH & Co. KG fĂŒr PrĂ€zision in Kunststoff. Als Spezialist fĂŒr hochprĂ€zise technische Kunststoffspritzgussteile vertrauen fĂŒhrende Unternehmen aus den Bereichen Automotive, Medizintechnik, Elektrotechnik und weiteren Industrien seit mehr als 90 Jahren auf die QualitĂ€t der ROS-Produkte. Mit rund 300 Mitarbeitern an zwei Standorten in der Region Nordbayern/SĂŒdthĂŒringen kreiert und fertigt das Unternehmen mit eigenem Werkzeugbau hochprĂ€zise Werkzeuge fĂŒr die Verarbeitung von Hochleistungskunststoffen, woraus Funktionsteile entstehen.

Mass Finishing Work Piece Handling Series, Part 3 – Maintaining Wear Linings

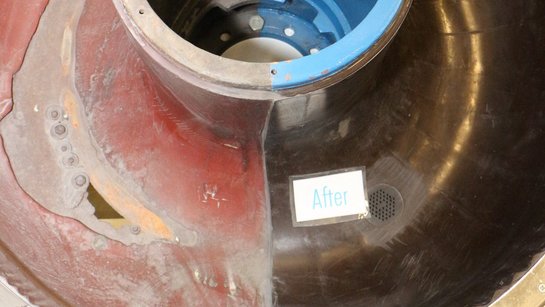
Adequate wear linings are an important factor in ensuring work pieces are efficiently handled in a mass finishing machine. Along with the method speed of transfer as well as the media selection and separation, the condition of a machine’s wear lining factors into the quality of process results. Thick linings assist with work piece handling by providing a cushioning effect, yet thin or damaged wear linings allow unwanted knicks, scratches, and dings. With more than 80 years of expertise in surface finishing, Rosler can assist with all aspects of your mass finishing process including proactively eliminating potential work piece handling issues. Observing Machine Conditions Regularly checking the lining of your work bowl(s) and trough(s) for wear is one way to ensure parts don’t get accidentally damaged during processing. Inspecting linings consistently will help identify repairable issues before permanent damage to the machine occurs. To effectively finish work pieces, media must be matched to the specific finishing task and the initial state of a work piece. For example, media used for deburring/edge radiusing and surface grinding can be very abrasive. If not properly protected by a suitable wear lining, the steel construction of a work bowl would be completely worn through in a few hours by contact with the media and work pieces. Polyurethane and, to a certain degree, rubber are excellent lining materials providing wear protection for thousands of operating hours. Even these materials wear through and must be periodically replaced with a new lining. Small areas can be temporarily patched with Polyurethane Repair Kits until the unit can be removed and professionally relined. If a reline is required, only use a qualified reline supplier such as the lining shop at Rosler. Relines are available in different degrees of hardness (shore A) and different qualities. Always make sure that the lining material is suitable for your specific mass finishing process. More information about specifying liner materials is available in a previous blog post . Side-by-side comparison of a vibratory bowl before and after relining Maintaining Process Stability Checking your work bowl lining for wear and replacing it in a timely manner is essential for the stability of your mass finishing process as a whole. In addition to worn work bowls, failure to ensure a proper protective lining can create other problems including: Work pieces getting stuck in the machine and, therefore, jeopardizing the integrity of different work piece batches. Media, water, and process chemicals can leak from the machine if the metal processing bowl is worn through and holes or cracks appear. Severe machine malfunction can occur when media or parts can get trapped in worn spots during the separation phase when the finished work pieces are separated from the media. Damage to the work bowl that is beyond repair, causing unnecessary downtime and requiring costly replacement parts. A weakened bowl can crack and make the entire machine unusable. Check your bowl lining at least monthly for wear or rips. The areas around drains, the parts loading chute, and around the unload areas will see the highest wear and are especially crucial. The “nail test” makes checking the liner thickness easy. Push a nail through the liner until you hit the base metal and record the thickness of the liner. Keep track of the liner thickness over time to predict when you will need to replace your liner. Most liners are between 5/8 and 1 in (15-25 mm) thick. Plan to get your machine relined when the thinnest part of your liner is less than 1/4 in (6 mm) thick. Just as optimal media mix must be regularly monitored, so must the condition of a work bowl. If not, the entire process and downstream operations may suffer. The Rosler Way Maintaining adequate wear linings protects your work pieces, equipment, and overall mass finishing process. Contact us for mass finishing expertise and insight. The complete Mass Finishing Work Piece Series includes: Part 1 – Selecting the Best Work Piece/Media Separation Method . Part 2 – Preventing Drop Height Damage . Part 3 – Maintaining Wear Linings .
emi-automatic centrifuge Z 800

Rösler Smart Solutions: Digitales Prozesswassermanagement – Optimierte Gleitschliffergebnisse durch besseres ProzessverstĂ€ndnis

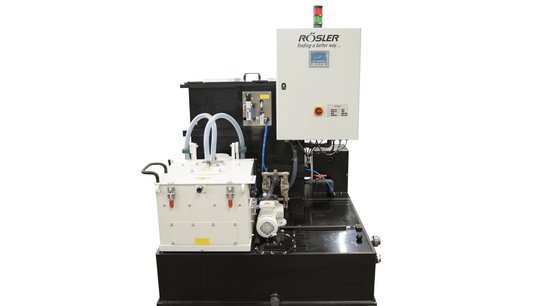
Mit Federn der 1889 von Siegmund Scherdel gegrĂŒndeten Drahtzieherei experimentierte schon Rudolf Diesel am ersten Dieselmotor der Welt. Inzwischen deckt die Scherdel-Gruppe von der Umformtechnik ĂŒber die Montage- und FĂŒgetechnik bis hin zur OberflĂ€chentechnik sowie den Maschinen , Werkzeug- und Anlagenbau ein breites Spektrum ab. Das heute mit 32 Standorten weltweit tĂ€tige Unternehmen steht seinen Kunden vom Briefing bis zur Serienfertigung als Partner zur Seite. Ergebnis sind Premiumprodukte, die nicht nur in der Automobilindustrie, sondern beispielsweise auch in der Medizintechnik, der Elektro- und Energietechnik im Einsatz sind. Dazu zĂ€hlen auch die Stanz- und Biegeteile, Federringe und Komponenten fĂŒr die ElektromobilitĂ€t, die bei der Scherdel Waldershof GmbH & Co. KG im bayerischen Waldershof gefertigt werden. Die Komponenten aus verschiedenen Stahllegierungen, Edelstahlen und Buntmetallen erhalten zum Teil in Gleitschliffprozessen den perfekten Schliff. Neben der eigentlichen Bearbeitungsaufgabe wie dem Entgraten und Kantenverrunden sind dabei eine anforderungsgerechte technische Sauberkeit sowie saubere OberflĂ€chen wichtige QualitĂ€tsmerkmale, sodass eine optische QualitĂ€tskontrolle einwandfrei durchgefĂŒhrt werden kann. Eine entscheidende Rolle dafĂŒr spielt die QualitĂ€t des Prozesswassers. Aufbereitung und Überwachung des Prozesswassers – fĂŒr viele Anwender und Betreiber Das Prozesswasser aus dem Gleitschliffprozess wird bei Scherdel Waldershof im Kreislauf gefĂŒhrt und durch eine halbautomatische Zentrifuge aufbereitet. Eine Überwachung der ProzesswasserqualitĂ€t erfolgte jedoch nur sehr eingeschrĂ€nkt in Form einer tĂ€glichen Kontrolle der Compound-Konzentration und mit wechselndem Personal, das ĂŒber kein tiefes Know-how zur Aufbereitung und Überwachung des Prozesswassers verfĂŒgte. „Durch den Eintrag von Ölen aus den Stanz-Biegeprozessen und Bandschmiermitteln sowie dem Material- und Schleifkörperabrieb verĂ€ndert sich die ProzesswasserqualitĂ€t. Einerseits nimmt die LeitfĂ€higkeit zu, was bei den optischen PrĂŒfungen zu fehlerhaften Ergebnissen fĂŒhrte. Andererseits wurden die Vorgaben hinsichtlich PartikelgrĂ¶ĂŸen und -mengen nicht immer eingehalten, woraus aufwendige Nacharbeiten oder sogar Ausschuss resultierte“, berichtet Tobias König, Abteilungsleiter OberflĂ€che Gleitschleifen / Reinigen bei Scherdel Waldershof. Digitales Prozesswassermanagement bringt Transparenz und Know-how Entsprechend groß war das Interesse des Abteilungsleiters, als ihm der Einsatz der digitalen Prozesswassermanagement-Lösung „Advanced“ von Rösler Smart Solutions als Pilotanwender vorgeschlagen wurde. Dieses neue Produkt fĂŒr die Prozesswasseraufbereitung fĂŒr halb- und vollautomatische Zentrifugen ermöglicht die anwenderorientierte Überwachung, Erfassung und Auswertung wesentlicher Prozessparameter. Dies sind: Compound-Konzentration (Titration oder Brechungsindex – BRIX), pH-Wert, LeitfĂ€higkeit, WasserhĂ€rte, mikrobiologische Belastung durch Bakterien, Hefen und Pilzen, Chloridgehalt, CSB-Wert (chemischer Sauerstoffbedarf), BIT-Gehalt (Biozide im Prozesswasser), Aussehen und Geruch. Angepasst an die jeweilige Anforderung an den Gleitschliffprozess, können die zu ĂŒberwachenden Parameter individuell ausgewĂ€hlt werden. In der ersten Ausbaustufe des Paketes „Advanced“ erfolgen die Probennahme und Analyse manuell mittels entsprechendem Messequipment, das auf Wunsch mitgeliefert werden kann. Eingegeben werden die ermittelten Werte ebenfalls manuell. Auf Basis der eingegebenen Daten berechnet der in der Software hinterlegte Algorithmus direkt umsetzbare Handlungsempfehlungen, um bei Abweichungen vom zuvor definierten Soll- oder Toleranzwert eines oder mehrerer Parameter diese wieder in den vorgegebenen Bereich zu bringen und damit die ProzessstabilitĂ€t zu sichern. Die Handlungsempfehlungen enthalten darĂŒber hinaus ErklĂ€rungen, welche Folgen Abweichungen des jeweiligen Parameters auf die BearbeitungsqualitĂ€t haben. Da alle Parameter gespeichert werden, kann auf die Daten in Form von Tabellen und Verlaufsdiagrammen zugegriffen werden. Letzteres ermöglicht ungeplante Betriebsunterbrechungen durch einen erforderlichen Wechsel des Prozesswassers zu vermeiden und einen Neuansatz auf einen in den Betriebsablauf optimal integrierbaren Zeitpunkt zu legen. „Rösler hat uns das digitale Prozesswassermanagement vorgestellt und wir haben sofort das Potenzial erkannt, durch diese Lösung mehr Transparenz und Prozesssicherheit zu erzielen. Außerdem haben wir die Möglichkeit gesehen, das ProzessverstĂ€ndnis unserer Mitarbeitenden durch die Handlungsempfehlungen mit entsprechenden ErklĂ€rungen deutlich zu verbessern“, erklĂ€rt Tobias König. ProzessstabilitĂ€t und BearbeitungsqualitĂ€t optimiert Scherdel Waldershof nutzt das digitale Prozesswassermanagement fĂŒr eine halbautomatische Zentrifuge Z 800 von Rösler, die eine im dreischichtigem Betrieb laufende Gleitschliffanlage (Rösler R 620), mit Prozesswasser versorg. Überwacht werden die Compound-Konzentration und der pH-Wert jeweils einmal pro Schicht. Eine LeitfĂ€higkeitsmessung erfolgt einmal wöchentlich. Die Kontrolle der mikrobiologischen Belastung des Prozesswassers wird nach Bedarf durchgefĂŒhrt. Dies ist beispielsweise der Fall, wenn Aussehen und Geruch, die ebenfalls regelmĂ€ĂŸig erfasst werden, Anzeichen auf eine VerĂ€nderung liefern. „Die Messungen und die Erfassung der ermittelten Werte ist einfach und schnell durchzufĂŒhren. Der Zeitaufwand fĂŒr die Messung und Erfassung der Compound-Konzentration und des pH-Werts ist nahezu identisch mit dem der Kontrollen vorher“, beschreibt der Abteilungsleiter. „Allerdings erhalten wir heute eine ĂŒbersichtliche Auswertung und im Falle von Abweichungen leicht verstĂ€ndliche und direkt umsetzbare Handlungsempfehlungen, die automatisch ausgegeben werden. Das trĂ€gt definitiv dazu bei, sowohl die Prozesswasser- als auch die TeilequalitĂ€t stabil zu halten und dadurch Nacharbeiten und Ausschuss um bis zu 50 % zu reduzieren.“ Handlungsempfehlungen stehen aber nicht nur bei Sollwert-Abweichungen zur VerfĂŒgung, sondern auch fĂŒr bestimmte qualitĂ€tsmindernde Vorkommnisse wie Korrosion auf den Teilen, einer Schaumbildung im Gleitschliffprozess und bei unzureichender Bauteilsauberkeit, die beispielsweise Folgeprozesse beeintrĂ€chtigt. Um diese Probleme zu beseitigen, enthalten die Handlungsempfehlungen verschiedene Maßnahmen sowie ErklĂ€rungen ĂŒber die ZusammenhĂ€nge im Prozess. „Die Kolleginnen und Kollegen in der Abteilung haben ĂŒblicherweise keine spezielle Ausbildung zum Thema Gleitschleifen und Prozesswasser. Durch die Handlungsempfehlungen wissen sie nicht nur, was im Fall des Falles zu tun ist. Sie erhalten auch entsprechendes Hintergrundwissen, sodass das Bewusstsein fĂŒr die ZusammenhĂ€nge zwischen ProzesswasserqualitĂ€t und TeilequalitĂ€t gestĂ€rkt wird“, merkt Tobias König abschließend an.

Testing & Expertise Overcome Shot Blasting Challenges

For nearly a decade, Sales Representative and Interim Product Manager of Turbine Blast Equipment Zack Murray has been one of Rosler’s top shot blasting experts. Working with customers and our global Customer Experience Centers , he helps develop and test surface finishing machines and media in addition to dialing in specific process parameters. At times, adhering to the Rosler motto and guiding principle of “finding a better way
” can be difficult and complicated. Luckily, Murray and the entire Rosler team are committed to delivering world-class surface finishing equipment, consumables, and service in a variety of industries . In this post, Murray shares the most challenging issue he has tackled at Rosler and how the team developed a solution. The Problem A customer contacted Rosler for help in processing relatively large magnesium automotive parts. Considering the need for high throughput speeds in combination with the size of the parts, Murray knew a turbine blast machine would be the best option. Shot blasting turbine “In turn, the indication of a turbine blast machine meant that we were limited to metallic blast media,” Murray said, “as these machines are not typically suitable for mineral-based blast media such as aluminum oxide or glass beads. “Magnesium is a tricky material to blast in a turbine machine since it is prone to sparking with most metallic media. In addition to the fact that magnesium dust is highly flammable and combustible, we needed to avoid a potential recipe for disaster.” The process had to safely and efficiently deliver deburring and edge radiusing while minimizing the potential for sparking. The Solution Understanding that a relatively soft metallic media was required for safety and effectiveness, the team was left with the choice of aluminum or zinc blast media. Testing both media types demonstrated that results from the aluminum media most closely aligned with the customer’s desired process results. “Unfortunately, aluminum dust is also highly flammable and combustible,” Murray said. “The combination of the magnesium and aluminum dust was potentially dangerous enough to warrant an St3 Dust Hazard rating, which is the most severe rating, indicating a very high potential for fire and/or explosion. “Since the customer was not at a point in their product development cycle where they could get a dust hazard analysis performed as a result of part availability, we had to assume that the dust would be rated at St3.” As such, a wet dust collector with an anti-oxidizing compound dosing system was suggested for the customer with the further recommendation that the dust collector be installed outside, away from areas that commonly see human traffic, and that exhaust air was absolutely not allowed to feed back into the building. Rosler RF 550 NS including sludge drag conveyor and high-efficiency design to reduce residual dust The Rosler Way With more than 80 years of experience and a portfolio containing more than 15,000 equipment and consumable products, solving challenges is what we do at Rosler. Testing for safety and efficiency is an important step in achieving a stable and repeatable surface finishing process. Contact us today to request free test trials in one of our global Customer Experience Centers and allow us to develop a solution for your unique challenges!

Blade Technology: Straight vs. Curved Blades Explained

As an expert in the shot blasting industry, Rosler knows about blade technology. All shot blasting machines require blades to propel media towards workpieces. While both straight and curved blades are used, each type offers advantages and disadvantages. What are the Differences? Straight blades are, as the name suggests, blades that do not have curvature when viewed from the side and do not possess tangential curvature with respect to the turbine. Curved blades are blades that have some degree of curvature when viewed from the side. As the newer design, curved blades are generally better than straight blades, but they also have some drawbacks related to longevity, maintenance, and cost of ownership. Wear Rates Historically, the largest disadvantage of the curved blade design is that the blade will wear at a disproportionate rate along the length of the curvature, meaning that the curved blade design would wear through quicker than straight blade design. Modern technology has allowed the industry to overcome this particular flaw through the careful selection of curvature angle of the blade based on blade material properties to the point that curved blades now have similar usable lives to straight blades. Change Out Times A further disadvantage that has historically plagued the curved blade design is that the shape of the blades and fixturing take longer to change out than straight blades. The Rosler Gamma G turbine with forged metal blades overcomes this issue through the use of a retaining pin allowing for rapid blade change outs . This problem still currently persists for hard metal blade designs. Cost The final disadvantage is that curved blades tend to be more expensive than the straight blade designs, depending on the blade material. For cast and forged blades, the price difference is relatively small; however, for hard metal machined blades, the cost difference can be quite significant. Advantages Despite the disadvantages, curved blades also offer advantages over traditional straight blades. The largest advantage that the curved blades offer over straight blades of equivalent size is that the curved blades have a greater radial component to their velocities while maintaining an equivalent tangential component. This provides a higher throwing speed of the blades on the media (at equivalent turbine rotational velocities and equivalent turbine diameter) and therefore greater impact energy being transferred to the workpiece, allowing for the removal of more severe contaminants. Alternatively, if greater impact energy is not needed, the turbine’s rotational velocity can be controlled via a variable frequency drive to slow the turbine down which, in turn, provides a greater media throughput at equivalent media throwing speeds when compared against a straight blade turbine. Curved blade designs function at their best when the parts have very difficult finishing requirements or when greater part throughput is necessary. Orientations Curved blades have two types of orientation that can be used: a γ (The Greek letter gamma) shape and a C shape. The C shape has a greater curvature angle, allowing for a greater velocity/energy efficiency; however, the γ shape blade has a blade longevity factor in that once one side has been worn down, the blade can be flipped for a second use, effectively doubling the blade’s life. This is also an advantage over most straight blade designs. C-shaped blade Furthermore, the C shape does not have the ability to utilize a retaining pin for rapid blade changeout . The curvature angle of the blade (and therefore the blade's velocity and energy gain in comparison to a straight blade design) provides an equivalent lifetime based off of the material properties of the blade, namely its metal hardness. For modern metals, a cast blade can support a nearly negligible curvature without severely impacting its life, while a forged blade is capable of supporting a curvature angle that provides approximately a 7% increase in velocity (approximately 15% increase in energy) and a hard metal machined blade supports a curvature giving up to approximately 15% increase in velocity (approximately a 32% increase in energy) (utilizing a C shaped blade for maximum gain). The Rosler Way You can count on Rosler to help you find a better way when it comes to blade technology. Contact us today to discuss your unique challenges so we can identify the right blade for your needs.
Handshake

Sauber Technologies baut Partnerschaft mit AM Solutions, eine Marke der Rösler Gruppe, aus

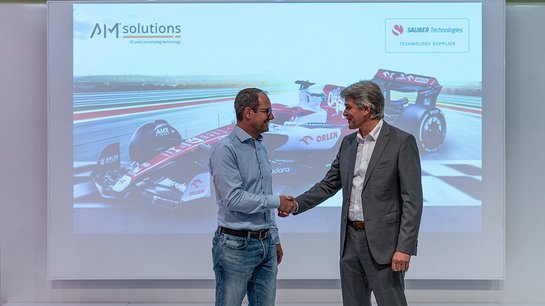
Sauber Technologies verlĂ€ngert seine Technologiepartnerschaft mit AM Solutions – 3D post processing technology, eine Marke der Rösler Gruppe, und geht damit einen weiteren Schritt in Sachen technologischer Innovationen. Die VerlĂ€ngerung der bereits 2021 geschlossenen Partnerschaft um weitere zwei Jahre ist eine logische Konsequenz der wertvollen und vertrauensvollen Zusammenarbeit, die beiden Parteien bereits hervorragende Ergebnisse beschert hat. Die automatisierte Nachbearbeitung von additiv gefertigten Teilen ist fĂŒr Sauber Technologies unverzichtbar, wenn es darum geht, reproduzierbare und hochwertige Bauteile wirtschaftlich herzustellen zu können, insbesondere im industriellen Maßstab. Im vergangenen Jahr profitierte das Unternehmen bereits von Röslers langjĂ€hriger Erfahrung in der OberflĂ€chenbearbeitung, indem Sauber Technologies auf Nachbearbeitungslösungen der Rösler-Marke AM Solutions – 3D post processing technology setzte. Mehrere 3D-gedruckte Teile wurden auch im Alfa Romeo F1 Team ORLEN C42 verbaut, wodurch die strategische Partnerschaft letztendlich auch den Weg von der Fabrik auf die Rennstrecke fand. Unter der Marke AM Solutions – 3D post processing technology bĂŒndelt die Rösler Gruppe alle TĂ€tigkeiten rund um die additive Fertigung und bietet ein herausragendes Produkt- und Leistungsspektrum an, darunter Anlagen, Verfahrensmittel und Verfahrenstechnik fĂŒr die serienreife automatisierte Nachbearbeitung von 3D-gedruckten Teilen. Röslers langjĂ€hrige, branchenĂŒbergreifende Erfahrung in der OberflĂ€chenveredelung im industriellen Produktionsumfeld sowie der eigene Maschinenbau bilden ein starkes RĂŒckgrat der AM Solutions Angebote. Sauber Technologies und AM Solutions kooperieren im Rahmen ihrer Partnerschaft derzeit im Bereich der Nachbearbeitung 3D-gedrucketer Teile, welche mittels SLA (Stereolithographie) Technologie hergestellt werden. Ziel ist die Entwicklung von Lösungen, die die Effizienz des Reinigungsvorgangs und der Entfernung der StĂŒtzstrukturen maximieren. DarĂŒber hinaus nutzt Sauber Technologies bereits mehrere Gleitschliff- und Strahllösungen von AM Solutions. Christoph Hansen, COO Sauber Technologies: „Im Laufe des letzten Jahres war die Partnerschaft mit AM Solutions sehr wichtig fĂŒr uns. Unsere Gruppe konnte in mehreren GeschĂ€ftsvorhaben davon profitieren. Dies reichte von Windkanalmodellen bis hin zu hoch experimentellen Bauteilen und natĂŒrlich unseren Formel-1-Rennwagen. AM Solutions bereichert Sauber Technologies mit seinem außerordentlichen Erfahrungsschatz und den exzellenten Lösungen. Wir können 3D-gedruckte Teile nun schneller und effizienter herstellen, was zwei wesentliche Merkmale fĂŒr ein sich stĂ€ndig wandelndes GeschĂ€ft wie das unsere ist. Ich freue mich sehr, dass wir unsere Partnerschaft mit der Rösler Gruppe ausweiten und ich bin gespannt, was wir in Zukunft noch alles erreichen können.“ Volker Löhnert, GeschĂ€ftsfĂŒhrer der Rösler OberflĂ€chentechnik GmbH: „Die VerlĂ€ngerung unserer Partnerschaft mit Sauber Technologies ist ein wichtiger Meilenstein fĂŒr AM Solutions – 3D post processing technology. Das Sauber-Team hat eine lange Tradition in der Verwendung von additiv gefertigten Bauteilen in seinen Formel-1-Rennwagen. Insbesondere in den Bereichen Design, Materialauswahl und Leichtbau bietet der 3D-Druck erhebliche Vorteile. FĂŒr die Optimierung der gesamten Prozesskette ist eine qualitativ hochwertige und reproduzierbare Nachbearbeitung von großer Bedeutung. Hier kommt unsere jahrzehntelange Erfahrung in der OberflĂ€chenbearbeitung ins Spiel – zusammen mit unseren maßgeschneiderten Lösungen, die speziell fĂŒr die Besonderheiten von 3D-gedruckten Teilen entwickelt wurden. Aus diesen GrĂŒnden haben wir mit Sauber Technologies den perfekten Partner an unserer Seite."
centrifugal disk finishing machine

Husqvarna setzt auf intelligent verkettete Anlagen von Rösler

Den KapazitĂ€tsengpass bei der OberflĂ€chenbearbeitung beseitigt Vor der Erweiterung und Modernisierung waren die Fliehkraftanlagen verschiedenen Gleitschliffprozessen fest zugeordnet. Diese Trennung der Bearbeitungsprozesse sollte eine Vermischung der ProzessflĂŒssigkeiten vermeiden und somit deren Reinigung erleichtern. Hierdurch konnten jedoch die Fliehkraftanlagen nicht flexibel verplant werden, weshalb die verfĂŒgbare KapazitĂ€t nicht wirtschaftlich genutzt werden konnte und EngpĂ€sse unvermeidbar waren. Um die Fertigung deutlich flexibler zu gestalten, ist die neue Fliehkraftanlage mit doppelter Dosiertechnik ausgestattet, sodass unterschiedliche Prozesse darin durchfĂŒhrt werden können. Zusammen mit der Integration der neuen Zentrifuge und der daraus resultierenden VergrĂ¶ĂŸerung und redundant ausgelegten AufbereitungskapazitĂ€t der ProzessflĂŒssigkeiten können die Bearbeitungsanlagen ohne mögliche QualitĂ€tseinbußen bei der TeilequalitĂ€t nun bedarfsgerecht geplant werden. Innovative Details fĂŒr höhere Prozesssicherheit bei kĂŒrzeren Bearbeitungszeiten FĂŒr eine optimierte und prozesssichere Bearbeitung sorgt bei der neuen Fliehkraftanlage mit kundenspezifisch konstruierter Beschickungslösung einerseits der speziell konzipierte ArbeitsbehĂ€lter mit erhöhtem Volumen, andererseits wird durch speziell entwickelte Strömungsleitsegmente und einfach auswechselbare „Anti-Schlupf“ Stege, in Kombination mit einem speziell ausgeformten Drehteller und einer erhöhten Antriebsleistung, eine bessere Durchmischung der meist mehrere Hundert Kilogramm schweren Teilecharge erzielt. Die daraus resultierende intensivere Bearbeitung ermöglicht kĂŒrzere Prozesszeiten und erhöht die ProduktivitĂ€t der Anlage deutlich. Ein weiteres Ausstattungsmerkmal, das Husqvarna sofort begeisterte, ist die vollautomatische Verstellung des Ringspalts zwischen Drehteller und BehĂ€ltermantel. Manuelle Einstellung und zeitraubende PrĂŒfung des Spaltmaßes durch den Maschinenbediener werden damit vermieden und die intelligente Steuerung ermöglicht zusĂ€tzlich, dass die Fliehkraftanlage selbststĂ€ndig auf ein bauteilgerechtes Spaltmaß einstellt. Außerdem wird der Spalt auch wĂ€hrend des Bearbeitungsprozesses ĂŒberwacht und bei Bedarf automatisch nachjustiert, was ein Alleinstellungsmerkmal von Rösler ist. Diese Technologie verhindert, dass insbesondere dĂŒnne und filigrane Teile wĂ€hrend der Bearbeitung in den Spalt gelangen und einen erhöhten Verschleiß oder gar Maschinenschaden verursachen. Neben der Prozesssicherheit erhöht die automatische Spalteinstellung die AnlagenverfĂŒgbarkeit, da keine Zeit mehr fĂŒr die Einstellung benötigt wird. VollstĂ€ndige Prozesskontrolle und Traceability Zum Auftragsumfang zĂ€hlte auch die Verkettung der Gleitschlifftechnik mit der Anlage eines Nachfolgeprozesses inklusive der Übermittlung von Programmen und Prozessdaten, sowie die Einbindung der Anlagen in das bestehende Manufacturing Executive System (MES) von Husqvarna. Dadurch ist eine vollstĂ€ndige und lĂŒckenlose Prozesskontrolle und RĂŒckverfolgbarkeit des Anlagenzustandes und der Bearbeitungsparameter gewĂ€hrleistet. Digitales Prozesswassermanagement - bis zu 50 % weniger Frischwasserverbrauch und lĂ€ngere Standzeit der ProzessflĂŒssigkeit Da die Prozesswasseraufbereitung bei Husqvarna sehr anspruchsvoll und herausfordernd ist, legt das Unternehmen großen Wert auf die Integration des digitalen Prozesswassermanagements von Rösler Smart Solutions in den modernisierten Wasserkreislauf. Diese innovative, interaktive Monitoring-Lösung fĂŒr die Prozesswasseraufbereitung mit halb- und vollautomatischen Zentrifugen ermöglicht die Überwachung, Erfassung und Auswertung wesentlicher Prozessparameter. Entsprechende Handlungsempfehlungen, die automatisch ausgegeben werden, ermöglichen den Frischwasserverbrauch deutlich zu verringern und die Standzeit der ProzessflĂŒssigkeit kostensparend zu erhöhen. Auf Basis zunĂ€chst manuell durchgefĂŒhrter Analysen konnte der erforderliche Wechselintervall fĂŒr die ProzessflĂŒssigkeit um bis zu 50 % verlĂ€ngert werden. Die erzielte StandzeitverlĂ€ngerung liegt ebenfalls bei bis zu 50 %. Projektrealisierung in Time Umgesetzt wurde die KapazitĂ€tserweiterung und Modernisierung mit einem anspruchsvollen und ambitionierten Zeitplan. Dabei konnte Rösler trotz der derzeitigen UnwĂ€gbarkeit hinsichtlich TeileverfĂŒgbarkeit den vereinbarten Liefertermin nicht nur einhalten, sondern das System sogar zwei Wochen frĂŒher bei Husqvarna in Betrieb nehmen. Rösler Smart Solutions – verbesserte TeilequalitĂ€t und minimierter Ausschuss Im Einsatz ist Rösler Smart Solutions auch bei der Scherdel Waldershof GmbH & Co. KG, die aus Stahllegierungen, EdelstĂ€hlen und Buntmetallen Stanz- und Biegeteile sowie Komponenten fĂŒr die Automobilindustrie fertigt. Bei der Gleitschliffbearbeitung sind neben dem Entgraten und Kantenverrunden eine anforderungsgerechte technische Sauberkeit sowie einwandfrei saubere OberflĂ€chen fĂŒr die nachfolgende optische QualitĂ€tskontrolle zu erreichen. Dabei kam es aufgrund der bisher einfachen QualitĂ€tsĂŒberwachung des Prozesswassers anhand weniger Parameter immer wieder zu RĂŒckstĂ€nden auf den bearbeiteten Teilen, die nur durch kostspielige Nacharbeiten entfernt werden konnten, bevor die Teile zum Kunden geliefert wurden. Dies hat sich durch den Einsatz des digitalen Prozesswassermanagements von Rösler Smart Solutions geĂ€ndert. Die ĂŒbersichtliche Auswertung und die leicht verstĂ€ndlichen, direkt umsetzbaren Handlungsempfehlungen vom „digital Guide“ sorgen dafĂŒr, dass die ProzesswasserqualitĂ€t stabil ist und damit auch die TeilequalitĂ€t. Nacharbeiten und Ausschuss haben sich nun um bis zu 50 % reduziert. Durch stabileren Prozess Wirtschaftlichkeit erhöht mit digitalem Prozesswassermanagement Bei der Wegmann Automotive GmbH, WeltmarktfĂŒhrer fĂŒr Auswuchtgewichte, erfolgt die Aufbereitung des Prozesswassers durch eine vollautomatische Zentrifuge. Den Prozess hatte der Mitarbeiter eigentlich auch gut im Griff. Trotzdem entschied man sich fĂŒr den Einsatz des Rösler Smart Solutions. Denn aufgrund unterschiedlicher Anforderungen – die Gewichte aus Stahl erhalten im Gleitschliffprozess einen Korrosionsschutz, bei den Teilen aus Zink muss fĂŒr eine nachfolgende Beschichtung eine vorgegebene OberflĂ€chenspannung erzielt werden – fĂŒhrte eine zu hohe oder zu geringe Compound-Konzentration zu Nacharbeiten und Ausschuss. Eine mikrobiologische Belastung, die den Korrosionsschutz beeintrĂ€chtigen kann, hatte man nicht im Blick. Auch hier sorgt das interaktive Prozesswasser-Monitoring mit Rösler Smart Solutions fĂŒr einen stabileren Prozess sowie eine erhöhte Wirtschaftlichkeit.

How to Use a Vibrascope to Measure Vibratory Bowl Amplitude and Frequency

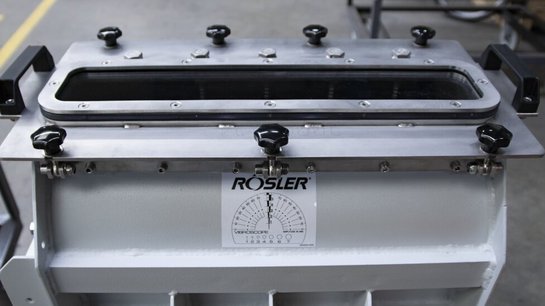
When it comes to mass finishing , amplitude and frequency require balance and careful consideration. Amplitude is a measure of movement and intensity while frequency refers to the rate of repetition. The wrong amplitude, for example, can create lackluster finishing results and longer processing times if it is too low. If too high, it can cause unnecessary wear and tear on the machine. Creating Vibratory Energy Whether rotary or tub style , mass finishing vibrators always include two key components: a work bowl containing the finishing media and the work pieces. Firmly attached to this work bowl is a vibratory drive system generating the energy to put the media and work pieces in motion. The work bowl with an attached vibratory drive system sits on a number of coil springs – in some cases on air cushions – which in turn sit on a machine base. The springs, respectively, act as air cushions allowing the work bowl to “free float” up and down within a certain distance. Example of vibratory drive The force from the vibratory drive system moves the media and work piece mix within the work bowl. Depending on the type of finishing machine, this force is generated by vibratory motors or electric motors driving a shaft with one or multiple imbalance units attached to it. Imbalance units are made up of a rotating shaft with out-of-balance counterweights at each end of the shaft. Due to its imbalance, the rotating shaft causes an intense wobbling effect. Common drive systems in vibratory bowls and tubs include foot motors for small tub vibrators, flange motors for rotary vibrators, and multiple imbalance units with electric drives for large tub vibrators. The Effects of Vibration Since the work bowl with attached vibratory drive system is loosely sitting on the coil springs or air cushions, the energy induced by the vibratory drive system causes the work bowl to move up and down within a relatively narrow distance band at the speed of the rotary drive system. The maximum up and down displacement of the vibrating work bowl from its position of rest is an indicator of the vibratory intensity and is called amplitude. Measuring & Reading Amplitude Understanding your machine’s amplitude is part of the process to dialing in precise surface finishing results. The amplitude – actually the double amplitude from upper to lower peak – is mostly measured in mm. In finishing vibrators, the amplitude is usually between 3 and 6mm. Rosler uses a visual devise called a vibrascope, a sticker applied to the outside wall of the work bowl, to visually measure amplitude. This sticker contains a row of 7 circles with diameters from 1 to 7 mm. Example of Rosler's Vibrascope sticker The simplest way of reading the amplitude is by observing the vibroscope sticker as the machine is in operation. The vibration of the work bowl has the visual effect of showing two rows of circles, with some circles being completely apart and some overlapping. The two circles which are apart but nearly touch each other represent the observed amplitude value. Adjusting Amplitude The vibratory intensity or amplitude of a machine is determined by three factors. Adjusting one or more of these factors will adjust the resulting amplitude. Speed of the Vibratory Drive System – Higher rotary speeds produce higher amplitude. Mass of the Imbalance Weights – Heavier imbalance weights produce higher amplitude. Angle or “Lead Angle” Between the Two Imbalance Weights – Smaller angles produce higher amplitude. The highest intensity is produced at zero degrees, while the lowest – practically no vibration – is produced at 180 degrees. Rosler advises adjusting one factor at a time for the most accurate fine tuning as well as safety and longevity of the machine. The speed and amplitude in finishing vibrators cannot be increased beyond a certain value; otherwise the machine would destroy itself. The acceleration, consisting of rotary speed and amplitude must not exceed 6g. At high rotary speeds, the imbalance weights must be set for a low amplitude (mass of the imbalance weights and lead angle). At lower speeds, the imbalance weights can be set for a higher amplitude. The Rosler Advantage Machines built by Rosler run with more frequency and less amplitude, meaning our media contacts a workpiece more times and is gentler than competing machines. This unique advantage of Rosler equipment creates less wear on media and machines while producing greater longevity. The ability to reduce amplitude yet deliver the desired surface finishing produces less machine shaking and part damage while slowing the rate of machine wear. When using vibratory bowls and tubs, most of Rosler’s competitors hit harder. While impressive, the force of those hits may not produce the most efficient results. Finding the Right Settings In the above graph, the numbers highlighted in yellow are the optimal combination of amplitude and frequency. Amplitude settings depend on the machine set-up, workpiece condition, and desired outcome. Not sure what amplitude is best for your unique needs? Trust the experts at Rosler to conduct a trial and dial in the results before you purchase a machine. The Rosler Way Whatever your mass finishing needs are, you can count on Rosler to help you find a better way. Contact us today to discuss your unique challenges and request a free trial in one of our Customer Experience Centers .

New Deflashing Equipment Assists 30-year Customer Increase Production

For over 30 years, Berker GmbH & Co KG (Berker) has trusted Rosler shot blasting equipment in its manufacturing processes. A member of the Hager Group since 2010, Berker is one of the leading manufacturers of high-end electrical components, from timeless classical switches to intelligent electrical systems for buildings. The company also supplies switches for electrical appliances and automobiles. The Situation Berker primarily uses continuous feed systems such as loop and flat belt machines to deflash plastic components including switching elements, electrical outlet covers, frames, and more. Increased production volume at its Wenden-Ottfingen manufacturing location led Berker to decide to invest in an additional shot blast machine in 2018. The new investment was intended to replace an existing continuous feed loop belt system with the latest deflashing technology. Its specifications called for increased capacity and high equipment availability. The Solution After the capacity requirements had been established, Rosler developed a system concept that fully met the customer’s technical and economic demands known as the RSBS 1702 continuous feed loop belt blast machine. Equipped with two direct-drive blast turbines , the new Rosler machine produces excellent deflashing results combined with an extremely high degree of process stability. The machine includes a host of technical features including modern PLC controls, an optimized media cleaning and recycling system with a vibratory screen and air wash separator, a sensor-controlled media replenishment unit, automatic replenishment and mixing of anti-static compounds, noise protection, an automatic standby module, and a dust collector. The new machine design also allows the automatic deflashing of large work pieces which could not be handled with the old equipment and has been in operation since 2020. The Advantages Rosler is grateful to have the opportunity to assist a 30-year customer achieve new efficiencies even in the midst of a global pandemic and labor shortage. Automated aspects of Berker's new system went beyond improved efficiency and capabilities to provide an additional advantage in the reduced need for manual labor. Like many employers, Berker has faced increasing competition for manpower. The use of work piece handling systems, conveyor belts, and robots have helped bridge the gap in human resources and maintain production rates. Additionally, in the world of manufacturing, this mitigation of human intervention offers even greater and more measurable efficiencies and consistent quality. The Rosler Way “Finding a better way
” is more than a motto at Rosler; it’s our mission. With more than 80 years of experience and a portfolio containing more than 15,000 equipment and consumable products , solving challenges is what we do. Contact us to learn how we can help you achieve more efficient, automated surface finishing.