Solution Finder
SOLUTION FINDER

La vostra guida nel mondo dei prodotti Rösler

Con pochi clic troverete la macchina giusta per le vostre esigenze!

Risultati: 237 Articolo

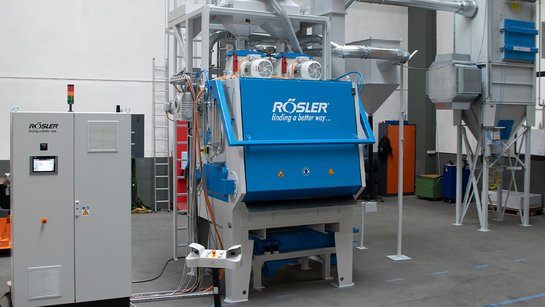
Wet Blasting Equipment & Media, Part 4 – Internal Cleaning, Rebuilds Prolong Machine Lifetime  

While highly effective in a number of applications and industries, wet blasting can be a messy process. Unlike dry shot blasting which produces dust, wet blasting generates a mix of media, dirt, and debris mixed with water mist. If this water/particle mix is not removed properly the machine itself may be soiled to the point that it cannot be used. Mist which escapes the machine can also cause health hazards to personnel and other equipment in the area. Rosler builds its wet blasting machines with usability and safety in mind, factoring in precautions and cleaning functions to prolong the machine’s use and ensuring a clean, safe work environment. Internal Cleaning Rinse systems flush out contaminants including dirt, broken down media, and oil from the blast cabinet. After each blast cycle the inside of the wet blast machine must be cleaned by completely rinsing it down with clean water. High-pressure spray nozzles are installed to rinse the wet blasting machine’s viewing window. During the blast cycle and as needed, high-pressure spray nozzles rinse off any dirt from the viewing window. Water mist from processing as well as the internal cleaning process is continuously removed from the blast cabinet by a suction fan equipped with a filter which removes contaminants from the water. Rebuilding Established Systems Blast machines are often a considerable investment for companies. When these highly specialized and high-investment pieces of equipment start to show signs of wear and underperformance, expert surface finishing companies such as Rosler can help prolong the life and effectiveness of your investment by repairing and rebuilding a machine instead of replacing it. Cost is often the biggest factor considered when rebuilding a blasting machine. Generally, rebuilds offer shorter turnaround times than buying a new machine. Rebuilds also come with the added benefit of not needing to integrate a new process since the process already includes a proven shot blasting process. The Rosler Way We have the experience and expertise to meet your wet blasting needs. Rosler partners with you to find a better way, the best machine, and the best finishing results. Contact us today to discuss your unique challenges. Previous posts in the Wet Blasting Equipment & Media series include: Part 1 – “Machines Range in Complexity, Uses.” Part 2 – “Technical Components Combine for Systematic Success.” Part 3 – “Maintain Slurry Concentrations for Finishing Consistency.” The final post will be: Part 5 – “Careful Media Selection, Additive Use Impact Results.” Sign up for enews alerts to be notified of new posts!

Automotive Manufacturer Partners with Rosler for Fast Processing, Long Wear Life

True to our “finding a better way
” motto, Rosler partnered with thyssenkrupp AG to create a continuous flow shot blasting operation for the fastest crankshaft forge shop in the world. World renowned for its drive trains, chassis, and automobile manufacturing equipment, the automotive division of thyssenkrupp AG significantly contributes to the technical progress and efficiency of motor vehicles. The thyssenkrupp Gerlach GmbH plant in Homburg, Germany, is a leading partner for the development of automobile engine components, offering a full-service package ranging from component design, prototype fabrication, and full-scale production. Developing a Solution To improve cost efficiency at its Homburg plant and to meet all customer requirements, thyssenkrupp AG installed its high-tech “production line 19” for forged crankshafts for engines with one to four cylinders in 2016. For this line, Rosler developed an innovative shot blast equipment concept known as the Rosler RKWS crankshaft shot blasting system . At the beginning of the manufacturing sequence, bar blanks are cut to length. They are then heated in an induction oven before being shaped in a 6,500-ton press. In the last step, the crankshafts undergo a blast cleaning process in a shot blast machine. Using a unique equipment concept for the final blast cleaning step, Rosler engineers created a system for handling different work piece sizes without time-consuming retooling of the work piece holders. This innovation helped reduce the cycle time to less than 10 seconds, which in turn allowed the manufacturing operation to be run in a continuous flow. The result of the comprehensive cooperation between thyssenkrupp AG, Rosler, and all the other partners created the fastest, most modern crankshaft forge shop in the world capable of producing a finished component for its customers every 7.5 seconds. Crankshaft after surface finishing Delivering Convenience & Longevity Our innovations go beyond world records to provide long-lasting value and dependability. The RKWS system was also designed for long life and easy maintenance. The three blast chambers and the work piece load/unload chamber are arranged in a circle around a rotary drive equipped with an asynchronous servo motor with an extremely high overload reserve. Blast media is accelerated and thrown by Rosler Gamma G blast turbines equipped with a unique Y-shaped throwing blades. Rather than being made of chilled iron castings typically used in conventional turbines, critical wear components of the turbines are made of forged tool steel. This results in a much longer uptime of the throwing blades whose curvature produces a much higher throwing speed than straight throwing blades. In addition, the symmetrical Y design allows the use of both blade sides. The combination of more wear resistant material and the blade geometry result in up to three times longer usable blade life. Another feature of the Gamma G turbines is their easy maintenance. Turning the blades around or exchanging them can be done from the top of the turbine housing without having to dismount the impeller, control cage, and the media inlet tube required with conventional turbines. The RKWS is equipped with 12 Gamma G turbines, each with an installed power of 22 kW. The turbines, evenly placed on the three blast chambers, are capable of throwing the large steel shot onto the entire surface area of the crankshafts with a speed of 80 meters per second. This results in a complete removal of forging scale and other surface contaminants. By utilizing highly wear resistant material for all components exposed to the large cast steel shot and the removed forging scale, the RKWS shot blast system’s external workings are protected from excessive wear. The three blast chambers are lined with wear resistant hardened steel. Media augers are made from special steel that is predominantly utilized in the mining industry. Technical characteristics of this material are its extreme toughness and its remarkable hardness of 600 Vickers providing it with a considerable structural strength. Planning Proactive Maintenance Thyssenkrupp AG’s “production line 19” processes the entirety of the company’s customer orders within 21 shifts per week, posing a considerable organizational challenge for the thyssenkrupp Gerlach GmbH maintenance department. In order to manage time for the equipment upkeep, the maintenance team utilizes a TBM (time-based maintenance) system. Within a pre-determined time span, a recurring time window is defined for all inspection and maintenance activities as well as any required repairs including the replacement of spare parts. The time management allows requisitioning all repair materials in advance and facilitates the effective assignment of the maintenance personnel at thyssenkrupp Gerlach GmbH in Homburg. Stocking Spare Parts Planning certainty for the entire manufacturing line along with consistently high product quality is a high priority at thyssenkrupp Gerlach GmbH. For this reason, essential wear and spare parts for all machines were determined jointly with the equipment suppliers and stocked on-site in Homburg. To define the specific requirements for the crankshaft shot blast machine, the customer relied on the experience of the Rosler service department. Based on the customer specifications, our service experts conducted a risk and wear analysis using an ultra-modern simulation of the blast media recycling process allowing them to determine the wear intensity for every single component. Based on the results of the analysis a comprehensive list of recommended spare parts was prepared including wear parts such as protective wear plates, etc. The Rosler Way Working with an experienced supplier is the best way to develop and maintain a shot blasting operation. From selecting the right type of machine for your needs to suggesting everyday actions to ensure repeatable results and extended uptime, Rosler develops lasting solutions. Contact us to learn how we can put our surface finishing expertise to work for you!
Tumble belt blast machine

Tumble belt blast machine for coating preparation

Blast cleaning of springs prior to coating Shot blasting is the most common pre-treatment technology to prepare the surface of technical springs for subsequent coating operations. In a newly established manufacturing line for compression springs this cleaning operation takes place in a Rösler tumble belt blast machine. Within short cycle times the custom-engineered RMBC 4.2-HD produces surfaces that are perfectly prepared for the subsequent coating operation. Oil carried into the shot blast process, is neutralized and, through the media cleaning system, separated from the blast media. The Baumann Springs Ltd., located in Ermenswil, Switzerland, is a global leader in the production of springs and all kinds of stampings. This family-owned company was founded in 1886 and ever since has been managed by the family, today in the fifth generation. Baumann Springs is specialized in the development and production of custom-engineered products with tight dimensional tolerances and high demands for process stability in the automobile industry, medical engineering and other markets. The products are manufactured in 11 plants in Europe, Asia and North-America. Shot blasting solution for a new production line In 2021 the plant in Stare Mesto in the Czech Republic established a new production line for different types of long compression springs made from spring steel EN 10270-2. For cleaning and texturing (roughening) the surface of the springs prior to coating, the company purchased a tumble belt blast machine, model RMBC 4.2-HD, from Rösler . Claudio Hertig, project manager global operations at Baumann Springs, explains: „For this challenging task we had discussions with several equipment manufacturers and requested quotes from three of the suppliers“. “The Rösler solution impressed us not only because of the design of the equipment but also its functionality. Another positive factor was the sturdy machine construction. To familiarize myself with the suppliers, I visited all three companies and prepared a detailed technical comparison. Last-but-not-least, our good experience with Rösler equipment already running at some of our facilities and the global presence of the company, also played a role in our decision for Rösler”, continues Mr. Hertig. Equipped for short cycle times and clean results The RMBC 4.2-HD was painted per customer specifications and is equipped with special technical features. It allows the blast cleaning of complete batches of loosely tumbling compression springs with batch weights of up to 1,000 kg. Two Gamma 300G turbines , each equipped with a power of 11 kW, ensure a high shot blast intensity. These high performance turbines, developed by Rösler, are equipped with curved throwing blades in “Y” design. Compared to conventional turbines the specially calculated blade curvature generates very high media throwing speeds resulting in an up to 20% higher blast performance and, consequently, shorter cycle times. All this is achieved with a lower energy consumption. Moreover, the special “Y” design of the throwing blades allows the use of both blade sides. This practically doubles the usable life of the throwing blades. A quick-change system permits a quick blade change without the need for dismounting the turbine from its housing. The blast process is further intensified and accelerated by the integrated blast media deflectors. These special compressed air nozzles are causing an additional blast media movement. The automatic blast media flow control allows not only the monitoring but also the precise adjustment of the media flow to the respective work pieces. The media replenishment takes also place fully automatically. An additional automatic dosing system allows the application of a powder cleaning compound in the blast chamber to catch and discharge any oil that may be carried into the shot blast machine by the work pieces. It should be noted that the powder compound does not affect the functionality of the blast media: In the air wash separator of the media cleaning system the powder is completely separated from the blast media. Since the machine was also intended for stripping the coating buildup from the work piece carriers used for the coating operation, the dry dust collector is equipped with explosion protection features. In order to minimize machine downtimes due to wear, the inside of the blast chamber is lined with easily replaceable 6 mm thick highly wear-resistant manganese plates. The left and right side of the media discharge opening of the turbines is equipped with additional wear plates. These bundle the media stream and prevent this section of the blast chamber to be attacked by the blast media. Finally, the barrel heads, also made from manganese steel, are equipped with a PU coating providing an additional wear protection in the primary blast zone. This helps to further extend the equipment uptime. Claudio Hertig concludes: „The comprehensive experience and know-how of Rösler with the production of such machines is an invaluable advantage that helps improve the overall efficiency of the equipment. In addition, the global Rösler technical service allows us to work in other plants with the same processes and machinery and have them maintained by local Rösler service engineers”.

Mass Finishing Process Water, Part 2 – Maintain Adequate Drainage to Protect Your System

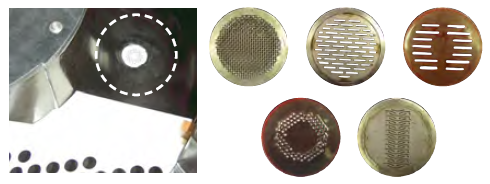
Numerous functions and calibrations factor into developing a precise and stable mass finishing process. From media and compounds to work piece characteristics and processing times, successful finishing requires each process aspect to be carefully monitored and evaluated. When it comes to process water flow rates, poor drainage from the machine can cause quality control issues as well as equipment damage and costly downtime. While simple in their function, drains play an integral role in regulating the flow of process water out of the machine. With the exception of intentional “flooding” of the process bowl for sharp work pieces, the same amount of compound and water entering the machine must be flushed out again. Otherwise, contaminants in the form of dirt, media, metal fines, and, frequently, oil will accumulate in the process water. Since this buildup can cause the finishing process to deteriorate and even collapse, mass finishing machines must have sufficient drainage! With more than 80 years of experience, Rosler can expertly design mass finishing technology and troubleshoot issues to protect your system for the life of the machine. Machine Features Most mass finishing machines, including rotary and tub vibrators and drag‐ , plunge‐ , and surf‐finishers have special drainage screens built into their work bowls. High-energy centrifugal disc finishing machines differ since the “dirty” process water is evacuated through the gap between spinner and work bowl. Drain types used in rotary vibrators. Made from plastic such as polyurethane or stainless steel material, these drains must allow process water and media debris to be flushed from the system while retaining usable media mix and the work pieces. Machines utilizing small media, including steel media for ball burnishing or pressure deburring , always require more drains since small media has a much higher water retention rate than large media. Regardless of the media size, drains can be easily plugged with media debris, flashes from die castings, small metal pieces, etc., and it is essential to make sure that the drains are regularly inspected and cleaned. Drain for undersized media seperation in the work bowl. Manual Evaluation Taking action to prevent process failure, machine damage, and costly repairs and downtime will improve process results and machine longevity. To ensure proper process water drainage: Make sure that the work bowl of your mass finishing machine contains enough drains. If additional drains are needed, they can be easily installed while the work bowl is being relined. Alternatively, a suction pump can be installed for faster evacuation of the process water, if needed. Regularly inspect the machine drains and make sure that they are in good condition, functioning properly, and removing debris appropriately. Install drains with bigger or differently shaped holes if plugging occurs. The Rosler Way Working with an experienced supplier is the best way to develop and maintain a mass finishing operation. From selecting the right type of machine for your needs to suggesting everyday actions to ensure adequate drainage, Rosler develops lasting solutions. Contact us to learn how we can put our surface finishing expertise to work for you! The complete Mass Finishing Process Water Series includes: Part 1 – Understand When to Balance Flow or Flood the Process Bowl . Part 2 – Maintain Adequate Drainage to Protect Your System .

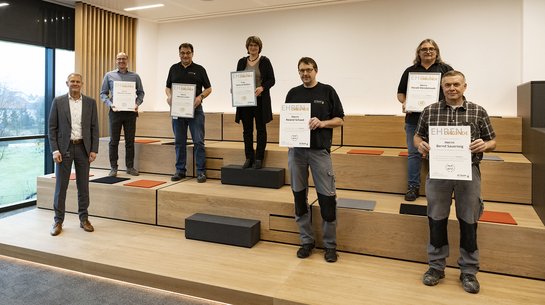
820 Jahre Betriebszugehörigkeit: Die Rösler OberflÀchentechnik GmbH ehrt 67 langjÀhrige Mitarbeiterinnen und Mitarbeiter

Die Rösler OberflĂ€chentechnik GmbH freute sich auch in diesem Jahr wieder 67 Mitarbeiterinnen und Mitarbeiter fĂŒr deren insgesamt 820 Jahre Treue und LoyalitĂ€t zu ehren. Allerdings mussten, wie bereits im Vorjahr, die Feierlichkeiten coronabedingt in kleinem Rahmen unter strenger Einhaltung der Hygienevorschriften stattfinden. Die traditionelle Ehrungsfeier der Jubilare sowie die Verabschiedung treuer Mitarbeiterinnen und Mitarbeiter in den Ruhestand sollte in diesem Jahr erstmalig in dem neuen und modernen Betriebsrestaurant der Rösler OberflĂ€chentechnik GmbH am Standort Memmelsdorf stattfinden. Doch auch in 2021 konnte die Feierlichkeit aufgrund der Corona-Pandemie leider nicht in dem ursprĂŒnglich geplanten Rahmen abgehalten werden. Um den Jubilaren trotzdem die verdiente, persönliche WertschĂ€tzung gegenĂŒberzubringen, fanden die Ehrungen in kleinen Gruppen durch die entsprechenden FĂŒhrungskrĂ€fte unter Wahrung der erforderlichen Hygieneregeln statt. In diesem Zusammenhang dankten die jeweiligen FĂŒhrungskrĂ€fte im Namen der Rösler OberflĂ€chentechnik GmbH ihren langjĂ€hrigen Mitarbeiterinnen und Mitarbeitern fĂŒr deren LoyalitĂ€t und Engagement. Die Rösler OberflĂ€chentechnik GmbH gratuliert 
 zum 40-jĂ€hrigen BetriebsjubilĂ€um: im Werk Memmelsdorf: Harald Wendelmuth und Helmut Lutter sowie Gertrud RĂ€dlein aus dem Werk in Hausen. 
 zum 25-jĂ€hrigen BetriebsjubilĂ€um: Roland Schaad, Michael Striebe und Edmund HĂŒbner – alle tĂ€tig im Werk Memmelsdorf – sowie Bernd Sauerteig im Werk Hausen. 
 zum 10-jĂ€hrigen BetriebsjubilĂ€um: im Werk Memmelsdorf: Daniel Bahls, Gerhard Bauer, Michael Berwind, Jens Beugnies, Marcus Breitfelder, Patrick Diez, Stephan Dohles, Ivan Drescher, Thilo Friedel, Florian Gries, Stefan GrĂŒndel, Marco Habermann, Stephan Hacker, Adrian HĂ€fner, Viktor Heinrich, Herwig Heiser, Angela Herr, Simone JĂ€ger, Woldemar Jung, Stefan Kalb, Manuel Kambach, Daniel Keim, Tom Kollacks, Manfred Kohmann, Tobias Kurzendörfer, Andreas Lamm, Johannes Leicht, Denis Leidner, Stefan Mantey, Iris Martin, Sebastian Martin, Katharina Meixner-Pelkner, Andreas Popp, Marcus Roth, Benedikt Reubel, Patrick Rösler, Lisa Schad, Anna Schlawne, Christian Schmidt, Astrid Schwappach, Oleg Strauch, Peter Strohschein, Benjamin SĂŒlzle, Oxana Walinger, Rebecca Walther, Dimitri Wander, Bernhard Waschkowski, Dimitri Winterholler, Christoph Wunner und Thomas Zimmermann. im Werk Hausen: Vladimir Bauer, Steffen Beyer, Fabian Heer, Alexandra Janson, Andreas KĂ€stner, Bernd Landvogt, Mario NĂŒĂŸlein, Sabine Precklein, Viktor Schell und Marion Zeller. Nach langjĂ€hrigem verdienstvollen Einsatz wurden Detlef Bauer, Josef Bornschlegel, Albin Dorsch, GĂŒnter Elflein, Adelgunde Fischer, Ralf Gutmann, Uwe Hein, Gerd Leipold, Uwe Michael, Josef Schnapp, Siegfried Schrenker sowie Hartmut Tremel in den Ruhestand verabschiedet. Rösler stellt die Weichen fĂŒr eine erfolgreiche Zukunft In seinem traditionellen Weihnachtsgruß bedankte sich Stephan Rösler, GeschĂ€ftsfĂŒhrender Gesellschafter der Rösler OberflĂ€chentechnik GmbH, bei allen Mitarbeiterinnen und Mitarbeitern fĂŒr deren tatkrĂ€ftige UnterstĂŒtzung und LoyalitĂ€t in einem Jahr, welches aufgrund der Corona-Pandemie und der damit verbunden wirtschaftlichen Situation strukturelle Anpassungen im Unternehmen erforderlich machte. „Doch nur wer sich Ă€ndernden Rahmenbedingungen nicht verschließt und entsprechend reagiert, kann langfristig und nachhaltig erfolgreich sein“, so die Maxime von Stephan Rösler. Dass die getroffenen Maßnahmen erste Wirkung zeigen, beweist eine deutlich verbesserte Auftragslage, wenn auch nicht auf Vorkrisenniveau. Zudem investierte das Unternehmen auch in Krisenzeiten wieder in wichtige Zukunftsthemen wie z. B. die Digitalisierung und Automation, sowohl in Form der angebotenen Produkte als auch im Unternehmen selbst. Als Teil des produzierenden Gewerbes ist sich die Firma Rösler aber auch seiner gesellschaftlichen Verantwortung gegenĂŒber dem Thema Nachhaltigkeit bewusst und ist deshalb seit kurzem Teil der VEA-Initiative „Klimafreundlicher Mittelstand“. DarĂŒber hinaus ist das Unternehmen nun bei der CDP gelistet, bei der es sich um eine gemeinnĂŒtzige Organisation handelt, die Unternehmen und Regierungen zur Nachhaltigkeit anhĂ€lt und die weltweit fĂŒhrende Plattform zur Offenlegung von Umweltdaten betreibt. Die insgesamt getroffenen Maßnahmen lassen den GeschĂ€ftsfĂŒhrenden Gesellschafter der Rösler OberflĂ€chentechnik GmbH optimistisch in die Zukunft blicken.
Wet Blasting Equipment & Media, Part 3 – Maintain Slurry Concentration for Finishing Consistency

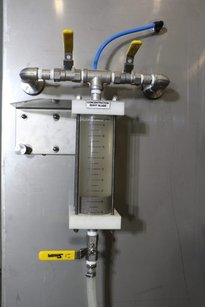
Wet blasting propels a mixture of media and process water at the surface of a work piece to provide cosmetic (anti-glare) finishes, surface smoothing , deburring , de-powdering, decontaminating, and cleaning after casting, welding, machining, and additive manufacturing . Useful in a variety of industries , this specialized form of shot blasting relies heavily on the media and water mix known as wet blasting slurry to work in tandem with the machinery in order to deliver the desired finishing results. Rosler has extensive experience developing wet blasting systems as well as providing guidance on slurry concentrations and supplying the necessary consumables . Slurry Characteristics Wet blast schematic The slurry is created in a tank housed within the blast chamber by mixing water and an abrasive media. A special pump delivers the slurry to the blast gun where it is then propelled onto the work surface using compressed air. High-speed impact of the slurry on the surface of the work piece creates the desired blasting effect, be it cleaning, coating preparation, cosmetic surface texturing, or peening . Wet blasting in process The concentration of abrasive media in the slurry usually amounts to 10-40% by volume, for example, 20% media and 80% water, etc. Establishing the ideal concentration may require extensive processing trials initially or if the work pieces and their original condition change. In these cases, contact the machine manufacturer for guidance. Controlling Slurry Concentrations Regular and gradual slurry loss is expected even in a well-calibrated finishing operation. During the blast process the media wears by becoming smaller or fracturing. These smaller and irregular pieces must be removed from the system. To make up for this loss and removal of undersized media, new media must be added. Maintaining a very tight tolerance range of 1-2% in the prescribed slurry concentration is required to achieve consistent results. For smaller systems, maintaining slurry concentration can be done by visual inspection of the media-to-water ratio in the graduated viewing glass of the concentration measurement unit and manually adding media as needed. In larger blast systems, the slurry concentration is controlled automatically with an ultrasonic level sensor, a weighing system, or continuous density measurement. Adding media to the desired concentration level can be done manually or through an automated, PLC-controlled media adder. Manual slurry concentration measurement unit The Rosler Way Rosler has more than 80 years of experience in shot blasting. Whatever your wet blasting challenges are, we are confident that we can deliver a solution. Contact us to discuss your needs today! Previous posts in the Wet Blasting Equipment & Media series include: Part 1 – “Machines Range in Complexity, Uses.” Part 2 – “Technical Components Combine for Systematic Success.” Upcoming posts will include: Part 4 – “Internal Cleaning, Rebuilds Prolong Machine Lifetime.” Part 5 – “Careful Media Selection, Additive Use Impact Results.” Sign up for enews alerts to be notified of new posts!
MultiShape ceramic media

Innovative consumables for mass finishing operations

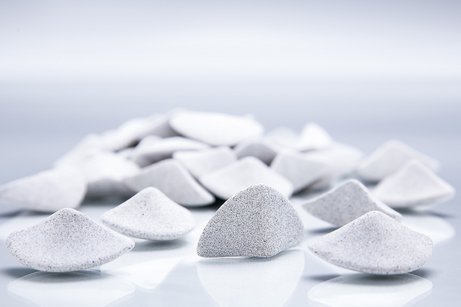
Simple steps to improve finishing results, sustainability and efficiency When it comes to achieving the required quality of products by surface refinement, the mass finishing technology can be used for a broad range of different finishing tasks. With its comprehensive research & development activities the Rösler OberflĂ€chentechnik GmbH continues to generate new technical highlights not only for the machine technology but also for the respective mass finishing consumables. Three recently introduced products make it possible to significantly improve the finishing results, the process consistency, the cost efficiency and sustainability of mass finishing operations. At the same time, they open the door for new applications, for example, the finishing of complex, cup-shaped work pieces. The mass finishing technology can handle all kinds of surface finishing tasks ranging from the simple deburring/edge radiusing and surface grinding to high gloss polishing of mass-produced bulk goods and single components. It can even create special effects on the surface of the work pieces. Of course, like any other industrial processes, mass finishing operations must comply with all kinds of requirements such as high quality standards, process stability, work piece traceability and cost-efficiency. More recently optimal resource utilization and sustainability have become a focal point in numerous industries. And finally, the rapidly growing automatization and digitization of manufacturing operations also calls for specially adapted solutions for mass finishing operations. For decades the Rösler OberflĂ€chentechnik GmbH has met these challenges with comprehensive research and development in the equipment sector as well as in the fields of process and automation technology and consumables. In this context a big advantage is that Rösler is producing all its consumables in-house. RĂŒdiger Böhm, global R & D manager at Rösler, explains: „We study the technical trends and requirements in numerous industries and markets extensively. Our findings are then systematically utilized for the development of innovative products to provide a significant incremental value to our customers and to expand the application range for the mass finishing technology”. MultiShape – a unique media shape that makes the impossible possible Such an innovation is the new MultiShape ceramic media. Compared to all other products currently available in the market, this media has a patented shape without any flat, parallel surface areas. On the one hand this unique design prevents media lodging in the work pieces, which can occur particularly in case of complex work pieces. Such lodged media can severely affect the finishing process and must frequently be removed by hand. On the other hand, the shape with its rounded surface areas allows the surface refinement of work pieces, which to-date could not be handled by mass finishing at all or only with very complicated operational setups. This includes components with difficult-to-reach surface areas like tight radii, undercuts, notches and slits, which can frequently be found in stamped and bent components. The unusual ceramic media also allows the effective and homogeneous finishing of external and internal surface areas on tube segments and cup-shaped components like housings and deep drawn parts. Compared to traditional ceramic media, the new product is also characterized by a faster and more dynamic motion of the work piece/media mix and a higher material removal rate. This results in up to 10 % shorter finishing times. Therefore, the new media represents a significant contribution towards higher productivity and cost-efficiency. Another important attribute of the MultiShape media are its uniform wear characteristics. This excellent shape retention feature allows a longer media use, which is positively affecting the operating costs. The grinding intensity can be adjusted to the respective finishing application through different ceramic compositions. Mass finishing without foaming – increased process stability, efficiency and sustainability Unwanted foam is a common phenomenon in mass finishing processes with plastic media, even with foam-reduced media versions. Foaming can be problematic because, acting as a buffer between the work pieces and media, it reduces the grinding performance and material removal rate. This can diminish the process stability, and the processing aim can frequently no longer be achieved within the defined cycle time. Moreover, the foam containing metal and media fines contaminates the surface of the finished work pieces. The foam also causes a deterioration of the process water cleanliness, requiring a higher compound dosing rate and forcing the user to replace the process water more frequently. Last-but-not-least, foam discharged from the mass finishing machine contaminates the working environment. In the past the users tried to control the foaming by adding special chemical compounds. But this was not very successful, caused additional costs and reduced the process sustainability. With its non-foaming plastic media, the so-called “N” version, the R & D department at Rösler has now developed a better solution. Christian Höhn, head of the technology management at Rösler, explains: ”Prior to introducing the product in the market we conducted extensive field trials with special pilot users. The trials proved convincingly that the non-foaming plastic media has the same grinding characteristics and performance as the standard product”. The trials also demonstrated that with the newly developed media the mass finishing processes are running much more stable, and the required results are achieved in shorter cycle times. This positive effect regarding cost-efficiency and sustainability is augmented by a longer usable life of the media and process water and a reduced compound usage. ”Because of the disruptive foaming many users had been using ceramic media, even though this was not the best option. For these users the non-foaming plastic media version is a great opportunity to optimize their finishing processes”, concludes Christian Höhn. All plastic media in the comprehensive Rösler portfolio are available in the non-foaming “N” version. Dust-free drying with organic drying media The third new development in the consumables sector in 2021 allows a significant reduction of the dust occurring during drying processes utilizing organic drying media such as maizorb. Even in small quantities the liquid, easily dispensable, Anti-Dust additive significantly reduces the formation of dust. Depending on the operating times and work pieces the additive can be manually added or dosed fully automatically. The Anti-Dust additive is employed in drying operations for metal and plastic components, whenever organic drying media is used. Without negatively impacting the drying performance it guarantees absolutely spot-free surface finishes. At the same time, dust residues on the finished work pieces and the surrounding area are minimized. This also represents a huge step towards a clean, low-dust working environment. Rainer Schindhelm, division manager of the consumables production, explains: „Because it is purely organic and complies with the prevailing food standards, the Anti-Dust additive also represents a significant contribution towards a cleaner environment”. Increasing the productivity of the mass finishing technology, improving overall sustainability and reducing CO2 emissions; these are the main goals of the development work at Rösler in the year 2022. Various solutions from the sectors equipment technology and consumables are already being tested at various customers.
dosing unit RDS-pH 10

Automated dosing system blocks legionella

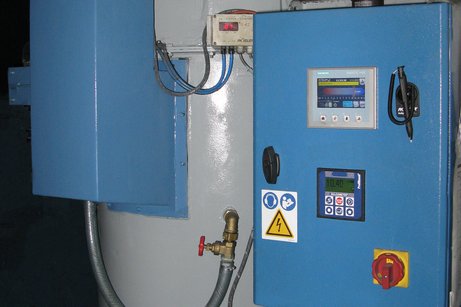
Like evaporation cooling systems and cooling towers, wet dust collectors can be the source of hazardous legionella. To eliminate such a risk for the respective personnel the 42nd BImSchV obliges the operators of such installations to maintain a high degree of transparency and to conduct regular, time consuming and costly controls. The dosing system RDS-pH from Rösler has proven to be a highly effective and cost-efficient alternative to these controls. In combination with a specially developed additive it automatically maintains the pH value of the process water above a level of 10 and, thus, prevents the formation of legionella. The process water in cooling towers and evaporation cooling systems is an ideal breeding ground for legionella and other microorganisms. The same is true for wet dust collectors used for neutralizing the explosive dust created during shot blasting operations with work pieces made from aluminum and other non-ferrous metals. Since the water is sprayed, aerosols containing legionella can contaminate the environment around the equipment and become a health hazard for the personnel working nearby. With the 42nd administrative order regarding the federal emission protection law of Germany (42. BImSchV), in effect since August 2017, comprehensive and strict obligations for the operators of such systems were imposed. For example, their operation must be reported to the authorities, and the process water must be analyzed by an approved test lab during the startup phase. Regular controls during operation According to these regulations, an operating log must be maintained, in which the results of the required regular bi-weekly internal microbiological tests for the presence of legionella are documented. The results of tests conducted by an approved external test lab every three months must also be recorded. Compliance with these requirements can be quite costly! Violations of the 42nd BImSchV regulations and missed deadlines are punishable as legal infractions of the law. Always on the safe side with an automatic dosing system The BImSchV provisions also describe ways to avoid the complicated and costly controls. The regulations do not apply to operators who consistently maintain a pH value of 10 or higher in their process water. However, irrespective of this, an operator log must be maintained and kept up-to-date. For this purpose Rösler has developed the dosing unit RDS-pH 10 and additive RST-P1 allowing the automatic compliance with the BImSchV provisions. The dosing unit, maintaining the pH value of the process water in the required alkaline range, can be connected as stand-alone system to practically any wet dust collector regardless of the manufacturer. It is equipped with a measuring device that continuously monitors the pH value. As soon as the pH level falls below 10, a certain amount of additive is injected to increase the pH value. This prevents the formation of legionella consistently and reliably. The measured values are transferred from the dosing unit to a USB memory drive. The data can then be easily analyzed and visualized with a special Excel tool. This procedure is in full compliance with the requirement to maintain an operating log. Improved safety and cost-efficiency All these benefits convinced Emanuele Cassataro, manager of the die-casting department at the GSB Aluminium GmbH to install the dosing unit. This company, located in Wuppertal, Germany, is utilizing casting, forging and friction welding technologies to make aluminum components for various industries, such as automotive, machine building and medical engineering. About 80 percent of the die-castings made from a variety of aluminum alloys and weighing between five grams and eight kilograms undergo a shot blasting process. A side effect of this operation is the creation of explosive dust that is neutralized by a wet dust collector. Emanuele Cassataro explains: „Initially we had to replace the process water on a weekly basis to prevent the formation of legionella. Naturally, this was quite costly. Therefore, we looked for a simple and inexpensive solution to comply with the regulations of the 42nd BImSchV”. During his search the department manager found out that by increasing the pH level of the process water the formation of legionella can be prevented. Subsequently, the company chose the dosing system RDS-pH 10 from Rösler. Besides its excellent functionality and high cost-efficiency another decision factor for this dosing unit was that the shot blast machine and wet dust collector were also supplied by Rösler. „We prepared a detailed documentation of the technical features of the dosing system for the authorities. For this reason we must no longer conduct internal measurements nor have external test labs conduct any controls”, reports Emanuele Cassataro. In the meantime the dosing system has been in operation for about 18 months. Since its installation the process water did not have to be replaced once. Fresh water is automatically added to offset losses due to evaporation and sludge discharge. The continuous pH measurements of the dosing system and the injection of a suitable amount of additive ensure that the pH value of the process water is always above 10. The department manager concludes: „I am very pleased with this solution. On the one hand the risk of legionella formation has been reliably eliminated. And on the other hand the entire shot blasting operation has become more economical because we no longer have to replace the process water and conduct costly controls. The system works so well that in September 2021 we purchased a second Rösler dosing unit for a wet dust collector from another supplier”.

Mass Finishing Process Water, Part 1 – Understand When to Balance Flow or Flood the Process Bowl

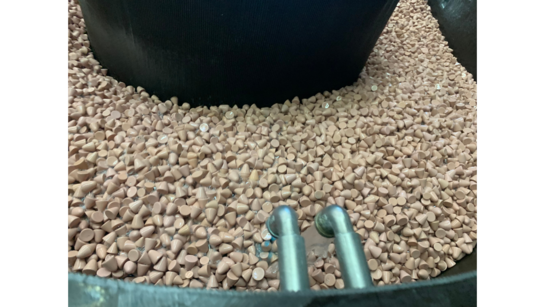
Maintaining the correct compound and water flow rate into a mass finishing machine is essential for the stability and success of a process. If inadequate compound and water are supplied to the machine, results will be more extreme and lead to unpredictable processing times, ineffective finishing, dirty work pieces after finishing, glazed media, and, potentially, a total collapse of the process. Excessive compound and water flow can be equally problematic. Too much water and compound will slow down the movement of media and work pieces in the machine or cause a complete stop. For example, in rotary vibrators the typical spiral movement of the media/work piece mix will give way to an uncontrolled shaking. In centrifugal disc machines , the rotating spinner will slip under the media/work piece mix with no movement at all. Longer processing times, poor finishing results, and even a complete collapse of the process can occur. For the best results and stability, Rosler understands that the flow rate of compound and water into the machine must be equal to the flow rate out of the machine. What Goes In, Must Come Out Compound and water fulfill distinct and important functions. The compound removes stains, dirt, and oil from the work pieces; burnishes and brightens them; and keeps the media clean. The water dissolves and distributes the compound in the machine, serves as a coolant for the finishing process and, above all, flushes out media and metal fines, and other contaminants from the machine. Hence the importance of matching the amount of compound and water entering the machine to what is flushed out. For example, if the drains are plugged with undersized media and debris, the compound/water mixture can become contaminated with media and metal fines and fail to remove oil and contaminants from the machine, jeopardizing results and machine functions. Optimizing Operations Achieving and maintaining a well-balanced process requires proactive evaluation and machine oversight. Key action points include: Regularly monitoring the compound and water flow and make sure that it is as specified. Ensuring that machine drains are not plugged and flowing easily. Installing bigger undersized media screens if drains are easily backed up. “Flooding” Benefits Mass finishing media in a flooded work bowl In some circumstances, it may be advantageous to run a process with high water levels or “flooding” the processing bowl with additional water. Keeping in mind that too much water and compound in the machine can slow or completely stop movement of media and work pieces in the machine, extra process water can be used to provide an extra cushioning effect and reduce machine intensity to create a gentler process. This prevents delicate work pieces from getting scratched or bent and even allows for certain polishing operations. Flooding the processing bowl can also protect the machine itself. For example, very pointed work pieces with sharp edges can undergo an initial deburring process in high water mode to help protect the bowl’s wear lining. Once the sharp points and edges are slightly rounded and pose a lower risk of destroying the wear lining, the processing mode can be switched to a normal water level for additional finishing. High water level mode is primarily utilized in high-energy systems like centrifugal disk finishing machines. Consult with your supplier to determine if running with high water is possible and feasible for your specific application. The Rosler Way “Finding a better way
” is more than a motto at Rosler; it’s our mission. With more than 80 years of experience and a portfolio containing more than 15,000 equipment and consumable products, solving challenges is what we do. Contact us today to discuss your process water challenges! The complete Mass Finishing Process Water Series includes: Part 1 – Understand When to Balance Flow or Flood the Process Bowl . Part 2 – Maintain Adequate Drainage to Protect Your System .

Equipment Investment Doubles Work Piece Longevity at Andersen Steel

Andersen Steel produces agricultural equipment including grubbers, front packers, and stubble tillers equipped with vibration tines for soil cultivation. Their equipment is exposed to extreme loads, causing decreased wear life of parts including the tines. Made using specially arched rolled steel at the company’s Poland plant, Andersen Steel tasked engineers at Rosler with finding a better way to process the tines and improve their wear life. We delivered a solution in the form of two identical machines for blast cleaning and shot peening . Delivering a Solution Compared to flat steel, the rounded edges of the material Andersen uses prevent small cracks from forming during the shaping process. The work pieces pass through a blast machine to remove mill scale and other contaminants before shot peening to further improve their wear resistance. For these dual shot blasting requirements, Rosler suggested two identical Rosler RHBD 13/18 K hanger machines . Successful blasting trials in a Rosler test center helped Andersen realize the advantages of purchasing these Rosler machines by demonstrating that shot peening the work pieces doubled the uptime of the tines. This improvement considerably exceeded the expectations of Andersen Steel and justified their investment in new equipment. Work pieces pass through two identical, subsequently arranged hanger machines for blast cleaning and shot peening in Andersen Steel's RHBD-K shot blasting machine. Technology in Action Each of the hanger blast machines is equipped with eight Gamma¼ 400G turbines featuring installed power of 15 kW each. Compared to conventional blast wheels this uniquely designed Rosler turbine style offers a 15–20 percent higher blast performance with double the uptime of wear parts like throwing blades. Pairs of two turbines located in the four corners of the blast chamber bombard the tines with media . The turbines are positioned to ensure that the individual blast patterns do not overlap, creating perfect blast coverage on the tines. Each blast machine is equipped with eight Gamma 400 G turbines strategically placed to ensure perfect blast coverage on the tines. Since the different work piece types require different media throwing speeds, the turbines are equipped with variable frequency drives. After the shaping process, work pieces are attached to the transport system on special carriers which move the components through the blast-cleaning, shot peening, painting, and drying stages. Vestibules equipped with multiple overlapping curtains are installed on the inlet and outlet side of the blast chamber to prevent blast media from spilling out of the machine. A sensor recognizes when a carrier enters the inlet vestibules and sends a signal to the machine controls to start the blast process. The Rosler Way “Finding a better way
” is more than a motto at Rosler; it’s our mission. With more than 80 years of experience and a portfolio containing more than 15,000 equipment and consumable products, solving challenges is what we do. Contact us today to discuss your shot blasting challenges!

Surface Preparation Standards, Part 2 – Dust Measurements and Considerations

As an expert in the surface finishing industry, Rosler knows that all the expertise in the world won’t do any good if the surface of the work piece is not properly prepared. When it comes to structural steel , we receive many questions about preparation. Among the most common questions is, “ How is the presence of dust on shot-blasted structural steel components evaluated?” Understanding dust considerations and mitigation will help produce higher quality and longer-lasting structural steel components more cost-effectively and safely. The Dangers of Dust Blast-cleaned structural steel surfaces must be completely free of dust to ensure proper coating and painting. Residual dust will reduce the adhesion of subsequently applied coatings and, by absorbing moisture, may promote the corrosion of the blast‐cleaned steel surfaces. The potential accumulation of dust is especially critical on horizontal surfaces, the interior of pipes, and inside structural cavities. Special inspections must be carried out to ensure that such areas are adequately cleaned and free from dust before painting. Standards of Assessment The most common standard of assessment for dust is ISO 8502–3:2017. Also known as the pressure‐sensitive tape method, this ISO standard describes a procedure to test shot blasted steel surfaces for dust and provides a reference description and photo with six dust ratings for comparison. On a scale of 0 to 5, the observation of dust particles and diameter are rated as follows: Visual rust scale 0 – No particles are visible under 10x magnification. 1 – Particles are visible under 10x magnification but not with normal or corrected vision; particles are usually less than 50 ÎŒm in diameter. 2 – Particles are just visible with normal or corrected vision; usually between 50 and 100 ÎŒm in diameter. 3 – Particles are clearly visible with normal or corrected vision; up to 0.5 mm in diameter. 4 – Particles are clearly visible; between 0.5 and 2.5 mm in diameter 5 – Particles are clearly visible; larger than 2.5 mm in diameter Testing for Dust ISO 8502 testing kit Special ISO 8502 kits include a 10x magnifier, adhesive tape to ISO 8502‐3 specification, comparator display board/operating instructions, a dust assessment plate, and 25 test record sheets. Proper procedure is required to accurately test for ISO 8502-3 using the kit. Remove a piece of tape about 8 in (200 mm) long. Place the sticky side of the tape onto the test surface; rub along the length of the tape using constant pressure several times. Pull the tape away from the test surface, compare the dust on the tape with the comparator display board and record the estimated dust rating number. Repeat the test at least three times on the surface being investigated. Minimum Requirements The dust test per ISO 8502‐3 is subjective and does not allow the precise determination of dust on a blast cleaned surface, but the rating can be a very useful approximation when carried out by experienced operators. Painting schedules usually call for shot blasted surfaces prior to painting to be free of dust. A generally accepted rule stipulates that the particle quantity and particle size do not exceed rating 2 of ISO 8502‐3. Rosler blow-off station Removing Residual Dust To remove residual blast media and dust from the work pieces shot blasted steel components are usually passed through a blow‐off station. These stations are frequently combined with a brush‐off system. The Rosler Way Rosler has more than 80 years of experience developing surface finishing technology and systems. We are confident that we can answer your surface finishing questions and develop a solution to meet your needs. Contac t us today to discuss your unique challenges. Additional information about surface preparation standards is available in Part 1 of this series, “Evaluating Surfaces Throughout Finishing Processes.”

Surface Preparation Standards, Part 1 – Evaluating Surfaces Throughout Finishing Processes

Surface preparation can account for up to 40 percent of structural steel painting and repainting jobs and the life of anti‐corrosion coatings on a steel surface largely depend on how thoroughly the surface was prepared before painting. At Rosler , we have extensive experience evaluating structural steel surfaces for coating before and after shot blasting. This knowledge of surface preparation standards and the widely used ISO and SSPC standards guide us in developing systems to expertly prepare and repair structural steel throughout its lifespan. The Standards Evaluating rust and mill scale pre- and post- shot blasting is a must. It is important to clearly specify the quality of the surface prior to preparation as well as the surface conditions after preparation. As a result, standards were developed to visually assess the initial surface conditions and the quality of the required surface preparation relative to the initial steel surface conditions. The dominant and widely used standards for evaluating rust and mill scale are ISO 8501‐1:2007 (based on the Swedish Standard SIS 05 59 00) and the SSPC (Steel Structures Painting Council) . While different in some minor details, these standards are practically identical. Pre-Paint Conditions In specifications relating to the preparation of surfaces prior to painting, the SSPC and SIS designations correspond as follows. Corresponding SSPC and SIS designations Rust Grades The standards identify four initial rust grades based on visual evaluation before surface treatment. The following examples illustrate and describe the four ratings. Visual comparison of rust grades A – The steel surface is covered completely with adherent mill scale and little, if any, rust. B – The steel surface has begun to rust and mill scale has begun to flake from the surface. C – The steel surface on which the mill scale has rusted away or from which it can be scraped, shows little pitting visible to the naked eye. D – The steel surface on which mill scale has rusted away shows considerable pitting visible to the naked eye. Preparation Grades After blast cleaning, the standards define four preparation grades. The appearance of the shot blasted surface must correspond to one of the following descriptions and standards: The cost to achieve longevity of each grade varies and should be considered based on initial cost as well as lifetime costs based on your structural steel’s uses and expected lifespan. Brush‐off – After light blast cleaning loose mill scale, rust, and foreign matter are removed. Despite being the least expensive grade of the four, brush-off preparation may not hold paint and coatings as well as the other grades and often requires more frequent resurfacing. Commercial – Thorough blast cleaning removes almost all mill scale, rust, and foreign matter. While normally adequate in a non-corrosive atmosphere, this grade is a more labor- and cost-intensive option compared to brush-off preparation. Near White – Very thorough blast cleaning removes mill scale, rust, and foreign matter to the extent that the only remaining traces are light stains in the form of spots and stripes. This grade is fully acceptable for most somewhat-corrosive environments. It is the most common preparation grade for ship building and most industrial and commercial weldments and fabrications. White Metal – Blast cleaning reveals pure metal. This grade is very expensive and typically reserved for applications in which the costs of coating failure are catastrophic, for example, for tanks containing highly corrosive, hazardous chemicals. Preparation Grade Examples Based on ISO 850-1 The different preparation grades depend on the initial rust grade. ISO 850-1 standard grades are presented below to provide visual examples. SSPC Vis 1/89 incorporates similar visual comparisons. Visual comparison of preparation grades The Rosler Way Whatever your pre- and post-treatment goals, count on Rosler to help you find a better way. To demonstrate our capabilities, we offer FREE sample processing in our global test centers . Contact us to discuss your surface finishing goals and challenges. Learn more about surface preparation standards in part two of the series, “Dust Considerations and Measurement” , and sign up for enews alerts to be notified of all new posts!