Solution Finder
SOLUTION FINDER

您的罗斯勒产品世界指南

只需点击几下,您就能找到适合您的需求的机器!


结果: 237 文章

Automation, Part 2 – Why Automation is Beneficial for Your Business

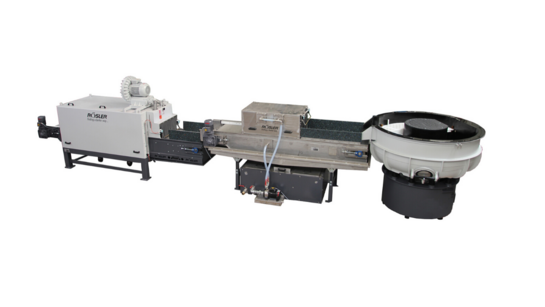
It’s hard to dispute that technology, on the whole, has made our lives easier and more convenient. Myriad functions have been automated – and improved – to mitigate the effects of human intervention. We make purchases more intelligently, we manage data more efficiently, we can control devices with our voices and eye movements, and we ultimately move through life with less left to chance. In the world of manufacturing, this mitigation of human intervention promises even greater and more measurable, efficiencies. At Rosler Metal Finishing , quality improvements and cost benefits that have resulted from the mechanization and automation of mass finishing and shot blasting operations deliver dividends that transcend the manufacturing floor. Rosler Multichannel System Since the first microprocessor-controlled machine appeared on the manufacturing floor in 1974, hundreds of new varieties have been shipped across the world. With each improvement, these automated attendants encompass a larger footprint, are able to handle heavier loads and more axes, and require fewer controllers to do their work, according to a McKinsey study . Automation has revolutionized smaller tasks as well, including simple parts bin handling, lift assists, automatic media adding systems, or multi-step process control systems (like those where noxious chemicals are dosed, without human risk, into the process). So how do these automation upgrades pay off for you? Let’s start by taking a look at where mass finishing and shot blasting has fit into the manufacturing paradigm. Then we’ll dive deeper into the benefits of today’s automated processes which have a lasting impact on the finished product. Rosler R 220 SO System for small parts The Role of Mass Finishing and Shot Blasting in Modern Manufacturing When mass finishing and shot blasting were “invented” years ago, their sole purpose was to replace the tedious job of manual deburring, or the stripping of rust and paint from a surface. Early equipment was simple and required substantial operator involvement, but represented great strides productivity and quality improvement. Over time, both technologies grew into sophisticated surface treatment technologies that have become essential for the proper function of components used across many industries. Today, state-of-the-art mass finishing equipment is used to place the finishing touch on orthopedic implants like knee femorals, tibia plates, or hip stems before implantation. Complex shot peening systems are also used for extending the service life of critical aircraft components. Rosler RMT Multi Tumbler System Mass finishing and shot blasting have made a significant contribution towards zero-defect manufacturing with absolutely repeatable, highly cost-efficient, surface improvement processes. To a large extent, this only became possible through further mechanization and automation. What Are the Benefits of Automation? When deployed properly, automation offers numerous tangible technical and economic advantages, including: Improved surface treatment quality, including tighter tolerances. As an example, the automation of the shot peening of turbine blades has greatly improved the peening quality as measured by Almen values. Consistent, repeatable quality. A stable process environment means no variations in the output. This can be seen with the automated polishing of orthopedic implants in dedicated mass finishing equipment, which delivers consistent high qualities, batch after batch, day after day. Time savings with reduced manufacturing lead times. As an example, the direct linking of the blast cleaning of steel plates and beams and their corrosion protection in a single, automated preservation line process can drastically reduce turnaround times. Rosler KON-RRB Preservation Line with transfer system Improved operational efficiency, which translates to fewer rejects and lower costs. A manufacturer of outboard engines, for example, could reduce its reject rate from 12 percent to 0 by simply converting to an automatic drag finishing process for paint preparation. No need for trained mechanical labor . Automation relieves the pressure of finding qualified, well-trained mechanical labor that understands the complexities of surface finishing in a shrinking marketplace. Cost savings. Automation pays for itself through lower expenditures for personnel, faster turnaround times, and much lower reject rates. Rosler RDGE 800-8 Wire Mesh Belt System Is Automation Always the Best Solution? It’s clear that automated mass finishing and shot blasting systems produce better surface finishes in a consistent, repeatable manner, reduce the finishing costs, and help reduce lead times. Therefore, for industrial volume production, automation is a “no-brainer.” However, for work pieces that are produced in very small volumes or are particularly large, bulky and heavy, partial automation may offer a good compromise. This is definitely the case in prototyping shops or foundries and forges making special, custom castings or forgings. As with any business process, you’ll simply want to analyze what the right balance of automation is for your particular application and budget. Rosler R780 Bowl System with dryer The Rosler Way For more information or to discuss your automation needs and challenges, contact us . With more than 80 years of experience in the surface finishing industry, we are confident that we can deliver a solution for your process. Rosler Tandem R370_12 SE Multi Channel System The complete Automation Series includes: Part 1 – How Robots are Improving Mass Finishing and Shot Blasting Processes. Part 2 – Why Automation is Beneficial for Your Business. Part 3 – What Problems Do You Want to Solve? Part 4 – How Do I Select the Right Machine and Consumables? Part 5 – What Automation Hardware is Available? Part 6 – Environmental Considerations of Automation. Part 7 – The Top 3 Mass Finishing and Shot Blasting Machines. Sign up for enews alerts to be notified of all Rosler blog posts!

Part-on-Part Mass Finishing, Part 2 – Rotary Vibrators Versus Centrifugal Disk Machines

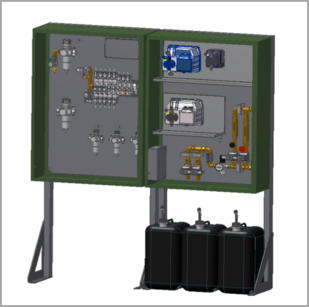
As described in Part 1 of our Part-on-Part Blog Series , some forms of mass finishing techniques encourage part-on-part contact to achieve the desired finish. In addition to viewing work piece impingement as an asset, this type of mass finishing also eliminated the need for ceramic, plastic, and other types of media . The only additives required for such part-on-part finishing are water and the respective compounds . Rosler Metal Finishing designs and manufacturers two machines specifically for part-on-part mass finishing known as WTA rotary vibrators and MK centrifugal disk machines. The applications and benefits of each machine provide a range of part-on-part mass finishing uses for sturdy parts in bulk. Let’s compare their designs. WTA Rotary Vibrators Rosler developed special WTA rotary vibrators especially for part-on-part processing. These machines not only allow running the finishing/washing process, but also the subsequent drying stage in one single machine. The WTA series’ unique, innovative equipment design is a key to finishing success. Design attributes as noted in the diagram include: Rosler WTA rotary vibrator machine design A rotary vibrator at the center of the finishing system with a pneumatic unload gate. An integrated hot air generator which blows hot air onto the finished work pieces in the work bowl. Special dual function drains in the work bowl which use a diaphragm pump to extract process liquid. A suction fan which extracts drying air. A condensation unit which filters drying air. A sophisticated compound dosing system allows for multiple finishing tasks within a single, automated process. Rosler WTA rotary vibrator compound dosing system Rosler WTA rotary vibrator machines allow fully automatic part-on-part cleaning/degreasing , pickling, passivation, and drying of the work pieces in one single machine without any media. https://youtu.be/ZXY1UPoWByY MK Centrifugal Disk Machines In addition to WTA rotary vibrators, Rosler also offers centrifugal disk finishing machines that allow part-on-part cleaning/washing and drying in a single machine. Compared to vibratory equipment, centrifugal disk machines offer the advantage of about 10 times higher processing intensity. However, disk machines should only be used for treating small, sturdy work pieces that will not be damaged (scratched, bent, etc.) by the higher intensity. Rosler MK centrifugal disk machine design As seen in the diagram, the rotating spinner at the bottom and the stationary work bowl of centrifugal disk finishing machine create the centrifugal force and the “vortex” needed to finish work pieces. The centrifugal force of the rotating spinner impels the mass of the parts and compound up the walls of the stationary work bowl. Once the parts have lost their kinetic energy, they collapse back to the center of the spinner. From there, they are accelerated again. The Rosler Way Not sure whether a rotary vibrator or centrifugal disk machine is best for your part-on-part application? We can help! Contact us today to discuss your surface finishing needs. The complete Part-on-Part Series includes: Part 1 – Utilizing Work Pieces as the Media. Part 2 – Rotary Vibrators Versus Centrifugal Disk Machines. Part 3 – Effective Finishing for Ammunition Work Pieces. Sign up for enews alerts to be notified of all Rosler blog posts!

Automotive Crankshafts, Part 2 – Shot Blasting Machines Designed for Crankshafts

As established in Part 1 of our Automotive Blog Series, “Cost-Effective Surface Improvement for Key Engine Components,” shot blasting is an effective technique for the surface treatment of automotive parts including crankshafts. Used in heavy trucks, heavy equipment, and, even, large ships, crankshafts enable an engine to move a vehicle by converting the reciprocating (up/down) movement of the pistons/connecting rods into a rotational movement that propels the vehicle forward. Depending on their size, weight, and production volume, crankshafts can be blast-cleaned in different machines. Rosler Metal Finishing offers solutions for a wide range of crankshaft types with weights from 15 to more than 500 lbs and lengths from 10 up to 80 in and more. Typical Machines Built with specific work pieces in mind, the machines designed to process crankshafts are as diverse as the work pieces they accommodate. RHBE Spinner Hanger Series For somewhat larger work pieces with relatively low production volumes, Rosler’s RHBE spinner hanger machines offer flexible options. Rosler RHBE 17/22 spinner hanger shot blasting machine For example, the RHBE 17/22 spinner hanger shot blast machine with a working envelope of 67 x 86 in allows the individual blast cleaning of crankshafts with lengths of up to 80 in and weights of more than 500 lbs In case of smaller crankshafts, a special work piece fixture permits the simultaneous processing of eight or more components. https://youtu.be/4jMmSm_dz4g Rosler RHBE Overhead Rail Machine RKWS Crankshaft Blast Machine Series In recent years there has been a trend towards specially engineered, dedicated shot blast machines allowing low-cost, efficient blast cleaning of large volumes of small to midsize crankshafts. Rosler RKWS 3 x 4 blast machine Responding to this trend, Rosler has introduced two specially engineered, highly compact shot blasters, the RKWS 2 x 2 and the RKWS 3 x 4. These machines offer cycle times of 20 seconds per part for the RKWS 2 x 2 and 15 seconds per two parts for the RKWS 3 x 4, including work piece loading and unloading by multi-axis robots. Gamma G Turbines The specific turbines used in a shot blasting machine greatly impact its effectiveness and efficiency. That’s why Rosler designed its Gamma 400 G turbines. Rosler Gamma G turbine blade These turbines produce 20 percent higher blast performance and lower energy consumption than conventional blast wheels. With a quick-change system, the Gamma blades minimize downtime caused by blade changes. To minimize wear and the need to purchase new blades, Gamma blades are curved to allow both sides of the blades to be used for added longevity. https://youtu.be/q-NlIOq-iL0 Maintenance demonstration for Gamma 400 G turbine blast machine blades The Rosler Way With more than 80 years of experience, Rosler has the technology and drive to develop a shot blasting application for your automotive crankshaft needs. Contact us to discuss your challenges and needs so we can help you find a better way. The complete Automotive Series includes: Part 1 – Cost-Effective Surface Improvement for Key Engine Components. Part 2 – Shot Blasting Machines Designed for Crankshafts. Part 3 – Typical Mass Finishing Machines Used for Crankshafts. Sign up for enews alerts to be notified of all Rosler blog posts! https://vimeo.com/467660633

Automation, Part 1 – How Robots Are Improving Mass Finishing and Shot Blasting Processes

Automation is changing the way mass finishing and shot blasting processes are delivered. In this seven-part blog series, Rosler Metal Finishing will explain what has given rise to automation trends, the human factors of these manufacturing upgrades, and how such automated processes deliver benefits to your business. Those of us of a certain age remember a portrayal of robotics that, in hindsight, was rather quaint: human-looking automated machines would be crisscrossing our landscape, delivering us food and wardrobe, pumping our gas, collecting our garbage, or – in a more macabre rendering – leading a rise of the machines that would eliminate the human race. Rosler Surf Finisher with automation options In reality, Rosie the Robot and the Terminator have not ruled the world, as predicted by Hollywood. Today, faceless, automated machines, arms, and processors are streamlining the way in which products and services are delivered. In fact, a World Economic Forum article found that the 2020s will be the “age of automation,” with manual jobs making up only 35 percent of the manufacturing labor force by the end of this decade (a drop from 48 percent, as measured in 2016). Additionally, one study expects that more than 1.2 million automated machines will be deployed in industrial situations by 2025 – leading to an increase of automated manufacturing processes to fully 25 percent, from 10 percent today. The relatively low U.S. unemployment rate reinforces the pressure to mechanize. When unemployment is low, the labor force tends to be choosier. As of now, the labor force seems intent on moving toward less physical career choices. Rosler FKS with automation options That said, humans still will have a significant role on the manufacturing floor. Financial analyst Dave McKay noted that automation won’t “kill off your job,” but necessitate new advanced roles in manufacturing that require people who possess skills in critical thinking, complex problem-solving, and monitoring. This offers opportunities for existing employees to pursue a less laborious, and more analytical, career path – things like monitoring, operating, and handling minor maintenance on automated production systems. So, it is clear that mechanization, and partial- or full-automation of our working environment, is here to stay. At Rosler, we, too, are realizing the benefits of automation – developing equipment to support surface treatment technologies including mass finishing and shot blasting . Automated equipment is going a long way toward replacing processes that have had to be done by hand, and also boosting the overall safety, precision, and efficiency of our manufacturing operations. Automation is, simply expressed, a technology, by which a process or procedure is performed with the goal to minimize or completely eliminate human involvement. For mass finishing and shot blasting automation, this means the linkage of two or more finishing stages into a mechanized operation that requires a minimum of operator intervention. Rosler RMBS Today, and into the future, we see this technology evolving, into sophisticated, indispensable surface refinement technologies across many industries including automotive , aerospace , equipment building, medical engineering , power generation, and, even, additive manufacturing . So how will automation promote the factory of the future? How is it beneficial to our business and yours? How do equipment and environmental considerations fit into the paradigm? And what does the future hold? Stay tuned as we explore automation in greater detail in future posts within our Automation Blog Series. Rosler Roboblaster As always, we are eager to learn about your challenges in order to develop and deliver a solution. Contact us today to discuss how we can help you find a better – and perhaps, more automated – way. The complete Automation Series includes: Part 1 – How Robots are Improving Mass Finishing and Shot Blasting Processes. Part 2 – Why Automation is Beneficial for Your Business. Part 3 – What Problems Do You Want to Solve? Part 4 – How Do I Select the Right Machine and Consumables? Part 5 – What Automation Hardware is Available? Part 6 – Environmental Considerations of Automation. Part 7 – The Top 3 Mass Finishing and Shot Blasting Machines. Sign up for enews alerts to be notified of all Rosler blog posts! https://vimeo.com/467660633
Part-on-Part Mass Finishing, Part 1 – Utilizing Work Pieces as the Media

Mass finishing processes require pressure and constant rubbing to achieve the desired finishing results. In most cases, these applications require media specifically selected for its material, size, and shape to act upon work pieces and achieve the required effects. Some mass finishing applications also seek to eliminate or reduce part-on-part impingement or contact to protect delicate and high-value work pieces. Conversely, part-on-part mass finishing intentionally exposes work pieces to impingement and encourages contact between work pieces and the resulting pressure to create finishing effects without the need for ceramic, plastic, and other types of media . The only additives required for such part-on-part finishing are water and the respective compounds . Rosler Metal Finishing designs part-on-part mass finishing machines, known as WTA machines , which help reduce cost per piece through the elimination of media consumption and faster processing times. Ideal Work Pieces Part-on-part finishing is ideal for small, bulk parts that are made of brass, steel, aluminum, and even small ceramic components. Contact pins Pre-conditions for work pieces exposed to part-on-part finishing include: Small sizes, approximately 0.1 to 2” in length or width. Simple, compact shapes. Sturdy nature without a need for delicate handling. Zipper components Part-on-part finishing is commonly used for: Small chain components including rollers and bushings. Small eyelets and hooks. Small stampings such as electrical contacts. Metal buttons. Rivets. Small metal tubing. Zipper parts including sliders and pull tabs. Rollers for small roller and needle bearings. Electrical contact pins. Small spindles and shafts. Ammunition cartridge components including blanks and cups for casings, deep drawn casings, bullets, and primers. Rivets Finishing Processes With the right compound(s) and suitable dosing system, part-on-part finishing machines can handle nearly any type of surface finishing task. Descriptions of finishing tasks and the suggested compound include: Cleaning, degreasing, and de-oiling – In order to remove dirt, grease, or oil from the surface of the work piece, these tasks use pH neutral/slightly alkaline compounds. Pickling – This task utilizes a highly acidic compound to remove oxidation and light scale left over from annealing, brazing, or welding. Deburring and light edge breaking – Breaking and removing sharp edges, such as those left by machining, is achieved with a pH neutral compound. Surface grinding and smoothing – Grinding paste is added to help smooth surfaces. Polishing – To create very smooth surfaces, polishing paste is added. Brightening – pH neutral compounds are utilized to create bright, shiny surfaces. Passivation and corrosion protection – For protection from oxidation and short-term resistance to corrosion, pH neutral and slightly alkaline compounds are effective. Oil compounds are utilized for long-term protection against corrosion. By using several compounds, multiple tasks such as cleaning/degreasing, pickling, and drying or polishing, brightening, passivation, and drying can be combined into a single, fully automatic process. Rosler washing and drying system Operation Benefits In addition to the elimination of media costs and ability to use successive compounds and achieve various processes in a single machine, part-on-part mass finishing benefits include: Compact, space-saving designs since no additional space is required for a separate dryer. Simple material handling due to the elimination of work piece transfer between finishing machine and dryer. Fully automatic operation with suitable work piece loading and unloading equipment. No media issues such as lodging, chipping, or separation because no media is used. Batch operation with complete machine unload, eliminating the risk of parts getting mixed up. Different processing modes for different applications. Flow-through modes open drain valves allowing process liquid to flow straight through the machine. High water level modes close drain valves to retain process liquid in the machine. Use of multiple types of compound in one single process including acidic, pH neutral, and alkaline compounds as well as grinding and polishing paste. Standard Machinery Rosler developed special WTA rotary vibrators especially for part-on-part processing that not only allow running the finishing/washing process, but also the subsequent drying stage in one single machine. Rosler WTA Rotary Vibrator with drying system Besides WTA rotary vibrators, Rosler also offers centrifugal disk finishing machines that allow part-on-part cleaning/washing and drying in a single machine. Both machine types allow the complete unloading of a batch of finished parts to take place either by tilting the work bowl or by activating an unload gate in the bottom of the work bowl. Future posts in the part-on-part mass finishing blog series will compare these machines and their applications. The Rosler Way The experts at Rosler are eager to learn more about your part-on-part mass finishing challenges in order to learn about your needs, develop a solution, and deliver results. We are confident that Rosler can design a process and machine to fit your needs and supply the most appropriate compound for your process. Contact us today to discuss your needs. The complete Part-on-Part Series includes: Part 1 – Utilizing Work Pieces as the Media. Part 2 – Rotary Vibrators Versus Centrifugal Disk Machines. Part 3 – Effective Finishing for Ammunition Work Pieces. Sign up for enews alerts to be notified of all Rosler blog posts!
Automotive Crankshafts, Part 1 – Cost-Effective Surface Improvement for Key Engine Components

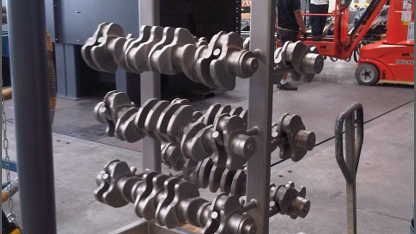
Crankshafts are a key component of internal combustion engines, be it mass-produced engines for motorcycles and automobiles , engines for heavy trucks, off-high highway equipment, and even large ships. Crankshafts convert the reciprocating (up/down) movement of the pistons/connecting rods into a rotational movement that drives the wheels and allows a vehicle to move forward. Rosler Metal Finishing understands the vital importance of these engine components and has developed specific shot blasting and mass finishing machines to process these pieces to perfection. A crankshaft with connected rods and pistons Materials & Production Methods Considering that automotive crankshafts weigh around 40-60 pounds and rotate approximately 100 times per second, these parts are exposed to tremendous tensile, compressive, and shear stresses. In addition, combustion forces and piston acceleration in an engine can also cause significant vibration. Therefore, crankshafts must be made from tough, wear-resistant materials, usually high alloy carbon steel. Typical alloying elements are manganese, chromium, molybdenum, nickel, cobalt, or vanadium. The most common materials are AISI/SAE 4340, EN-30B, 4330-M, 32-CrMoV-13, or 300-M. Crankshafts are made by: Casting – The production of cast iron crankshafts is limited to cheaper production engines, for example, low-performance diesel engines with lower overall loads. Hot forging – Today the most common manufacturing method is hot forging at temperatures of 1,700 to 2,100° F. Compared to casting, forged cranks offer a higher strength with – at the same time – lower weights and somewhat more compact dimensions. Depending on the utilized steel alloy, forged crankshafts may have to undergo a heat treatment process in the form of tempering and quenching. This is generally done after forging, but sometimes also after machining. Complete machining from a steel billet – This method is quite costly and is predominantly used for motorsport and high-performance applications, never for high-volume engine production. A hot-forged crankshaft After forging or casting, crankshafts must undergo an intensive machining process that includes: Turning of the journals, sometimes also called crankpins. Drilling of the oil holes in the journals. Drilling of the balancing holes in the counterweights. Milling of the drive sprockets, etc. Surface Treatment Tasks The main surface cleaning/treatment tasks for crankshafts include: Blast cleaning after forging or casting. Shot peening after machining. Deburring after machining. Blast cleaning after forging or casting is required because the forging/casting/heat treatment process leaves a relatively strong layer of scale on crankshafts and other work pieces. Prior to subsequent production processes such as machining and micro finishing, the work pieces must undergo a blast cleaning process to create a surface finish of SA 3, i.e. a pure white metal surface without any scale residues whatsoever. Crankshafts before and after blast cleaning The high compressive, shearing, and tensile stresses that crankshafts are exposed to as a result of machining can be relieved significantly by shot peening. In this application, the peening process focuses on the journals, especially the bearing surfaces as well as the journal fillets and journal cheeks (counterweights). Crankshaft peening is usually done by air blasting with relatively fine steel media. Deburring after machining is required to smooth edges including those of counterweight cheeks, drilled balancing holes in the counterweights, milled drive sprockets, and, sometimes, drilled oil holes in the journals. It is extremely important that the bearing areas on the journals are not damaged. The deburring operation is frequently done by mass finishing. Crankshaft machining The Rosler Way Whatever type of engine your crankshafts are designed for, Rosler can develop equipment and a process to provide accurate and repeatable finishing results. We are proud to lend our surface finishing expertise to the automotive industry. Contact us today to discuss your unique challenges. The complete Automotive Series includes: Part 1 – Cost-Effective Surface Improvement for Key Engine Components. Part 2 – Shot Blasting Machines Designed for Crankshafts. Part 3 – Typical Mass Finishing Machines Used for Crankshafts. Sign up for enews alerts to be notified of all Rosler blog posts!
Manufacturing Industry Outlook

At Rosler Metal Finishing , we believe in helping our clients in many industries find a better way to finish and process their products. Part of our success comes from understanding their industry, their process requirements, and market drivers. Our friends at IndustryWeek are making our jobs easier when it comes to understanding market drivers. The top findings from their recent research The Future of Manufacturing: 2020 and Beyond include: Positive outlook for growth and sales Leaders are overwhelmingly positive about their business growth prospects. Nine out of 10 expect revenues to increase and more than half (58%) anticipate strong growth of 5% or higher per year over the next five years. More than two thirds (70%) of manufacturers expect to increase the number of people that they employ over the next five years. Fulfillment strategies shift towards build-to-order Over the next five years, manufacturers will continue to move away from make-to-stock and shift towards less inventory dependent build-to-configure and engineer-to-order fulfillment strategies. This shift will cause processes and company strategy to focus on agility. Companies will be required to quickly shift attention and resources to mitigate risks and fully capitalize on growth opportunities. Increased productivity tops manufacturers’ investment list Companies will invest billions of dollars in a wide range of technologies during 2020. Decisions on where to invest will depend on leadership priorities and objectives. Predictably, whether driven by new technology or process improvements, productivity tops the list. The top 5 new technology investment priorities include: Higher productivity Faster responsiveness to customer orders and requests Enhanced collaboration with customers and suppliers Enhanced market intelligence More effective customer communication Market Volatility and rising material costs threaten growth he top challenges to meeting these strong growth expectations are market volatility, rising material costs, price reduction pressures, and increasing labor costs. To thwart such threats, according to Industry Week research, manufacturers are pushing hard to improve performance across a range of capabilities, starting with improving production processes, strengthening customer relationships and finding people with the right skills and experience. Rosler is your Secret Weapon With continued growth predicted across industrial sectors and a focus on improved process and productivity, Rosler is your secret weapon. The Rosler Group has been the experts in the field of surface finishing for more than 80 years and offers the most extensive portfolio in the world of mass finishing systems, shot blasting, consumables and services. The job of our specialists is to design a system for your finishing process, or a complete production line. We will provide support throughout your machine’s lifetime; from the planning phase, all the way to after-sales support and service. Our technology management team works with you to develop the perfect finishing process, precisely tailored to your work pieces. https://youtu.be/E7OQkfEXc8Y At Rosler, finding a better way is our goal. The Rosler Way True to our motto of “finding a better way…” Rosler considers all inputs and outputs of your process. We offer experienced finishing engineering and an entire range of surface finishing equipment and consumables (media and compound) to ensure that the entire process is optimized. Whatever your surface finishing needs are, you can count on Rosler Metal Finishing to find a better way. Contact us today to start the conversation.

Mass Finishing – Are You Ready to Meet Customer Demand in 2020?

Updating a process to meet increased production demand is a cost-effective way to not only improve your processing times and results, but also increase and prolong your equipment’s usefulness. Let’s say production has been steadily building over time. How do you know if it’s time to evaluate the process for improvement? Mass finishing experts suggest examining the final finish accomplished by the process and its ceramic or plastic media and compound usage. Processes in need of optimization will not achieve the desired finish in an acceptable timeframe and will use more media and compounds than necessary. Increasing production demands without reconsidering the process can trigger finishing issues and lead to extra processing time and expense as well as rejected components. As more parts are processed, media begins to wear more quickly. As the media to component ratio decreases, part-on-part impingement is likely to occur and damage surfaces. In these cases, a more aggressive media with a higher cutting ability may solve the problem by producing the desired finish in a shorter cycle time. By lowering cycle times, the required media to component ratio can be achieved eliminating part-on-part contact and ineffective deburring. A process-oriented, experienced manufacturer such as Rosler can help you evaluate your current media type, workpiece properties, process time, and results to suggest an alternative media for optimized performance. Reactive Problem Solving Not all finishing problems are a result of increased production. An increase in processing time and scrap parts, poor finish, using too much water, and creating too much foam can also signal processing issues brought on by other known or unknown causes. If you’re not getting the desired finish on your components, reviewing the mechanics of the machine should be your first step. Meeting with a Client to Discuss a Process, Consumables, and Improvements Mass finishing experts suggest reviewing the machine to answer the following questions: Are the drains clogged? Has the movement of mass in the machine changed? Is the water/compound mix flowing properly? Are there bad valves or plugged compound valves? Is the liner intact or is a tear creating a dead spot where media is trapped? If the machine itself and its mechanics check out, the process should be examined carefully to identify an area in need of optimization. Process-related concerns include media that has glazed over and the presence of excess foam in the machine and/or too much water trapped by clogged drains. Evaluating mechanical and process efficiencies will not only help identify process problems, but also reduce processing costs. For example, maintaining the correct compound usage will reduce unnecessary consumption and ensure that components are processed more efficiently and with fewer rejects. A Learning Experience Mass finishing is an art and a science. No one knows that better than Rosler. When you lose track of that balance, mistakes are bound to happen. Whatever your process optimization needs are, you can count on Rosler Metal Finishing to find a better way. Contact us today to start the conversation.

A Year in Review – Top Blog Posts from 2019

At Rosler, we believe in helping our clients in unique markets find a better way to finish and process their products. According to Grand View Research, Inc., the global structural steel market is expected to reach USD 140.4 billion by 2025. It is projected to expand at a CAGR of 5.6% during the forecast period. Increasing construction spending in emerging economies is projected to drive the demand for structural steel. Maybe that’s why our top posts this year included a series on Structural Steel. Enjoy the following recap. 5. Optimal Media Mix, Part 1 – Identifying and Maintaining Proper Levels The best mass finishing equipment is useless without the proper media. That’s why the experienced engineers at Rosler Metal Finishing pair their quality equipment with the right type and amount of media to achieve consistent results. Media comes in all kinds of shapes and sizes Understanding how your machine, the work pieces it is finishing, and the selected media will interact is key to delivering an optimal finish each cycle. Doing so requires understanding why media levels are important, determining and tracking levels, and evaluating media consumption to avoid issues. Read more about identifying and maintaining proper levels with your media levels. 4. Structural Steel FAQ, Part 7 – Comparing Commonly Used Blast Machines Steel construction and steel trade , shipyards and ship building , and heavy equipment and machinery building rely heavily on specially designed shot blasting machines to prepare their components. Rosler Metal Finishing expertly designs shot blasting machines for these industries and others to descale, clean, and prepare structural steel for surfaces for end-use. The particulars of each machine largely depend on the size and shape of the specific components in need of preparation. This installment of our Structural Steel FAQ series answered: What are the most commonly used blast machines for structural steel surface preparation and how do they compare? Learn more about the commonly used blast machines for structural steel surfaces. 3. Structural Steel FAQ, Part 4 – Evaluating the Presence of Dust As an expert in the surface finishing industry, Rosler Metal Finishing knows that all the expertise in the world won’t do any good if the surface of the work piece is not properly prepared. When it comes to structural steel, we receive many frequently asked questions about preparation. This installment of our Structural Steel FAQ series answered: How is the presence of dust on shot blasted structural steel components evaluated? Learn more about how to evaluate the presence of dust. 2. Using Vibrascope to Measure Amplitude V. Frequency in Vibratory Bowls Example of vibratory drive When it comes to mass finishing, amplitude and frequency require balance and careful consideration. Amplitude is a measure of movement and intensity while frequency refers to the rate of repetition. The wrong amplitude, for example, if it’s too low, can create a lackluster finishing results and longer processing times. If too high it can cause unnecessary wear and tear on the machine. Read more on using vibrascope to measure amplitude v. frequency in vibratory bowls. 1. Structural Steel FAQ, Part 3 – Evaluating Rust and Mill Scale Pre- and Post-Blast Surface preparation can account for up to 40 percent of structural steel painting and repainting jobs. As Rosler Metal Finishing’s Structural Steel FAQ series has already established, the life of anti‐corrosion coatings on a steel surface depends to a large extent on how thoroughly this surface has been prepared for painting. Application of anti-corrosion paint in a preservation line blasting system Properly evaluating the surface of structural steel surfaces for coating before and after shot blasting will help balance the cost of preparing, repairing, and monitoring structural steel throughout its impressive lifespan. This installment of our Structural Steel FAQ series answered: How are rust and mill scale evaluated pre ‐ and post ‐ blast? Learn more about how rust and mill scale are evaluated pre- and post-blast. The Rosler Way True to our motto of “finding a better way…” Rosler considers all inputs and outputs of your process. We offer experienced finishing engineering and an entire range of surface finishing equipment and consumables (media and compound) to ensure that the entire process is optimized. Whatever your surface finishing needs are, you can count on Rosler Metal Finishing to find a better way. Contact us today to start the conversation.