Solution Finder
SOLUTION FINDER

Uw gids door de Rösler productwereld

Met een paar klikken vindt u de juiste machine voor uw behoeften!

Resultaten: 235 Artikel
Simulation der Staubbelastung

Besser, schneller, wirtschaftlicher durch Simulationstechnik

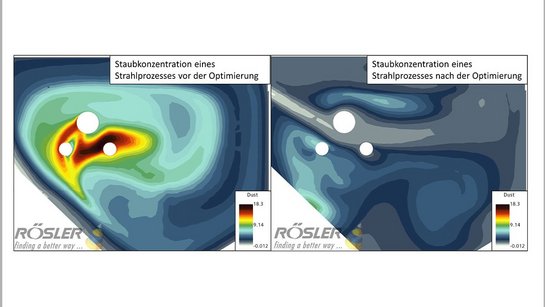
Die Bedeutung der OberflĂ€chenbearbeitung wĂ€chst in zahlreichen Industriebereichen. Die Forderung dabei lautet: Definierte QualitĂ€tsanforderungen in kurzen Prozesszeiten bei geringstmöglichen Kosten ressourcenschonend erzielen. Diesem Anspruch wird Rösler unter anderem durch den Einsatz von Simulationssoftware bei der Konstruktion von Strahl- und Gleitschliffanlagen sowie der Prozessauslegung und -optimierung gerecht. Zeit- und kostenaufwendige Versuchsreihen im Customer Experience Center können durch den Einsatz der Software reduziert werden, Anlagen und Prozesse stehen schneller und mit grĂ¶ĂŸtmöglichem Kundennutzen zur VerfĂŒgung. Optimale Strahlergebnisse in kĂŒrzerer Zeit mit weniger Strahlmittel und effektiverem Lufthaushalt Der multiphysikalische Ansatz dieser modernen Simulationslösung ermöglicht anspruchsvolle Strahlprozesse anhand von 3D-Daten zu simulieren und optimal auszulegen. In die Simulation fließen alle prozessrelevanten physikalischen Randbedingungen ein. So lĂ€sst sich Strahlmittel virtuell auf beliebige WerkstĂŒcke applizieren, die sich wie bei der spĂ€teren, realen Bearbeitung bewegen. Die korrekte Darstellung der Strahlbilder und der Strahlmittel-Massenströme erlaubt dabei eine zuverlĂ€ssige Auswertung und Anpassung des Trefferbilds und der Strahlleistung auf dem Bauteil. Der daraus resultierende, effektivere Strahlprozess sorgt dafĂŒr, dass geforderte Strahlergebnisse effizienter erzielt werden. Gleichzeitig verringert die gezieltere Applikation des Strahlmittels auf das Bauteil Verschleißerscheinungen innerhalb der Strahlkammer, wodurch Maschinenstillstandszeiten sowie Instandhaltungskosten deutlich reduziert werden. Ein weiterer Aspekt, der bei der Simulation betrachtet wird, ist die Staubbelastung in der Strahlanlage. Auf dieser Basis lassen sich konstruktive Maßnahmen fĂŒr eine bessere Absaugung von Staubfrachten sicher und einfach definieren, sodass eine mögliche Staubexposition im Umfeld der Strahlanlage erheblich vermindert werden kann – und das auch bei bestehenden Anlagen, unabhĂ€ngig vom Hersteller. Schnell zu idealen Gleitschliffprozessen fĂŒr komplexe WerkstĂŒcke Die Entwicklung von Gleitschliffprozessen fĂŒr geometrisch komplexe Bauteile, wie beispielsweise Knieimplantate, erforderten bisher aufwendige Versuchsreihen. Bei diesen Anwendungen bietet die Simulationstechnik ebenfalls entscheidende QualitĂ€ts-, Zeit- und Kostenvorteile. Durch die Darstellung der Schleifkörperbewegung, wobei Schleifkörper in beliebigen Geometrien abgebildet werden können, und der effektiven Schleifwirkung auf dem Bauteil, lĂ€sst sich die ideale Kombination von Schleifkörper und Maschinenparametern ermitteln. In die Partikelsimulation kann darĂŒber hinaus der Verschleiß der Anlage analysiert werden. Ein weiterer Vorteil der Simulation im Vergleich zu realen Versuchsreihen ist die Untersuchung von noch nicht gefertigten Bauteilen oder Systemen aller Art anhand von CAD Daten.

Mass Finishing Work Piece Handling Series, Part 2 – Preventing Drop Height Damage

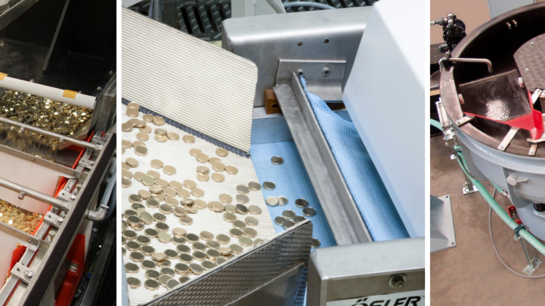
Ensuring drop heights are not too high when raw work pieces are loaded into and exiting a mass finishing machine is an important consideration. Rosler has extensive experience developing mass finishing machines as well as material handling accessories to create a productive and efficient surface finishing system and prevent drop height damage. When evaluating drop heights and machine configuration needs, it is recommended that you consult an experienced equipment provider to help review key machine aspects and suggest solutions tailored to your unique needs. Issues to Avoid Falling from a loading container into a machine as well as moving from the machine into a post-process collection can cause damage to work pieces in the form of nicking and scratching caused by contact among work pieces as well as with the machine itself. More delicate and/or sharp work pieces, therefore, require extra consideration and evaluation of drop heights than sturdy and rounded components. For example, components with critical sealing areas, parts requiring a tight fit, and parts that need a high gloss polish must be handled with extra care. If big height distances must be overcome, chutes should be employed allowing the work pieces to gently slide down instead of just being dumped on top of each other, essentially “de-sharpening” the effect of contact. Similar caution must be employed at the various transfer points within a mass finishing system, for example, the transfer of the finished work pieces from the finishing unit to the separation station or from the finishing machine to a dryer, collection table, etc. The prevention of high drop heights should be one of the key questions for a supplier when considering the purchase of a new mass finishing system or modifying an existing system. Rosler offers a variety of transfer sections and attributes, including (from left) separation systems for coin blanks, separation screens to dryer to prevent part-on-part damage with gentle drop heights, and separation system with linear drive for extra gentle transport of parts. Media Considerations In addition to issues with work pieces, excessive drop heights can also cause issues with media . For example, unusual splintering or chipping of ceramic media may occur at transfer points if drop heights are too high or media is returned to the machine too quickly when external media separation is utilized, such as with inline trough machines . Media return conveyor of an inline trough machine. Media may also be prone to fracturing if heavy parts are dropped into the machine too aggressively. These media chips and fragments can lodge in the work pieces and cause problems in downstream processes or when the product is in use. Working with your equipment supplier is key to ensure that all transfer points in a finishing system allow a gentle media transfer as well as work piece transfer. The Rosler Way Our team of experts can help design, service, and calibrate a mass finishing system for your unique needs. Contact us to discuss your mass finishing and work piece handling needs. The complete Mass Finishing Work Piece Series includes: Part 1 – Selecting the Best Work Piece/Media Separation Method . Part 2 – Preventing Drop Height Damage . Part 3 – Maintaining Wear Linings .
19 Auszubildende und Duale Studenten

Die „Rösler-Familie“ freut sich ĂŒber 19 NeuzugĂ€nge

Die Rösler OberflĂ€chentechnik GmbH bleibt in der Region einer der wichtigsten Partner beim Thema Ausbildung: 14 junge SchulabgĂ€nger beginnen zum 1. September eine Lehre in einem technisch-gewerblichen oder kaufmĂ€nnischen Beruf in Memmelsdorf und Hausen. Dazu kommen fĂŒnf Studenten, die bei Rösler den praktischen Teil ihres dualen Studiums absolvieren. Mit der Zahl der abgeschlossenen AusbildungsvertrĂ€ge ist Anja SĂŒppel, Abteilungsleiterin fĂŒr den Bereich Ausbildung bei Rösler, durchaus zufrieden. Doch auch bei dem familiengefĂŒhrten Industrieunternehmen wird es zunehmend schwieriger, die Stellen zu besetzen. "Der heutige Tag ist fĂŒr uns alle immer wieder etwas ganz Besonderes", so Anja SĂŒppel, Abteilungsleiterin fĂŒr den Bereich Ausbildung bei Rösler. "Wir sind uns bewusst, was fĂŒr eine Bedeutung der Tag fĂŒr unsere jungen Berufsstarter hat. Deshalb wollen wir ihn so positiv wie möglich gestalten. Wir fĂŒllen diesen Tag mit viel Information und Wissen, aber auch mit der Möglichkeit, sich kennenzulernen. Sollten die jungen Leute Ängste oder Bedenken haben, dann versuchen wir ihnen diese zu nehmen. Damit sie mit viel Freude ins Berufsleben starten können." Doch nicht nur der erste Tag soll etwas Besonderes sein fĂŒr die jungen BerufsanfĂ€nger bei Rösler. In der zweiten Woche stehen die „Projekttage“ an, bei denen die Neu-Azubis ihren Ausbildungsbetrieb und die Unternehmenskultur intensiv kennenlernen dĂŒrfen. Das große Finale ist am Freitag der Outdoor-Tag auf dem CVJM-GelĂ€nde in Altenstein. Zusammen mit einer Trainerin lernen sich die Auszubildenden dort als Gruppe kennen. „Sie erfahren, dass keiner allein ist und dass wir als Unternehmen eine tragfĂ€hige Gemeinschaft sind. Das ist dann der Tag, an dem spĂ€testens die Handynummern ausgetauscht und erste Verabredungen getroffen werden,“ so Anja SĂŒppel. „Viele Azubis erinnern sich noch Jahre spĂ€ter daran zurĂŒck, und fĂŒr uns als Ausbilder ist es immer wieder schön zu sehen, wenn aus vielen Einzelnen ein Team wird.“ Zufriedene Auszubildende sind die beste Werbung Ein hohes Engagement und viel WertschĂ€tzung fĂŒr die Azubis sind bei dem MittelstĂ€ndler selbstverstĂ€ndlich. Denn zufriedene Auszubildende sind fĂŒr das Unternehmen auch eine wichtige Werbung. Auf diese Werbung kann ein Unternehmen wie Rösler heute nicht mehr verzichten, da die Zahl der Bewerber seit Jahren rĂŒcklĂ€ufig ist. Besonders im Bereich Produktion. In einem dieser schwierigen Bereiche geht das Unternehmen jetzt dennoch in die Offensive. Geplant ist, in einem Pilotprojekt ein- bis zwei Bewerber im neu geschaffenen Ausbildungsberuf „Maschinen- und AnlagenfĂŒhrer“ auszubilden. Dabei sollen neue Zielgruppen angesprochen werden, neben BerufsanfĂ€ngern etwa auch ungelernte ArbeitskrĂ€fte aus dem eigenen Unternehmen oder von extern, die ihr praktisches Wissen spezifizieren und einen Berufsabschluss erwerben wollen. Die Ausbildung soll in der Abteilung Compoundfertigung angesiedelt werden. „Wir sehen es als gute Chance, Fachpersonal fĂŒr die Produktionsbereiche selbst auszubilden. Gerade weil wir die richtigen Infrastrukturen dafĂŒr haben: Produktionsanlagen, engagierte Ausbilder und eigene AusbildungswerkstĂ€tten,“ unterstreicht Anja SĂŒppel. Die Suche nach geeigneten Auszubildenden fĂŒr Herbst 2023 hat bereits begonnen. FĂŒr die jungen SchulabgĂ€nger bietet der Ausbildungsmarkt dann erneut enorme Möglichkeiten. Das Rösler-Ausbildungsteam freut sich auf viele Bewerbungen. Die Rösler-Gruppe sucht fĂŒr das Jahr 2023 folgende Auszubildende: Industriekaufleute, Chemielaboranten, Technische Produktdesigner, Konstruktions-mechaniker, Industriemechaniker, Mechatroniker, Elektroniker fĂŒr Betriebstechnik, FachkrĂ€fte fĂŒr Lagerlogistik, Maschinen- und AnlagenfĂŒhrer und Fachinformatiker. Ein dualer Studiengang ist möglich im Bereich Wirtschaftsingenieurwesen oder Elektrotechnik. Die Partnerhochschule von Rösler ist die Duale Hochschule in Mosbach. Online-Bewerbungen sind ab sofort möglich ĂŒber die Internetseite: www.rosler.com Bei Fragen zu Ausbildung/Dualem Studium gibt Anja SĂŒppel gerne Infos unter Tel.: +49 9533 / 924-442 oder per E-Mail an: a.sueppel@rosler.com

Comprehensive Mass Finishing System Provides ‘Shear’ Results for Gardena

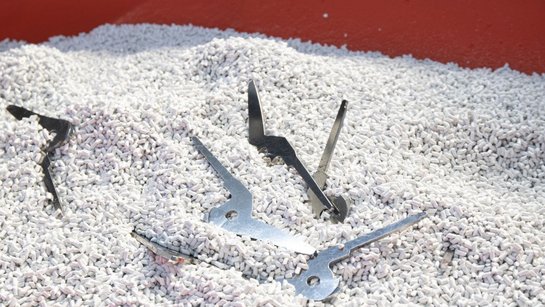
Improved productivity, increased production capacity, better quality, and lower costs—a leading garden tool manufacturer tasked Rosler with developing a new mass finishing system to improve the deburring and polishing of garden shear knives. Rosler provided a solution in the form of a tailor-made Keramo-Finish ¼ process carried out within a double-batch centrifugal disc finishing machine. Known as the FKS 35.1 A2-So , the system includes fully automatic work piece handling and a two-stage process that deburrs and polishes stamped and laser-cut knives. Work pieces are subsequently dried in an energy-efficient rotary dryer and prepared for the next manufacturing step. The Situation For more than 60 years, the Gardena division of Husqvarna Group has developed a variety of gardening products and tools. The company’s broad product range includes innovative systems for irrigation, soil cultivation, and lawn, tree, and shrub care. Gardena products are used in more than 80 countries worldwide. To ensure easy and simple handling, produce excellent cutting performance, and guarantee long service life, the Gardena’s shear components are produced with state-of-the-art manufacturing technologies. Stamping or laser cutting of the upper and lower knives followed by surface finishing is an important step. Gardena shear components in a Rosler mass finishing machine Previously, the lower knives required two separate finishing operations: one in a rotary vibrator and one in a centrifugal disc finishing machine . Since Rosler originally provided systems for the two separate operations, Gardena trusted Rosler to develop a combined solution with upgraded manufacturing capabilities and increased automation. In streamlining the mass finishing process, Gardena sought to optimize its process, improve productivity, increase capacity, and reduce operating costs. The Solution Keeping subsequent manufacturing steps in mind, engineers ran a series of trials with various processing media and different parameters in one of Rosler’s Customer Experience Centers . Gardena Keramo-Finish¼ process in use A Keramo-Finish ¼ process in a centrifugal disc finishing machine produced the best results. The specific process includes the use of a ceramic media with minimal abrasive characteristics in combination with a grinding and polishing paste and a cleaning compound with a distinct brightening effect. Most importantly, the new process allows the deburring and polishing of all knives with a single machine. The rotary vibrator was no longer required, and the work piece handling was simplified. Moreover, depending on the work piece type, the new Keramo-Finish ¼ process has reduced processing times significantly and now allows for bigger work piece batches. These improvements have helped reduce operational costs by approximately 10% while delivering improved finishing results. The Process The new double batch centrifugal disc finishing machine was perfectly integrated into the manufacturing flow at Gardena. Work piece specific processing programs stored in a PLC controller allow targeted finishing of the various knife types. After stamping and laser cutting, the work pieces are collected in perforated metal bins. An operator utilizes a swing crane to dump the raw knife components into a loading device that transfers them into a vibratory feed hopper. Once the respective finishing program has been manually selected, the hopper automatically feeds a work piece batch into the work bowl for processing. Following the preset finishing time, the work bowl gently dumps the mix of finished work pieces and media onto a vibratory hopper. The mix then passes through a vibratory separation unit where a screen separates work pieces from media. The media mix itself is further screened to discharge undersized media that is no longer suitable for the finishing process and guarantee a continuous high process stability. Gardena rotary dryer with direct heating While usable media is returned to the work bowl, the finished knife blanks are transferred to a drying station filled with a maize-cellulose product. The rotary dryer RT 550 Euro-DH is equipped with an innovative new direct heating system that guarantees not only fast, reliable, and spot-free drying of the work pieces but also produces energy savings of up to 40% compared to conventional rotary dryers. After completion of the drying cycle, knives are transferred to another vibratory hopper that loads them into small transport carriers made from plastic. A fully automatic Z 1000 centrifuge cleans the process water for re-use in the finishing process. This recycling helps save valuable resources by drastically reducing water consumption and promoting sustainable and efficient operation of the new mass finishing system. Automated Advantages The automated aspects of Gardena’s new system went beyond improved efficiency and capabilities to provide an additional advantage in the reduced need for manual labor. Like many employers, Gardena has faced increasing competition for manpower. The use of work piece handling systems, conveyor belts, and robots have helped bridge the gap in human resources and maintain production rates. Additionally, in the world of manufacturing, this mitigation of human intervention offers even greater and more measurable efficiencies. The Rosler Way Decades of experience and ability to design, service, and maintain machines as well as the consumables and accessories to get the finish you require make Rosler a well-rounded surface finishing expert. Contact us to discuss your mass finishing needs.
advanced version of the digital process water management system

Rösler Smart Solutions: Advanced version of the digital process water management

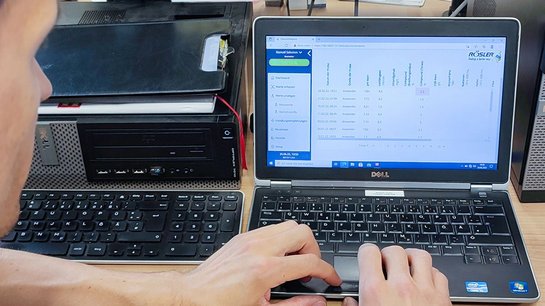
Sustainable and cost-efficient surface finishing of balancing weights Today centrifuges are the most commonly used systems for cleaning and recycling the process water required in mass finishing operations. For example, the globally leading supplier of balancing weights, Wegmann Automotive, is utilizing a fully automatic Rösler centrifuge, model Z1000. As a pilot customer Wegmann expanded the software for its centrifuge with the “advanced version” of the innovative digital process water management system from Rösler Smart Solutions. Compared to the previously practiced manual process control the new software package with its digital algorithms has produced considerable benefits. It helped not only to improve the overall product quality but also resulted in substantial cost savings. When it was founded in 1882, the company initially was building carriages. From these modest beginnings Wegmann expanded into a corporate entity with three different business units. In their respective fields all three units are global market and technology leaders. The Krauss-Maffei Wegmann GmbH & Co. KG develops and produces a wide range of products in the field of national defense. The Schleifring GmbH is a leading provider of systems for the transfer of energy, electrical signals, data and electronic media. With a huge portfolio of balancing weights, tire valves, battery terminals, tire pressure control systems, including suitable service kits and special weights, the Wegmann Automotive GmbH supplies not only numerous automobile manufacturers but also serves the entire automotive aftermarket. The company, located in Veitshöchheim, Germany, produces more than one billion components per year. As global leader for balancing weights Wegmann Automotive produces percussion and adhesive weights for steel and aluminum wheels. A mass finishing operation that must meet stringent demands The balancing weights are made as stampings from steel and galvanized steel as well as die-castings from zinc or zinc alloys. Eugen Weizel, the department manager for mass finishing and coating at the Wegmann Automotive company, explains: „After the stamping or die-casting process the weights undergo a part-on-part mass finishing operation in a rotary vibrator. The goal is to completely remove the residual oil left over from the stamping process and the water-based mold release agent left over from the die-casting operation. At the same time the utilized compound provides a corrosion protection for the steel parts. On the other hand, the zinc die-castings require a certain surface tension for the subsequent coating step. The surface tension is carefully monitored and controlled.” Mr. Weizel’s colleague Manuel Salomon, as WAPS (short for Wegmann Automotive Production Systems) responsible for setups in the coating department, trainings and Lean Management, adds: “A high compound concentration in the process water is beneficial for the corrosion protection on the steel parts. But if it is too high, we will not achieve the required surface tension on the zinc components. This can cause inadequate coating results and may even force us to scrap some products.” The product quality depends on the quality of the process water Since the process water is recycled, the process water cleaning operation with a fully automatic Z1000 centrifuge from Rösler and the control of the compound concentration are key factors that determine the quality of the balancing weights. Manuel Salomon continues: „When the mass finishing machine and the centrifuge were commissioned, we quickly recognized that there is a close correlation between the process water quality and the quality of our products. Therefore, we carefully measured the compound concentration once per week and recorded the measured results. This allowed us to precisely define the compound concentration for our finishing process and correct it as needed.” Since measuring and recording the concentration values was quite time consuming, Wegmann gladly accepted Rösler’s offer to utilize the advanced version of the “digital process water management system” as a pilot user. Eugen Weizel concludes: „We quickly recognized the benefit to further develop and refine the software package together with Rösler, and, at the same time, to deepen our process knowledge.” The new, interactive monitoring and control system for process water cleaning and recycling with semi- and fully automatic centrifuges is integrated into the centrifuge controls and allows the monitoring, recording and evaluation of all relevant process parameters. At Wegmann this includes measuring the compound concentration by titration or refraction (BRIX), the pH value, the process water conductivity, the water hardness, the microbiological contamination with bacteria, yeast and fungi, chloride contents, CSB value (chemical oxygen demand) and BIT concentration (biocide in the process water. The system also monitors the appearance and the smell of the process liquid. The process water parameters to be monitored can be individually selected and their values adapted to the respective finishing requirements. In the basic version of the digital process water management system from Rösler Smart Solutions the samples are taken manually and analyzed with suitable measuring devices that can also be supplied by Rösler. After the data have been entered into the system, the algorithm in the software determines if the measured values are within the specified limits. In case of deviations the dashboard displays suitable actions, which can be immediately implemented. In addition, the technical background and corrective actions are explained in detail. This allows the operator to undertake the measures required to bring back the values into the acceptable range and to secure the desired process stability. Since all parameters are stored in the system, they can be retrieved at any time, for example, in the form of a table or a chart. The latter helps to prevent unwanted and costly downtimes by carrying out necessary process water changes during periods, when they are not interfering with the manufacturing operations. The complete documentation of the operational parameters is also a valuable tool to prove the process quality and process stability during quality audits as well as for validation purposes. Recommended actions can also be called up in case of events that affect the overall quality of the mass finishing process. This includes foaming during the process, corrosion of the work pieces or insufficient work piece cleanliness that could negatively affect subsequent manufacturing steps. Manuel Salomon comments: „The pointers and recommended actions are extremely helpful. In the past we measured the process parameters. But when it came to the necessary corrections, we were entirely on our own. And in case of process problems we had to search for solutions ourselves, or we had to ask for help by telephone. Today the digital system provides all the support we need. This is especially helpful for colleagues with little knowledge of mass finishing and process water cleaning and recycling.” A simple solution that can be quickly implemented The smart process water management system has been in operation at Wegmann Automotive since the middle of March this year. Eugen Weizel remarks: „The software structure is well organized and easily understandable. And the system can be fully utilized after a short training. All critical data are arranged so that they can be viewed at a glance. And the entire information is presented in an easy-to-understand manner.” While in the past the compound concentration was only measured once per week, now it is measured twice, once in the morning and once in the afternoon of a particular day. In addition, the pH value is recorded, and the appearance and smell of the process water is monitored. „This approach provides us with valuable information about our process. For example, the development of the compound concentration tells us that due to a higher volume of oily work pieces we must increase the compound dosing rate to maintain the required process water quality,” explains Manuel Salomon, who continues: „Another example is the microbiological contamination. In the past we did not control this at all. If the contamination is too high, it can have an adverse effect on the corrosion protection of steel parts.” Significantly improved process stability and cost-efficiency For monitoring the various parameters with the digital process water management system Wegmann Automotive needs about 20 minutes per week. Compared to the once-per-week measurement of the compound concentration this requires about 15 minutes more. But the technical and economic benefits achieved by the digital system are so significant that the company gladly accepts the fact that a bit more time must be invested. Eugen Weizel concludes: „With the digital process water management system we find out quickly, if for example, the compound concentration is no longer adequate. Since this could have an adverse effect for subsequent manufacturing steps, we are grateful to have such a valuable, early warning system. Our finishing process is now not only a lot more stable but also more economical.” Therefore, it is not surprising that the company is interested in the next version of the digital process water management system from Rösler Smart Solutions. This allows the automatic measurement, evaluation and recording of the process parameters.
Foundry-Specific Shot Blasting Achieves Increased Efficiency

Replacing a shot blasting machine for a long-time customer requires finding a better way to deliver efficient finishing in a faster, smaller, and more maintenance-friendly way. That’s exactly what Rosler delivered when Linde Material Handling (Linde) returned to us for a shot blasting upgrade. Linde is a supplier of forklift trucks and warehouse equipment and also provides technical intralogistics solutions and services. With a sales and service network spanning more than 100 countries, the company has a global footprint. For this particular partnership, Linde’s foundry in Weilbach, Germany, challenged Rosler to supply a new shot blasting system capable of finishing and maneuvering the counterweights it manufactures for forklifts. Our solution was a sturdy foundry version of a continuous hanger shot blast machine known as the RHBD 22/27-F. The Situation Linde continuously strives to improve its manufacturing operations. As such, the new machines had to accomplish several goals, including faster processing, more flexible material flow, optimized utilization of available space, improved access to all critical maintenance areas, and increased overall efficiency. Working closely with the Linde project team, Rosler identified ways to optimize the material flow and increase overall flexibility within the shot blasting technology utilized. To fulfill the demand for better utilization of space, these technology enhancements were built into a customized version of the RHBD continuous feed spinner hanger blast machine. The Solution The newly created machine is setting new standards for surface finishing in the foundry industry, and its fully automatic and flexible operation integrates seamlessly into Linde’s existing manufacturing systems. Within the scope of the newly laid out material handling process, raw castings are deposited in a specially reserved and clearly marked staging area in front of the blast machine’s inlet chamber. An operator then manually positions the castings and prompts the system to transport the work pieces through the shot blasting chamber. Different PLC programs define and store specific shot blasting and transporting parameters based on the specific work piece being processed. This ensures that the various counterweight types are perfectly clean and free of residual molding sand after shot blasting. The work pieces also display highly homogeneous surface roughness and the typical casting structure even after subsequent painting. The Process After work pieces have been manually positioned in the staging area, trolleys on a power and free work piece transport system pick up and carry them through the different machine sections, including the inlet, blast, and outlet chambers according to predetermined indexing time intervals. A rendering of the RHBD 22/27-F’s blast media return and cleaning systems Despite being housed in a very tight space, Linde’s new RHBD is easily accessible for maintenance thanks to placing the return system for blast media and sand underneath the shot blasting machine. The system also includes a return system for sand left on the staging area after manual positioning. Both collections of sand and debris as well as any sand and blast media from the outlet chamber are transferred to the central screening hopper below the blast chamber where sand clumps, burrs, and metal flashings are separated, transferred to a sturdy Z conveyor belt, and discharged from the machine. The remaining sand/media mix is transported to an elevator and into a highly efficient media cleaning system. Consisting of a dual-stage magnetic separator and an airwash system, the media cleaner ensures high cleaning efficiency, guarantees trouble-free operation, and minimizes wear and tear on the shot blasting machine. The Specifications The three-chamber design of Linde’s RHBD shot blast machine also helps to minimize the escaping of sand, blast media, and dust into the immediate environment. The RHBD 22/27-F blast chamber At the center of the entire shot blast system is the blast chamber with five specially placed blast turbines. The chamber is made from wear-resistant austenitic manganese steel, grade X120Mn12. For additional wear protection, the blast chamber is also lined with 25 mm thick replaceable cast chromium plates. A large maintenance platform, easily accessible by stairs, greatly facilitates these and other required maintenance activities. The Rosler Way “Finding a better way
” is more than a motto at Rosler; it’s our mission. With more than 80 years of experience and a portfolio containing more than 15,000 equipment and consumable products, solving challenges is what we do. Contact us today to discuss your surface finishing goals and how we can deliver improvements!
StĂŒken rotary vibrator separation

Perfect finish for deep-drawn precision components

For tiny precision components with dimensions of < 1 mm and deep-drawn from 100 micrometer thick sheet metal, the surface finishing operation can be quite a challenge. StĂŒken, a worldwide leading manufacturer of such products, is meeting this challenge with custom-engineered equipment and specially developed media and compounds from Rösler. The solutions, offered by Rösler, guarantee a safe, risk-free deburring and edge radiusing process and ensure that the customer’s surface finishing specifications are fully met. A pioneering spirit, a forward looking company philosophy, an innovative approach and the conviction that efficient solutions can only be achieved in a cooperative environment - with this business approach Mr. Hubert StĂŒken started his business in 1931. 90 years later the Hubert StĂŒken GmbH & Co. KG is the world’s leader in the field of deep-drawn metal precision components. Stamped and bent parts, plastic-coated components and complex assemblies are complementing the product range of this family-owned company operating five manufacturing plants in Europe, the United States and China. The small high-precision parts are generally not visible after assembly. They are made from all metals that can be shaped by deep-drawing, such as stainless steel, copper, brass, aluminum, titanium and molybdenum. StĂŒken components are utilized in numerous technical products. For example, on average a fuel-driven passenger car contains about 40 StĂŒken parts. For vehicles with alternative drive systems this number tends to become even higher. The company’s components are also used in the products of such diverse industries as electronics, information and communication technology, medical engineering, pharmaceutical, household appliances and a wide range of consumer goods. However, they also play an important role in many other industries. Joint development of solutions – also for surface finishing To ensure that it can offer technically and economically optimal solutions to its customers, the company maintains its own R&D and development department at the corporate headquarter in Rinteln, Germany. Andreas Hellmann, sales manager at StĂŒken, comments: „For many of our customers we are a development partner. To perfectly adapt new products to their intended use, we are not only working with our customers but are also cooperating with partners from various technological sectors“. When it comes to issues around surface finishing that can be resolved by mass finishing, for 30 years the company has been relying on the experience and knowhow of the Rösler OberflĂ€chentechnik GmbH. The sales manager continues: „Our partnership is based on Rösler’s excellent quality, reliability and high uptime of the equipment and the good technical service. We also appreciate the company’s comprehensive knowhow and Rösler’s flexibility for developing solutions as a team. A major advantage is that Rösler has a technical presence at all locations, where we are manufacturing our components”. At its manufacturing locations around the world this deep-drawing specialist is using around 15 rotary vibrators, 10 centrifugal disk finishing machines and 18 centrifuges for cleaning and recycling of the process water. The deep-drawn components are generally characterized by an extensive degree of material shaping, complex geometries and extremely small dimensions requiring a high dimensional accuracy. This results in especially demanding specifications for deburring, edge radiusing and polishing of external and internal work piece areas. Equally challenging are the surface roughness and surface quality requirements. Dirk Schulz, project engineer at StĂŒken, explains in more detail: „On the one hand we must ensure that all pieces within a work piece batch receive the same high-quality surface finish. On the other hand, the metal removal rate on components with very thin walls and a large surface area must be limited so that the mass finishing operation does not damage or deform them. Furthermore, after completion of the finishing process the work pieces and the media must be reliably separated. A carry-over of work pieces and/or media into the next batch must be prevented at all costs!” This requires not only the precise adaptation of the finishing process to the work pieces. Likewise, the equipment and consumables must also be matched to the work pieces and the finishing goal. Frequently, this requires conducting special feasibility studies. Process development, equipment specification and media selection through processing trials For complex new components, the finishing processes are usually developed in the Rösler Customer Experience Center. This is equipped with ultra-modern machines that allow running a wide variety of different finishing processes. In extended processing trials the most suitable equipment technology and machine specification is defined. The trials frequently demonstrate that the usually smooth wear lining of the processing bowl of a mass finishing machine must be structured, in other words, must be somewhat rougher. „This prevents very small and light-weight components from adhering to the wall of the processing bowl. Also, to ensure a complete and reliable separation of the finished work pieces from the media, the separation units and screens must be frequently specially engineered”, explains Dirk Schulz. Of course, equally important is the optimal adaptation of the ceramic or plastic media type and shape to the respective finishing task. In order to achieve consistently good surface finishes, very often the media must have extremely tight dimensional tolerances. In a final step the process parameters, for example, the motor speed of the mass finishing machine, the batch size and cycle time must be defined. In this respect the comprehensive mass finishing experience and knowhow at StĂŒken plays an important role. Highly effective process water cleaning and recycling The finishing operation is not the only factor that determines the quality and cost-efficiency of a mass finishing process. Equally important is the system for cleaning the process water. The project engineer explains: „The finishing process is removing material from the work pieces and the media that contaminates the process water in the form of small metal and media fines. These fines must be reliably removed from the process water, before it can be re-used in the finishing process. For this purpose we are utilizing cleaning centrifuges, which are also supplied by Rösler”. The perfect technical adaptation of the Rösler centrifuges to the respective cleaning tasks ensures a high cleaning effect so that the cleaned process liquid can be recycled to the mass finishing process for re-use. This saves not only valuable resources but is also very eco-friendly. The optimal and consistent surface refinement of precision components made with the deep-drawing method requires the perfect interplay between equipment technology, consumables and process water cleaning. Generally, the best results are achieved by close cooperation with the customer.

New Compounds Double Process Water Usability

Experienced manufacturers know that optimum mass finishing process water handling, dosing, and recycling can significantly reduce operational costs and improve finishing results. With approximately 15,000 different products and the largest, continuously expanding range of media and compounds in the world, Rosler has the machines, consumables, and the experience to develop and maintain precise, efficient, and sustainable surface finishing processes. Our latest innovation in the field of consumables, Long Life Compounds known as LF compounds , allows mass finishing operations to further optimize their process water cycles. Advantages LF compounds utilize a special combination of raw materials to guarantee a remarkably high degree of sanitary stability. So much so that, in most cases, the addition of biocides to process water can be eliminated or greatly reduced when using these new compounds. Cleaner water, in turn, extends the usable life of your process water by nearly twofold. These savings in water and compound usage as well as associated disposal costs produce cost savings of up to 60%. These compounds also assist in optimizing mass finishing operations by lowering maintenance costs of the water recycling/circulation system itself and producing increased system availability and productivity. Applications Generally, any process with a recirculation system can utilize LF compounds. Finishing applications in need of increasing bactericides and hazardous substances, in particular, are good candidates for the use of LF compounds. Processes in need of defoaming compounds or additives also benefit from switching to LF compounds. Options Typically used to reduce issues of foaming, Rosler’s ZF compounds have been further optimized leading to the introduction of the long life LF compounds range. Effective properties of these existing compounds have been integrated into the new products along with improved system hygiene features. The LF compound line will continue to grow. Currently available formulas and their defining characteristics include: LF 110 – Offers the highest corrosion protection. LF 113 – Designed for universal application. LF 138 – Designed for universal application with good degreasing properties. The Rosler Way We understand that your work pieces deserve special treatment. When it comes to placing the optimal finish on their surface, you can rely on Rosler’s consumables and equipment. With more than 80 years of experience and an ever-evolving catalog of developments and innovations, we are confident that we can improve your surface finishing processes. Contact us to discuss your mass finishing and process water needs.
Mass finishing solutions for electric vehicles

Mass finishing solutions for electric vehicles

Vehicles driven by batteries or fuel cells and plug-ins contain a large amount of electrical and mechatronic components. These include connectors, circuit boards and busbars. For transferring the power they must handle high electric volumes. To function well, they must be free of burs and perfectly clean. For this surface finishing task the mass finishing technology represents a highly effective and economic solution. By fine-tuning the equipment and the consumables (media and compound), all developed and produced in-house, Rösler ensures that the required surface finishes are consistently achieved within short cycle times. Mass finishing systems are also used for finishing copper bars and various kinds of stampings. Copper bars are increasingly employed as winding material for rotors, whereas bent and stamped components are used for all kinds of housings. Friction causes not only increased wear and fuel consumption. It also generates unwanted noise emissions, vibrations and increased temperatures. Minimizing friction is, therefore, an important goal for components in vehicles that are powered by batteries or combustion engines. The optimal surface smoothing of components such as gears, cam segments, piston rings and camshafts are achieved with fully automatic mass finishing systems, for example, drag and surf finishers. The component surface is not only smoothed by removing roughness peaks and valleys. In addition, the components are also completely deburred. Such multi-function finishing operations in one single process generate significant cost savings and repeatable results.
Preservation line

Preservation lines in a class of their own

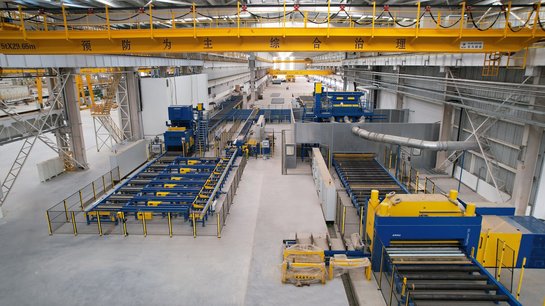
When it comes to top-of-the-line preservation lines, be it for shipyards or steel rolling mills, customers around the world rely on the technical competence of Rösler. This is not surprising, because Rösler offers not only comprehensive knowledge and many years of experience but has also implemented numerous reference projects. Another positive aspect are the project teams consisting of experts from the respective Rösler sales branches and the specialists from the head office in Untermerzbach, Germany. This close global cooperation produces technical solutions with numerous benefits to the customers. CMCS – successful entry into a new market segment China Merchants Cruise Shipbuilding (CMCS) is one of the leading manufacturers of expedition ships, floating platforms and floating cranes. To date the company had outsourced the corrosion protection of the steel plates and beams required for the production of its products. With the expansion of its business activities into passenger and cruise ships the company had to abandon this outsourcing policy. The construction of a midsize passenger ship alone requires 25,000 metric tons of steel. For this reason, the company looked for a partner for the design and installation of a high-performance preservation line . After an extensive analysis of the market the Chinese ship builder chose Rösler as supplier for this crucial investment. Key factors for this decision were the implementation and technical, efficiency of several preservation lines at European shipyards. Rösler was the only supplier who could present such an impressive reference list. Fully automatic interlinked steel preservation offers competitive advantages The 180 meter long preservation solution was specially engineered to meet the requirements of CMCS. It includes a plate section, the so-called main line, and a steel beam section, from which the shotblasted beams are fed into the main line. This unique preservation line consists of two roller conveyor shot blast machines, equipped with perfectly adapted Gamma 400G and Rutten 400 HD turbines , a straightening system for the beams and up to 12,000 mm long plates, a fully automatic coating system including a paint supply unit and a thermal post-combustion system. All these line components are digitally connected and integrated into the production control system of the shipyard. This intelligent control system allows the fully automatic processing of the steel components from the loading to the unloading zone at a speed of five meters per minute. The short pass-through times, a high process stability and consistent coating results provided CMCS with a significant competitive advantage. Of course, this was enhanced by the sturdy and wear-resistant design of the preservation line along with significantly lower personnel costs. A new dimension of corrosion protection for steel plates One of the largest manufacturers of steel and associated products with plants in the United States, Canada and Mexico convinced to purchase their new preservation line from Rösler. In this case it was the excellent experience with a preservation line installed a few years ago at another plant that prompted the major US company to choose a Rösler preservation line. The size of the steel plates with a width of 4,300 mm, a length of 18,000 mm and a thickness of up to 200 mm required a custom-engineered solution. Handling of loads of up to seven metric tons per running meter The entire line, in which the steel plates are preheated, shotblasted, painted and dried, had to be designed for loads of seven metric tons per running meter instead of the usual three tons. The integrated roller conveyor blast machine has a usable width of 4,500 mm and is equipped with 10 Gamma 400G turbines, each with an installed power of 30 kW. Such a “fire” power ensures that consistent, homogeneous shot blasting results are achieved across the entire width of the plates at a speed of 4 m/minute. This guarantees a high productivity.

AM Solutions Delivers Post-Processing Solutions for Prototypes & Parts

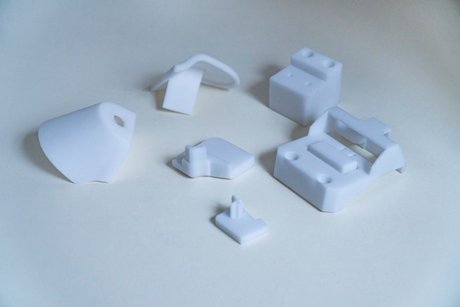
Knaus Tabbert AG is a leading manufacturer of recreational vehicles. The company’s innovative designs and powerful drive systems for motor homes, caravans, and panel trucks allow for safe, comfortable, and sustainable travel. At its German headquarters in Jandelsbrunn, Bavaria, Knaus Tabbert utilizes its comprehensive experience and know-how to continuously improve the materials and designs of its vehicles as well as new manufacturing technologies such as additive manufacturing. Seeking faster and less expensive post processing for its 3D printed prototypes, Knaus Tabbert turned to AM Solutions , a brand of The Rosler Group , to find a better way. Challenging Post-Processing From prototyping to production, Knaus Tabbert needed de-powdering and cleaning operations for additively manufactured work pieces. “On the one hand, we are using 3D printing technology for creating prototypes. On the other hand, we are also utilizing additive manufacturing for producing standard components in volume such as the bracket for an alarm system or the hinge mechanism for the swing-out shower stall,” said Mario Meszaros, Knaus Tabbert Development Engineer. De-powdering and cleaning of PA 12 polymer components produced by a powder-bed printing system were being done manually in a blast cabinet, producing highly erratic and inconsistent results as well as a lot of time and labor. The company wanted a more cost-effective and consistent automated alternative. Polymer parts used by Knaus Tabbert Comprehensive processing trials with different Knaus Tabbert components took place in the AM Solutions' Customer Experience Center . This division of The Rosler Group specializes in post-processing solutions for 3D printed components. After the conclusion of the highly successful processing trials, the customer chose the S1 shot blasting system . Perfect Cleaning & Quick Amortization The S1’s fully automatic operation delivers efficient finishing with absolute cleanliness. This shot blast machine was specifically developed for the post processing of plastic components produced with the powder-bed printing method. Featuring a plug-and-play design, the S1 is the only machine on the market to allow time-saving and cost-efficient de-powdering as well as surface smoothing and homogenization of 3D printed components in one single machine. All that is required is a simple change of the blast media , for example, from glass beads to plastic spheres. Equipped with a basket that rotates during the finishing operation and allows easy, ergonomic loading and unloading of the work pieces, the S1 offers fully automatic batch processing. Throughout the entire process—from loading and treatment to unloading—the basket remains in the machine housing. This, combined with a special door sealing system and antistatic system, prevents any powder spillage into the immediate surroundings. The control panel allows an easy and quick switch to manual operation without any retooling. “The fact that after surprisingly short cycle times the components came out of the machine perfectly clean and without any powder residues was very impressive,” Meszaros said. “With the underlying operating data, I prepared a ROI calculation. The results quickly convinced our management that, even with only three print jobs per week in the S1, we will achieve a return on our investment after roughly two years.” Since it is safe to assume that the quantity of 3D printed components will increase significantly, Meszaros said he expects that the amortization period will be drastically reduced as the S1 is used more extensively. Process Stability & Operational Safety In addition to excellent processing results and rapid amortization, the S1’s standard version also features a system that automatically monitors and records all relevant process parameters. The integrated blast media cleaning and recycling system drives high process stability by ensuring that media is always available in perfect condition no matter what type is utilized. The explosion-protected design of the shot blast machine with ATEX-compliant motors and valves provides additional peace of mind and safety. “I am absolutely convinced that the simple, effective, and efficient post-processing possibilities of the S1 will further promote the use of additive manufacturing in our company,” Meszaros said. David Soldan, Head of AM Solutions, agreed, adding that Rosler and AM Solutions provide finishing solutions to a variety of industries . “More and more companies from different industries are choosing the S1 for post processing their 3D printed components,” Soldan said. “This confirmation of our product strategy shows that our 3D post-processing products are in full compliance with the requirements of the market.” The Rosler Way “Finding a better way
” is more than a motto at Rosler; it’s our mission and why AM Solutions exists. With more than 80 years of experience and a portfolio containing more than 15,000 equipment and consumable products, solving challenges is what we do. Contact us today to discuss your additive manufacturing post-processing challenges!
RWK swing chamber blast machine

We are helping to build the car of the future

Integrable swing chamber blast machine enables parts processing in the production cycle The transformation of the automotive industry continues apace. At the beginning of June, the European Union decided to ban the sale of combustion engines from 2035. Subject to the approval of the individual EU member states, only electric cars or comparable climate-neutral vehicle systems may then be sold. To further increase their range, carmakers will rely even more on lightweight components in the future. However, lightweight components have already been used increasingly in automotive construction for years, for example to reduce emissions from classic internal combustion engines. Lightweight components include stator carriers, housings and components for drive technology, as well as axle and wheel mounts. These are produced by sand, pressure or injection molding. The parts then have to be finely desanded, deburred and their surfaces homogenized. For this purpose, our blasting technology experts at Rösler develop customized solutions. One of these is our compact swing chamber blast machine with automated parts handling. It was developed in such a way that it can be integrated into compact production lines in a space-saving manner. This enables parts processing in a production cycle - efficient, process-oriented and innovative. The advantages of the RWK swing chamber blast machine: Shortened cycle time due to simultaneous blasting as well as loading and unloading process Optimal for integration into existing production lines Process-safe pick-up of components due to integrated pneumatic clamping unit High blast intensity thanks to high-performance turbines Blast chamber made of manganese steel with additional exchangeable plates

Mass Finishing Work Piece Handling Series, Part 1 – Selecting the Best Work Piece/Media Separation Method

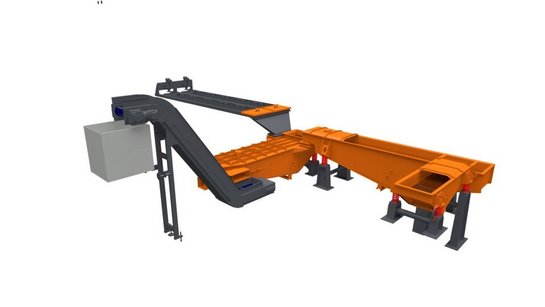
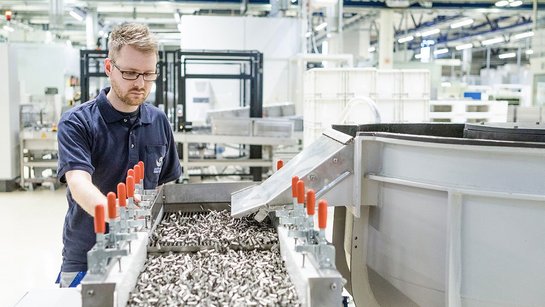
One of the first considerations in finishing process development is the ability to effectively separate mass finishing media from the work pieces. If separation cannot be achieved, the process will not be viable. Signs of inadequate separation may include the need for too much manual intervention, lodged media causing downstream process issues, failure to meet finishing standards, or even product recalls. For processes that do not require work pieces to be firmly mounted to fixtures in the machine, components and media loosely tumble in mass finishing processing bowls and troughs to achieve the desired finishing result. While this interaction is encouraged during processing, swift and precise media separation is crucial before work pieces move onto the next process step. Rosler has more than 80 years of experience designing mass finishing machines and supplying consumables. Our expertise can help develop the best separation method and settings for your unique combination of finishing, work pieces, and media. Separation Objectives If not properly removed from work pieces, media carried out of the machine can cause disastrous results in automated, downstream manufacturing operations such as machining, assembly, painting, etc. The manner in which media and work pieces are separated matters as well. The separation stage must not be too aggressive, as it could damage the finished work pieces with nicking and scratching if not carefully calibrated. Media and work pieces exit the machine outlet and pass over a polyethylene screen with round holes for external separation Separation must also take place in the shortest possible time to avoid costly extensions of the overall cycle time. The separation process should not require any support by the machine operator such as manually holding back the media/work piece mix on the separation screen. Separation Speeds While all machine types must meet the aforementioned separation objectives, some types require extra adjustments for vibratory motor speeds to aid the separation process within the machine. Where possible, separation is done in the finishing machine. This reduces the need for media handling, as the media remains in the machine and the parts are separated via built-in separation screens. Reducing the machine speed in rotary vibrators , long radius machines, and vibratory dryers after the higher intensity processing cycle provides more effective separation and minimizes part-on-part damage during the parts unloading step. Rosler rotary vibrator with internal separation screen Machines that require unloading the media/part mix from the machine at the end of the finishing process usually use external screening systems to separate the parts from the media. The external screening system has its own vibratory drive system that can be set and adjusted to maximize the screening speed while providing gentle part transportation. Rosler rotary vibrator with internal separation screen In either case, it is very important to select the correct screen type and hole size. Holes that are too small may cause media carry‐out while holes that are too large might cause work pieces to lodge in the screen or even fall back into the machine. The screen deck length must also be carefully considered. Methods of Separation In mass finishing, screen and magnetic methods of separation are most common. Separation Screens Available in a wide selection of hole sizes and shapes, separation screens are made of a variety of materials. Screen types include (top, from left) polyethylene screens with round or oblong holes, (middle) wire mesh screens coated with polyurethane or made from steel, and (bottom) bar screens made from steel or polyethylene Rosler offers numerous screen options, including: Polyethylene screens with round or oblong holes. Wire mesh screens coated with polyurethane or made from steel. Bar screens made from steel or polyethylene. Magnetic Separators When screen separation is difficult or even impossible, magnetic separators are a good alternative. For example, when the work pieces and the media have a similar shape or are the same size, magnetic separation is an excellent option. The use of magnetic separators requires that work pieces are ferrous and attracted by a magnet. These systems can be configured with a drum or belt as well as demagnetizing zones. Rosler magnetic drum separator Rosler magnetic belt separator Updates for Existing Systems Consult with your supplier to learn about the available separation options for the mass finishing machine you are using or intend to use. Available equipment updates may include: Frequency inverters enabling you to vary the motor’s speed. Most vibratory motors run at two speeds; namely 1,800 RPM (4‐pole mode) or 1,200 (6‐pole mode) by default. Installation of different screens utilizing different materials and hole sizes and shapes. Magnetic drum or belt separators. Regardless of the upgrade, ask your supplier to run a test processing trial before installation to ensure the change is satisfactory. Rosler offers free testing in our global Customer Experience Centers . The Rosler Way Decades of experience and ability to design, service, and maintain machines as well as the consumables and accessories to get the finish you require make Rosler a well-rounded surface finishing expert. Contact us to discuss your mass finishing and work piece handling needs. The complete Mass Finishing Work Piece Series includes: Part 1 – Selecting the Best Work Piece/Media Separation Method . Part 2 – Preventing Drop Height Damage . Part 3 – Maintaining Wear Linings .

Mass Finishing Machine Settings Series, Part 2 – Determine Imbalance Weight Settings for Consistent Results

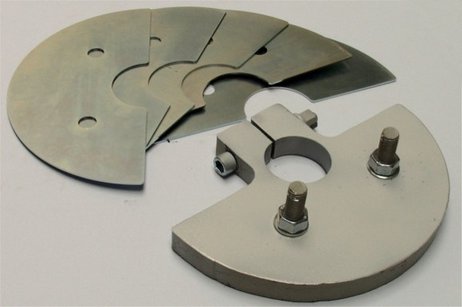
Specific mass finishing applications are developed through processing trials. Once defined, users should not deviate from the determined machine settings unless necessitated by work piece or process changes. Rosler partners with clients to provide testing in our global Customer Experience Centers to demonstrate our capabilities on a specific work piece and to calibrate machine settings. Determining the exact machine settings requires considering and testing multiple factors. Vibratory Systems The most common drive systems in mass finishing are vibratory. This refers to actual finishing machines such as rotary , tub , and linear continuous flow vibrators as well as auxiliary equipment like screening systems, vibratory conveyors, buffers, etc. In all of these cases, the speed of the vibratory motor or the electric motor driving the imbalance unit(s) may have to be adjusted as well as the setting of the imbalance weights. Vibratory weight plates The angle between the upper and lower imbalance weights determines the movement of the media and work piece mix within the machine. The number (mass) of imbalance weights determines the processing intensity (amplitude). More weights produce higher intensity while fewer weights deliver lower intensity. Vibratory motor diagram Setting Imbalance Weight s The movement of the media/work piece mix is always opposite to the motor direction. Typically, the motor runs clockwise and the media/work piece mix runs counter clockwise. In some instances, the motor can run clockwise and counterclockwise including the Rosler “R” machines and gate clearing in Rosler “Euro” machines. Half-circle metal plate weights on the top and bottom of the motor must be positioned with respect to each other. For a basic setting, the bottom weight plate must be turned 90 degrees forward of the top weight plate, in a basic setting. Imbalance weights locations and settings within a vibratory motor When setting imbalance weights, it is important to understand the impact of changes. For example, increasing the lead angle will make the media/work piece mix travel around the work bowl faster. Decreasing the lead angle will have the opposite effect, slowing movement. Typical lead angles range from 70 to 120° and can be observed by checking the gauge on the top of the motor shaft. Vibratory motor lead angle gauge Within the imbalance weights, the top weight controls the travel speed of the media/work piece mix around the work bowl. Adding additional weights to the top will increase the travel speed while decreasing the spiral speed in the work bowl. The top imbalance weight controls media and workpiece speed around the work bowl as represented by the red arrow while the bottom imbalance weight controls the spiraling speed of the work bowl contents. The bottom weight controls the spiral speed of the media/work piece mix in the work bowl. Conversely to the top weight, adding additional weights to the bottom will increase the spiral speed but also decrease the travel speed around the work bowl. Action Points Regularly checking a mass finishing machine’s settings including motor speed(s), setting of imbalance weights, work station angles, etc. to ensure they are as initially established will produce better results and protect the systems ROI. A vibrocope sticker on the work bowl allows for a quick check of the processing intensity. Additional information can be found in our Using Vibrascope to Measure Amplitude v. Frequency in Vibratory Bowls blog post. Virboscope sticker Additionally, if repairs require drive motors to be disconnected, make sure that they are rewired correctly and are not running in the wrong direction. If the machine settings must be changed, carefully follow the instructions in your operator’s manual or consult the manufacturer for assistance. If not already integrated, installation of a frequency inverter for precise setting of the drive speed of your machine may be available as an upgrade, providing additional control and oversight. The Rosler Way Rosler goes beyond developing mass finishing machines to provide operational insight and guidance for the lifetime of our machines as well as consumables and service . Contact us to discuss your needs and our capabilities. The Mass Finishing Machine Settings Series also includes Part 1 – Improve Machine Function with Proactive and Responsive Observation, Calibration .