Solution Finder
SOLUTION FINDER

Ваш гид по миру продукции Rösler

Всего за несколько кликов вы найдете машину, соответствующую вашим потребностям!

Результаты: 235 Статья - 53 Продукты

Are Your Additive Polymer Parts Breaking During Post Processing?

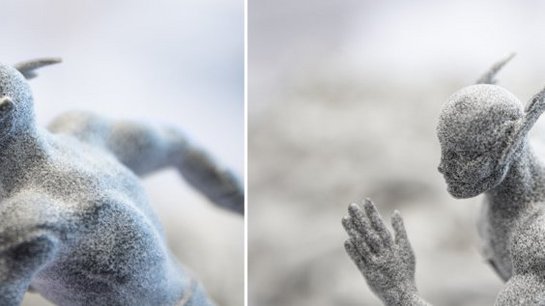
Growing utilization of additive manufacturing for volume production of plastic components has increased the demand for cost-efficiency and high-quality surface finishes. That’s why AM Solutions , a brand of the Rosler Group , has further expanded its product portfolio with the development of a media type specifically for the post processing of plastic components. Designed specifically for work pieces printed with MJF and SLS powder-bed-based technology, AM Solutions’ media permits the safe, cost-efficient finishing of 3D printed components with different shapes and sizes in one single process step and with absolutely repeatable results. This eliminates the time-consuming and costly media changes for different processing stages. In combination with an understanding of respective printing processes, the media mix generates a perfect, finely structured, and highly homogeneous surface finish. Experience-Based Design For this novel product, the AM Solutions experts took advantage of the comprehensive development know-how of the Rösler Oberflächentechnik GmbH. With more than 15,000 products Rosler offers the largest portfolio of media and compounds in the world by far. High versatility makes finishing processes simpler, safer, and more cost-effective. The material, shape, and size of the media has been perfectly adapted to the post-processing requirements of 3D printed plastic components. “The composition of the media mix was developed through numerous processing trials,” said Christoph Bätz, Project Engineer at AM Solutions. “The result is a product that allows the surface finishing of a broad spectrum of components with different shapes and sizes. Irrespective of whether small, delicate work pieces or large components must be treated, the result is always a highly homogeneous, consistent, and repeatable finish.” Simplified Processes The grinding performance depends on the geometrical complexity of the work pieces. For certain applications, the surface roughness can be reduced from Ra = 15 μm to Ra = 3 μm within 240 minutes. Multi-stage finishing processes frequently require multiple media changes. Since the new MJF/SLS media already contains an optimum mix of different shapes and sizes, the need for such changes could be eliminated. Maintaining the correct processing sequence is also no longer necessary. This facilitates the overall handling ease considerably. Since the media type can be used for a broad range of applications, there is no longer a need to stock multiple media types for different work piece categories, presenting a significant cost saving. Increased Benefits Higher cost-efficiency is only one part of the story. The media also helps improve the stability and safety of the finishing processes. Thanks to its mostly digitized and tightly controlled manufacturing process, consistently high quality of the ceramic media is guaranteed. “Decades of valuable experience allow us to continuously develop new products that offer a significant added value for our customers and provide solutions to the challenges they have to face,” Rainer Schindhelm, Division Manager for the Production of Consumables at Rösler Oberflächentechnik GmbH comments. “The perfectly adapted interaction between machines, consumables, and process know-how makes the innovative, unique solutions of Rösler and its brand AM Solutions' 3D post-processing technology highly successful.” Adaptive Results The media allows for efficient surface grinding of extremely delicate components without causing any damage. Typically, surface finishing of particularly delicate work pieces with complex geometries poses especially demanding 3D post-processing challenges. In combination with optimized printing methods, the media mix generates highly homogeneous results for these difficult finishing tasks while simultaneously minimizing scrap and reducing costs. Work pieces with delicate, fine structures pose significant post-processing challenges. At left, problems frequently caused by inefficient post processing are shown. At right, improved results delivered using Rosler and AM Solutions’ offerings are shown. Finding a better way… Utilizing Rosler’s more than 80 years of expertise, AM Solutions 3D post-processing technology can assist you in optimizing your engineering and improving overall results. At Rosler, “Finding a better way…” is more than a motto. Contact us today to discuss your challenges!

Structural Steel FAQ, Part 1 – Why Surface Preparation is Necessary

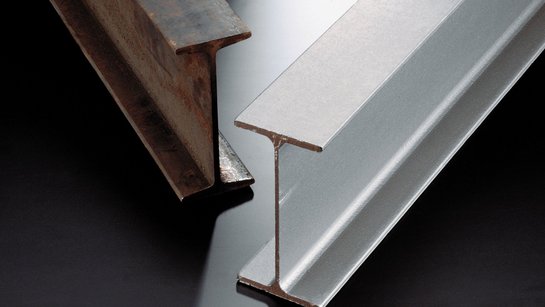
Structural steel components are used in many industries , including construction and construction equipment , shipbuilding , and the production of all kinds of heavy-duty vehicles, trucks, railway vehicles, and agricultural implements. In the construction of bridges, building of ships, or production of equipment that must withstand heavy loads, steel is selected for its strength and durability. To live up to its full potential and prevent premature failure, the steel must be guarded against corrosion with a protective coating. Shot blasting plays an indispensable role in preparing the steel surface for such coatings. Partnering with a shot blasting expert such as Rosler can help you determine the shot blasting equipment, blast media , and processing required for your structural steel components. In a series of blog posts, Rosler will answer the most common questions about the surface preparation and coating of structural steel. We begin with a basic question: Why do structural steel components need to be prepared for protective paint coating? The answer, in short, is for the best coating results and longevity. Goals of Surface Preparation If not covered with a suitable, protective coating, structural steel components are prone to rust quickly and fail with potentially catastrophic consequences. The effective life of a coating of anti-corrosive paint applied to a steel surface is largely dependent on how thoroughly the surface has been prepared prior to painting. Structural steel components requiring protective coatings include: Beams (I‐beams, H‐beams, channels, angles, etc.). Steel plates. Round bars and pipes. Weldments. Preparing and coating the surfaces effectively increases their durability and improves their appearance. Issues to Watch For A variety of factors can create surface issues necessitating proper preparation before coating such as the steel rolling process itself and prolonged exposure to the elements, water, or chemicals. Specific surface factors in need of attention include: The presence of rust or mill scale. The presence of surface contaminants. Surface profile or roughness. The presence of these and other contaminants on the steel surface can cause premature coating failure. Painting a surface with the wrong surface profile/roughness can also cause premature failure or drastically increase paint consumption. To achieve good coating adhesion, the surface profile generally must become somewhat rougher, increasing the overall surface area. Tools of the Trade While numerous cleaning techniques such as hand and power tool cleaning, high-pressure water jetting, and degreasing are used for surface preparation, dry shot blasting is the most common industrial paint preparation method for structural steel components. This method utilizes ferrous metallic abrasives and can be used in combination with other methods. For example, pre-cleaning steps are frequently required before the shot blasting process. Go-to Guidelines Surface issues for structural steel components vary greatly. Fortunately, users can rely on detailed standards describing the visual evaluation of surfaces and procedures regarding the correct surface preparation for coating and painting. The most commonly used standards address different surface characteristics of steel components and preparation requirements. ISO 8501 – Visual assessments of surface cleanliness, rust, and preparation grades of uncoated steel substrates ISO 8502 – Tests for the assessment of surface cleanliness ISO 8503 – Evaluates surface roughness characteristics of blast‐cleaned steel substrates ISO 8504 – Methods for abrasive blast cleaning AMPP - The Society for Protective Coatings (SPCC) and the National Association of Corrosion Engineers International (NACE) have merged to for the Association for Materials Protections and Performance (AMPP) ASTM D 2200 – Standard practice for use of pictorial surface preparation standards and guides for painting steel surfaces created by the American Society for Testing and Materials The Rosler Way Whatever your structural steel needs are and your materials’ starting conditions, you can count on Rosler to help you find a better way. Contact us today to discuss your unique challenges. Upcoming posts in the Structural Steel FAQ series will include: Part 2 – Methods of Surface Preparation. Part 3 – Evaluating Rust and Mill Scale Pre- and Post-Blast. Part 4 – Evaluating the Presence of Dust. Part 5 – Assessing Surface Profile. Part 6 – Blast Media’s Influence on Surface Profile. Part 7 – Comparing Commonly Used Blast Machines. Part 8 – Are All Turbines Created Equal? Part 9 – Removing Residual Blast Media and Dust. Part 10 – Blast Rooms for Touch-Ups. Part 11 – Preservation Lines. Part 12 – Material Handling Options.

Intuitive Post Processing Preserves Intricate 3D-Printed Details

AM Solutions , a brand of The Rosler Group , provides post-processing solutions for a number of customers worldwide. For leading manufacturer of wide-format inkjet printers and high-precision cutting plotters, Mimaki , Rosler and AM Solutions collaborated with the Japanese printer manufacturer to develop a fully automated surface finishing system for a Full-Color Inkjet 3D Printer. Through collaboration, a fully automatic machine capable of safely removing support structures for work pieces with the finest detail was developed. The Situation With the 3DUJ-2207 , Mimaki combines impressive color diversity with an imposing level of detail. The compact and affordable 3D printer with a build size of 8 x 8 x 0.4 in (203 x 203 x 76 mm) offers more than 10 million colors, high resolution, and, therefore, new application options in the field of professional additive manufacturing. Innovative uses of the printer include manufacturing prototypes, industrial design objects, and collectible figures as well as medical and architecture models. Usually, solutions for the removal of support structures are treating the work piece with wet blasting or a water bath. A safer, easier, and more efficient approach was required, since each of these processes involves the risk of damaging the often filigree 3D parts. Mimaki turned to AM Solutions for an automatized and production-ready solution. The Solution “With AM Solutions and Rosler, we have a partner with extensive know-how and experience in the fields of mechanical engineering, industrial surface finishing, and the development and production of consumables ," said Arjen Evertse, Mimaki General Manager of Sales. “At the same time, AM Solutions is among the leading suppliers of automatized post-processing equipment in the AM sector, where it pursues constant development.” The resulting post-processing solution consists of an Industry 4.0-ready plug-and-play system. Its matching compound is classified as non-hazardous and with a high flash point. The completely closed variant of the system already contains all the necessary safety features, making a regular 230 V electricity supply the only requirement for operation. Special casters make the repositioning of the machine easy. Furthermore, the system is equipped with a web interface enabling operation and monitoring via smartphone. Together, Mimaki and AM Solutions provide innovative printing technology and a well-matched assortment of post-processing equipment at an attractive price from a single source. At the same time, post processing can be up to three times faster than with equipment previously available on the market. The Process While the need for aggressive wet blasting has been eliminated, the solution includes accommodations to make the immersion bath less damaging to intricate filigree features on the work pieces. The fully automatic removal of the support structures is achieved by placing the 3D parts in an immersion bath via a basket and selecting the most fitting processing parameters. For this purpose, various programs are available in the equipment controls by default. Pre-saved programs cover a range from bigger parts with many support structures to very delicate printing objects. In addition, users can configure programs for their 3D parts themselves and save specific settings within the equipment controls. Once selected, the specific chemical, mechanical, and thermal effects interact according to the program’s specific parameters, and the prescribed interaction ensures that the support material is completely removed in a way that is gentle on the component and, at the same time, effective and fast. After a defined processing time, the basket is removed from the immersion bath. Dripping compound is collected and returned to the dip tank. Due to the classification as non-water hazardous, the parts can simply be rinsed under running water before subsequent processing and handling. Process Advantages Initial tests have shown that this specific support removal is up to three times faster than other systems on the market. One crucial advantage of the significantly shorter processing time is that it prevents the work pieces from swelling in the bath. At the same time, the relatively low bath temperature prevents damage. An integrated monitoring system ensures that the system automatically shuts down if the temperature is too high. “With this innovative post-processing solution, we can offer future-oriented printing technology including safe and simple post processing at an attractive price-performance ratio and from a single source. We are confident that this allows us to contribute to establishing 3D printing in new application areas,” Evertse said. David Soldan, Head of AM Solutions – 3D post-processing technology, agreed. “The collaboration with Mimaki gives us the opportunity to further deepen our expertise and to perfectly adapt our product development to the requirements of every user,” he said. The Rosler Way Decades of experience and the ability to design, service, and maintain machines as well as provide the consumables and accessories required to get the finish you require make Rosler a well-rounded, single source for surface finishing expertise. For additively manufactured components, AM Solutions builds upon Rosler’s expertise with innovative post-processing solutions. Contact us to discuss your surface finishing needs.

A Holistic Look at Automated Blasting in the Modern Metal Fabrication Shop

Written by Rosler CEO Bernhard Kerschbaum, this article was originally published in The Fabricator . Modern metal fabrication operations aren’t like the fab shops of old. Many are clean, well lit, with employees working in fresh, filtered air. Yes, some operations in fabrication are, well, just plain dirty—and manual blasting is a prime example. The work isn’t pleasant, requires protective gear, and if the booths aren’t maintained or set up properly, they can constrain workflow in a serious way. Options in blasting automation abound, but before diving into all that technological wizardry, try laying some groundwork by answering a fundamental question: What must the blasting operation accomplish? Shot Blasting Versus Shot Peening Shot blasting (or just “blasting” if using a different media other than shot) prepares a metal surface while shot peening aims to change the metal’s properties (see Figure 1 ). Certain aerospace applications require precise levels of stress relief (or other changes to material properties), and they use specialized shot-peening technologies to achieve it. Precision shot peening of landing gears is a prime example, with the process optimizing surface stresses, eliminating microcracks and the stress risers around them. Most metal fabricators employ blast cleaning for the vast majority of their applications, cleaning and preparing a metal surface for the next manufacturing step, usually painting. If a beam or plate isn’t blasted correctly, paint won’t adhere properly. However, some fabrication operations do employ a kind of peening—not as precise as high-end peening applications, but it’s peening nonetheless, with the media impacting the surface and causing compressive stresses that aim to change the material’s properties. Imagine fabricating a bowl that will be used in a high-vibratory setting. The welds within those bowls need a certain amount of stress relief, and shot peening helps accomplish this. To ensure adequate stress relief for the welds, the application might choose to use large shot, which can have a peening effect that penetrates deeper into the surface. Alternatively, the operation might choose to use the same shot that it uses for blast cleaning applications, though extending the cycle time to achieve the required peening effect within the part. When to Blast? Again, the majority of fabricators need to prepare a workpiece surface for a downstream operations like painting—so, they’re blasting (not peening). The higher quality the end finish is, the more important surface preparation becomes. Put another way, a high-quality, highly consistent coating requires a high-quality surface preparation. An automotive car panel requires very different surface prep compared to a structural beam. Where in the manufacturing sequence does it make the most sense to blast? Are cut plates being blasted to prepare them for downstream processes, or will the completed fabrication be blasted after bending and welding? Applying blasting to incoming material might seem counterintuitive, especially if welds need to be blasted anyway. After all, most operations that employ blasting do so just before it enters the final coating process. Still, blasting needn’t always occur at the end of the value stream. Sometimes, cleaner material coming into the shop can help downstream processes like cutting and welding, and it might help streamline the final finishing operation significantly. Some operations might choose to automate the blasting of incoming material yet keep the final blasting of welds manual, before the work enters the final coating process. The operation isn’t entirely automated, but because incoming material is clean, overall throughput rises dramatically, and time and labor required for manually blasting the fabricated parts is significantly reduced. Coating also doesn’t necessarily need to occur at the very end of production. For instance, some shipyards blast incoming plate, prime them with a weldable primer, then weld. Afterward, the work is blasted again—but only the welded seams. For large workpieces especially, such a manufacturing sequence helps streamline the overall operation significantly. Blasting Variables The industry has various standards (such as those from SSPC and NACE) to help fabricators assess the surface condition of material. The cleaner the material, the less aggressively you need to blast it, and the less aggressive blast media you need to use to achieve the desired finish. When working with plate with significant rust, shot might need to be larger, or the application might call for grit, which is angular. Round shot usually produces a finer finish than grit, but grit might be required to produce a rougher surface profile for adequate adhesion for a thick coat of paint. FIGURE 1. For fabricators requiring shot peening, for weld stress relief or any other application involving a change in material properties, maintaining the proper mix of media is critical. Fractured and undersized media must be continuously and consistently removed from the peening system. Consider the condition of raw stock and the final finish required—that is, what’s delivered versus the final surface finish you need to achieve before the product ships. The difference between the incoming and outgoing material quality determines the blasting throughput. The greater the difference in quality (that is, very rough to a fine finish), the longer the blasting will take. Some applications also might require several blasting stages, the first to clean and another secondary stage, using finer blast media to dial in the surface’s paint adhesion characteristics. “Speed” in blasting can be defined several ways. First, how much shot needs to hit the surface at a given time, and how often the shot needs to strike to remove rust and prepare the surface as needed? The more rust a workpiece has, the more shot it will require. One turbine might throw 500 lbs./min. of shot at a slow-moving workpiece, to ensure enough shot strikes the surface enough times to create the surface finish needed. Alternatively, a system can have multiple blast wheels, positioned one after the other, that throw (altogether) 1,500 lbs./min. to the surface, which allows parts to travel three times as fast. There’s a limit to this, of course. Throw too much shot, and the shot media begins to ricochet within the system, which in turn creates all sorts of inconsistencies. Thrown at a high enough volume, the blast media itself loses its effectiveness. Several variables control blast intensity. An operation can adjust the feed valves to control how much media flows onto the turbine. Alternatively, an operation might slow the turbine speed, so the blast media itself hits the part at a slower velocity. An application has an optimal exit velocity; too low, and the media isn’t effective (for instance, it fails to knock off surface rust); too high can cause other issues, like warping, especially for very thin workpieces. Another variable involves blast media size distribution. Automated systems have recycling systems that separate the blast media from the removed rust and debris. The recycling system itself is extremely critical; if it’s not operating properly, the blast media won’t be consistent, which can lead to paint adhesion and other challenges. Shot becomes smaller and smaller as it’s recycled. The blast media recycling system must be monitored to ensure enough fresh shot or other media is added to the mix, and that the screening system (which evacuates fine particles) is working properly. The procedure isn’t complicated. Operators essentially take a blast media sample and send it through several specially designed sieves, so they can see the coarseness distribution and any debris or contaminants that might be present. Anatomy of a Blast Machine Blast machines carry the parts through the blast stream, collecting as little media as possible on the part while also exposing every surface that needs to be blasted. The blast stream the turbine throws has a “hot spot” near the center, an area where the blast media carries the most energy. This in turn governs the optimal position of the turbines (see Figure 2 ). For instance, a blast machine that processes plate requires even distribution of blasting across the surface, and if those hot spots in each blast stream don’t overlap, the plate might end up with “stripes” in areas exposed to less blast media. These basics form the foundation of any blast machine design. A popular design for metal fabrication includes roller-type machines, where widely spaced rollers (see Figure 3 ) carry plate or beams into a machine, where it’s blasted from multiple directions. Placement of the turbine is key (see Figure 4 ). Some machines might place blast turbines a certain distance away to accept, for example, various beam geometries. The arrangement might not be as efficient for plate as a machine with turbines placed closer to the work, but the arrangement does offer flexibility—that is, the system can process both flat plate and beams of various shapes and sizes. FIGURE 2. Turbines emit overlapping blast streams to ensure all workpieces receive sufficient coverage. Again, when the work is blasted plays a role too. That flexible machine might blast raw plate to clean and prepare it for downstream processing, then blast the assembly after welding. A shop might employ this strategy because of blast media access issues (that is, a machine’s blast media can’t access all surfaces of the assembled product), or because welding requires clean surfaces that the blasting process produces. Alternatively, the company might choose to “blast twice”—both incoming stock and welded products—because it’s still the fastest, most efficient way to process the work. Cleaning raw stock as it comes in streamlines downstream operations. And because parts were already cleaned, blasting of the welded assembly takes less time. Which machine a fabricator chooses depends on the application requirements, including the part geometry. Flat parts or beams might be adequately blasted on a roller-type machine, while booms, buckets, or other complex shapes might call for a hanger-type or spinner-hanger-type machine. A bucket sent through a roller machine might start accumulating shot on its surface, which prevents the shot from hitting the surface with sufficient energy. In this case, a spinner-hanger blast machine, where a ring of blast turbines around a hung part that’s spinning, might be able to access all surfaces while still allowing the spent shot to fall from the part. The manual blast room’s principal benefit is operator access. The operator can blast all surfaces and brush off accumulated shot as needed. An automated system might not have this flexibility. At the same time, blast media from a turbine within an automated machine has much more energy than blast media from a manual gun. That energy can reduce the media buildup significantly. So, while a manual operator might be able to blast complex, challenging geometries, he also might have to brush off accumulated media more frequently. (Note: manual touchup blasting can be integrated into an automatic blast machine, such as a hanger-type machine. In that case, the operator suits up and blasts the part with a manual blast wand inside of the disabled blast machine.) On the other end of the spectrum, some blasting technologies offer complete automation—and not just of the entire blasting process. Some plate and beam blasting systems connect directly to a painting system (see Figure 5 ). Again, these help minimize the required surface prep later in the value stream. At the steel supplier or at the fabricator itself, beams and plates are blasted then immediately coated with a weldable primer. Such systems also can come with a cleaning station before blasting—especially useful for structural fabricators that store their material outside. That station removes the loose debris (like dirt, snow, and leaves) before the beams enter the blasting station. After blasting, the work passes through a cleaning station with brushes and air blowers, which remove any remaining shot or other debris before the pieces flow to painting and drying. Throughput for these systems depends on the material condition entering the machine as well as the painting requirements like thickness, consistency, and curing time. Designers of such systems have optimal throughput in mind. If curing time takes longer, then the blasting system could be altered to run slower (slower turbines, less media, or a combination of both). At the same time, not every workpiece need be sent through the painting system. For instance, a fabricator that cambers beams or forms plates downstream wouldn’t want to paint those pieces upstream, so those workpieces that undergo those processes could simply be blasted and then quickly sent through the idle painting system, then on to cambering or forming. Again, it’s about overall throughput, not the “local efficiency” of a specific blasting or painting process. Yes, blasting might take a little longer when coupled with painting, and the painting system might not be used for every beam. But linking painting directly to blasting boosts overall flow and minimizes work-in-process—both of which represent huge time savings. The result: The shop blasts and paints more material in less time using fewer resources. About the Entire Value Stream In applications with widely varying or complex part geometries, a fabricator might choose to partially automate blasting, with a machine blasting 80% or more of the material surface and a manual operator blasting the remaining 20%. Automating the entire process is, of course, ideal for many applications—but not all. The idea is to implement automated blasting where it can be most effective. In other situations, the operator might need only to blow blast media off. Certain hanger-type systems, for instance, have a designated cleaning station where operators, for parts that require it, can perform a final cleaning before the part moves on to the next stage (see Figure 6 ). FIGURE 3. Widely spaced rollers carry plate, beams, or similar workpieces through into the machine. The aim is to streamline the entire value stream, and this extends up to material purchasing. A fabricator could buy more expensive material that requires less blasting or no blasting at all, or it could buy less expensive material that requires significant blasting and surface preparation. However, what if the welds require blasting regardless of material quality? As long as application requirements can be met, it might make more sense to purchase the less expensive raw stock, spend more time blasting, and yet (thanks to less expensive material) save money overall. A high-volume fabricator might even choose to bring an automated blasting and painting line in-house, not only because it increases throughput, but also because it allows the operation to purchase less expensive material and gain greater control over material surface quality—depending, of course, on the final application requirements. Some structural beam processing operations have effectively automated their entire flow, from blasting to cutting, painting, then loading directly onto trucks. In at least one European structural steel fabricator, one operator sits in an air-conditioned room and controls the entire operation. His main job is to monitor equipment and flag maintenance personnel should a problem arise—be it extra vibration on a blast turbine (detected through sensors), a blade vibration issue at the band saws, or anything else. Developing such systems didn’t occur overnight, and it didn’t happen by analyzing specific processes in isolation. Considering the entire value chain is key, including linkage with enterprise resource planning as well as the potential of AI-driven predictive maintenance. When this happens, fabricators often find they can take automation to new heights. FIGURE 4. A blast machine's turbine wheels (three of them just above the work entrance) are placed to accept a variety of workpiece geometries. FIGURE 5. In this setup, beams or plates are blasted, cleaned, then flow directly to painting for a weldable primer. FIGURE 6. Some systems offer automated blasting together with a manual cleaning station.

Partnership Provides Excellent Finish for Deep-Drawn Medical Components

Deep-drawn functional components are increasingly being utilized in the production of medical and pharmaceutical products. To meet the strict standards for manufacturing and quality management in the field of surface finishing, Hubert Stüken GmbH & Co. KG has relied on mass finishing solutions and consumables from Rosler for more than 30 years. Founded in 1931, Hubert Stüken GmbH & Co. KG is a family-owned business with manufacturing operations at five locations in Europe, Asia, and the United States. Its product range includes stamped and bent parts, plastic-coated components, and complex assemblies. Rosler works with Stüken Medical , the company’s medical business division which focuses on medical and pharmaceutical engineering, to meet the increasing demand for deep-drawn metal components. Andreas Hellman, Manager of the ISO 13485-certified business division, explained, “Components used in the field of medical and pharmaceutical engineering must meet strict quality standards. The same strict standards apply also to the actual production operations. For this reason, we have pooled the required know-how for the development and production of such precision components at Stüken Medical.” The Situation Among other items, this division produces complex housings and assemblies, valves, extremely precise micro parts, and primary packaging. These components are made from metals suitable for deep drawing, including stainless steel, aluminum, and titanium. To meet the strict quality standards in the medical and pharmaceutical industry, the company utilizes multi-stage cleaning systems and operates two class 7 cleanrooms. Its research and development department, located at the corporate headquarters in Rinteln, Germany, continuously explores the possibilities to expand the range of processes and materials. “For many of our customers, we are a development partner,” Hellmann said. “To perfectly adapt new products to their intended use, we are not only working with our customers but are also cooperating with partners from various technological sectors.” The Solution When it comes to issues around surface finishing that can be resolved by mass finishing, the company has relied on Rosler’s experience and know-how for more than 30 years. “Our long partnership is based on the excellent quality and reliability of Rosler equipment and consumables,” Hellmann said. “This helps us to ensure that the required results are achieved in a consistent manner.” Dirk Schulz, Project Engineer at Stüken, agreed. “When it comes to the joint development of finishing processes, we especially value Rosler’s flexibility and expertise,” he said. “In this respect, our access to the Customer Experience Center in Untermerzbach is extremely valuable. “Rosler also supports us with documentation and equipment details required for machinery and processes that must be qualified and validated in line with ISO 13485,” Schulz said. At its manufacturing locations around the world, this deep-drawing specialist uses 15 rotary vibrators and 10 centrifugal disk finishing machines for its finishing operations. Stüken Medical also operates 18 process water centrifuges for eco-friendly and reliable cleaning and recycling of the process water. Rotary vibratory machine with work pieces in the media mix The Requirements The deep-drawn components are generally characterized by an extensive degree of material shaping, complex geometries, and extremely small dimensions requiring high dimensional accuracy and especially demanding specifications for deburring , edge radiusing , and polishing of external and internal work piece areas. Equally challenging are the surface roughness and surface quality requirements. “On the one hand, we must ensure that all pieces within a work piece batch receive the same high-quality surface finish. On the other hand, the work pieces must not be damaged or deformed,” Schulz said. “Last but not least, after completion of the finishing process, the work pieces and media must be reliably separated. A carry-over of the work pieces and/or media into the next batch must be prevented at all costs,” he added. In conjunction with polishing jobs, the work piece surface must frequently be marked with a UDI code. Fully meeting these specifications requires finishing processes that are precisely tailored to the respective work pieces as well as carefully adapted equipment and consumables. Conducting special feasibility studies is often required to determine system parameters. Deep drawn component made by Stüken The process for radiusing the edges of 0.8 in (20 mm) stainless steel housings for a medical device was developed in close cooperation with Stüken. This delicate housing’s large surface area in combination with extremely thin walls posed a challenge. To remove sufficient material at the edges, a high processing intensity that could be tightly controlled was required to prevent any deformation. The Cooperation The Customer Experience Center at Rosler is equipped with ultra-modern machines capable of running a wide variety of different finishing processes and conducting trials to define the most suitable equipment technology under actual production conditions. During such development processes, the processing bowl of standard machines must be frequently modified, sometimes involving substantial engineering changes. For this project, the comprehensive mass finishing experience at Stüken was a valuable source of ideas. To guarantee a reliable and complete separation of the finished work pieces from the media, the finishing equipment for Stüken Medical required a few changes in the separation process. Another goal of processing trials is the determination of the optimal media shape and type ( ceramic or plastic ) for the finishing task at hand. In order to achieve consistently good surface finishes, very often the media must have extremely tight dimensional tolerances. Deep drawn component made by Stüken All ceramic and plastic media are produced at Rosler in compliance with the highest ecological standards. With over 15,000 different products, the media, compounds, and process water cleaning agents Rosler offers are by far the largest range of mass finishing consumables in the world. A key factor in the development of successful finishing processes is the perfect interplay between the right equipment technology and the right consumables (media and compound). Generally, the best results are achieved by close cooperation with the customer. The Rosler Way Decades of experience and the ability to design, service, and maintain machines as well as provide the consumables and accessories required to get the finish you require make Rosler a well-rounded, single source for surface finishing expertise. Contact us to discuss your mass finishing needs.

Interlinked Mass Finishing and Cleaning Systems Half Processing Time

Because of a positive experience with four continuous flow washing machines operating at its headquarters, VIA Oberflächentechnik (VIA) decided to work with Rosler for a comprehensive mass finishing and cleaning operation. The resulting interlinked system meets the most demanding cleanliness specifications while achieving significant cycle time reductions and cost savings and providing a high degree of operational flexibility. The Situation Headquartered in Lennestadt, Germany, VIA sought an integrated solution for de-oiling, mass finishing, and deep cleaning of stamped and formed parts. Since its founding in 1996, the job shop company has been one of the leading work piece cleaning specialists in Europe. Its three production locations process automotive and other components. An in-house laboratory ensures that the treated work pieces are in full compliance with the specified cleanliness demands. Depending on the stringency of the customer requirements, some products are even packed in a dedicated cleanroom. After extensive cleaning trials with pilot production runs, VIA received a large order from an automotive supplier for volume cleaning of clutch carriers. The company's existing cleaning and mass finishing capacities were no longer sufficient and had to be further expanded. Rosler mass finishing system The Solution “Right from the project start, it was clear that we would purchase a new mass finishing system from Rosler," said Kai Lechner, Manager at VIA. "We were not certain about buying the water-based cleaning systems from the same supplier, but after inspecting a fully automatic combined mass finishing/cleaning system that has been successfully running at an automotive supplier for several years, we decided to purchase the complete package from one supplier, namely Rosler," he said. Utilizing the Rosler team as the single supplier and integrator for the interlinked system provided numerous benefits. Since Rosler not only produces the finishing equipment, but also the washing systems, our extensive experience in integrating robotics allowed us to provide a turnkey solution for VIA. Based on prior successful partnerships with Rosler, VIA also knew we had the expertise and experience to be responsible for the process, minimizing the need for coordinating with different vendors and providing one point of contact for a complex project. VIA's new line consists of two cleaning units, a linear continuous flow vibratory inline system , and an automatic process water cleaning system ; all supplied by Rosler. The company also purchases its grinding media as well as all cleaning and finishing compounds from Rosler. “For us, it is a lot easier to deal with one partner who takes care of everything including service and maintenance," Lechner said. The Process For the de-oiling stage, the clutch carriers are manually placed on the feeding conveyor of the compact spray-rinse washing machine. During the 6-second cycle, they pass through two separate cleaning zones and one blow-off station. Filtration units and a coalescence separator increase the clean liquid systems' uptime utilized in the initial step. A single media is used in the various cleaning processes which allows the work pieces to be directly transferred into the mass finishing machine without a drying step. Deburring and edge radiusing take place in the linear continuous flow vibrator, type R 650/6600 DA. Process water used in the machine is continuously cleaned by an integrated Z1000 centrifuge equipped with fully automatic sludge discharge. A vibratory separation unit transfers work pieces from the mass finishing machine to a feeding conveyor and the deep cleaning unit parts washing system. To ensure that the work pieces meet the stringent cleanliness requirements of no metallic particles > 600 µm, the carriers are manually positioned prior to entering the deep cleaning unit. Work pieces then pass through a cleaning zone followed by a rinsing and passivation zone. In these zones, the parts are sprayed with a cleaning solution from above and below. The pressure and volume of the water flow from the upper and lower spray nozzles can be separately adjusted, and the various parameters can be stored as individual programs in the equipment controls. After passing through a drying zone, the work pieces are discharged. Process Advantages The operational flexibility of the system allows VIA to utilize the different modules in any conceivable combination. The combined cleaning/finishing system also allows the processing of other work pieces with similar size and shape. Compared to the pilot production's cleaning process and its numerous manual operations, the new system cuts the processing time in half. “A big advantage is that after an unplanned delivery stop by the customer, we can resume production much more quickly and can supply the OEM with cleaned work pieces in extremely short lead times,” Lechner said. The interlinked equipment concept also yielded considerable cost savings by reducing the required manpower for operating the system. It also greatly improved the working environment for employees since they no longer need to move the part bins between different machines, saving them time and effort. Decades of experience and the ability to design, service, and maintain machines as well as provide the consumables and accessories needed to get the finish you require make Rosler a well-rounded, single source for surface finishing expertise. Contact us to discuss your mass finishing needs.

Herzensangelegenheit Mitarbeiter-Ehrung – Rösler feiert endlich wieder im großen Rahmen

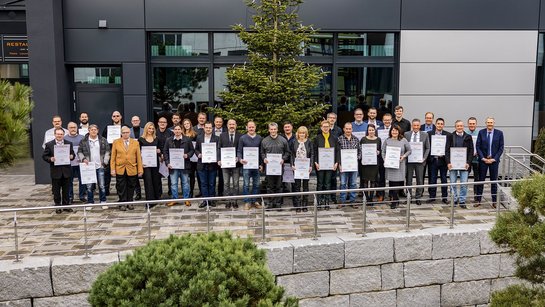
Im Jahr 1982 wurde Helmut Kohl Bundeskanzler der Bundesrepublik Deutschland, in Erlangen wurde das erste Retortenbaby des Landes geboren, und das US-Nachrichtenmagazin „Time“ wählte den Computer zur „Maschine des Jahres“. Alles entscheidende Ereignisse, die den Lauf der Welt maßgeblich beeinflusst haben. Für Maria Zillig und Thomas Eberth war das Jahr 1982 aber noch aus einem anderen Grund besonders einschneidend: Es war das Jahr, in dem sie ihre Ausbildung zur Industriekauffrau und zum Industriekaufmann begonnen haben. Und zwar bei der Rösler Oberflächentechnik GmbH in Memmelsdorf / Untermerzbach beziehungsweise Hausen. Dort arbeiten sie auch heute noch. Ganze 40 Jahre später. Genauso wie ihr Kollege Detlef Griebel, der ebenfalls seit 1982 bei „seinem“ Rösler beschäftigt ist. Einem Unternehmen so lange die Treue zu halten ist alles andere als selbstverständlich. Deshalb hat die Rösler Oberflächentechnik GmbH diese, und 39 weitere langjährige Mitarbeiter, jetzt im feierlichen Rahmen für ihre lange Unternehmenszugehörigkeit geehrt. Für den Geschäftsführenden Gesellschafter Stephan Rösler ist die jährliche Ehrungsfeier eine echte Herzensangelegenheit. In diesem Jahr ist sie es gleich aus mehreren Gründen: Nachdem die Ehrungen in den letzten Jahren aufgrund der Corona-Beschränkungen nur im kleinen Kreise stattfinden konnten, darf in diesem Jahr zum ersten Mal wieder im großen Rahmen gefeiert werden: Im neuen Rösler Betriebsrestaurant, welches 2021 am Standort Memmelsdorf / Untermerzbach eröffnet wurde. Bei der feierlichen Ehrung der verdienten Mitarbeiter bekam Stephan Rösler in diesem Jahr Unterstützung von seinen beiden Geschäftsführerkollegen Volker Löhnert und Oliver Grün. Letzterer wurde selbst für seine zehnjährige Betriebszugehörigkeit ausgezeichnet. Die Rösler Oberflächentechnik GmbH gratuliert … zum 40-jährigen Betriebsjubiläum: im Werk Memmelsdorf: Maria Zillig und Thomas Eberth. Beide sind dem Unternehmen nicht nur im selben Jahr, sondern als Lehrlinge auch am gleichen Tag beigetreten. Im Werk Hausen wird Detlef Griebel für vier Jahrzehnte Treue geehrt. … zum 25-jährigen Betriebsjubiläum: Eduard Fischer, Andreas Hentschel, Mario Jakob, Ralf Müller, Waldemar Riwe, Folkert Rothe, Steffen Schwab, Jens Siebensohn, Gerald Weiß, Katja Wohnig, Uwe Zörkler – alle tätig im Werk Memmelsdorf – sowie Ernst Hoffer, Peter Leipert, Rainer Schindhelm und Alexander Schröder im Werk Hausen. … zum 10-jährigen Betriebsjubiläum: im Werk Memmelsdorf: Norbert Wolf Dicker, German Gerstenlauer, Tim Gleichmann, Susanne Henkel, Christian Höhn, Martin Hopf, Kevin Kern, Kathrin Knöferl, Wolfgang Kroner, Marcus Mannel, Andreas Merz, Marco Schmittwolf, Arno Schneider, Holger Schwämmlein, Dominik Sperlich, René Stüllein, Sven Trier, Udo Weierich, Jennifer Weinland und Katja Weis sowie Katrin Fuchs, Oliver Grün, Ingrid Vetter und Yvonne Wagner im Werk Hausen. Nach langjährigem verdienstvollen Einsatz wurden Reiner Allert, Gerhard Edelmann, Uwe Fleischmann, Herwig Heiser, Imelda Hellmuth, Carola Jankowski, Wolfgang Panzer, Fredi Spangel, Martin Trutz, Theo Wirsching sowie Oswald Zöttlein in den Ruhestand verabschiedet. Kurs halten im Krisenjahr: Rösler hält an langfristigen Zielen fest Es war ein schwieriges Jahr mit vielen Unwägbarkeiten – dieses Fazit zog der Geschäftsführende Gesellschafter der Rösler Oberflächentechnik GmbH, Stephan Rösler, in seinem traditionellen Weihnachtsgruß an die Belegschaft. Man sei in den ersten drei Monaten gut gestartet, der Ukraine-Krieg habe dann aber vieles verändert – und die aufgrund der Corona-Krise ohnehin schon schwierige Lage an den Beschaffungsmärkten zusätzlich verschärft. Weitere Schwierigkeiten wie die Kostenentwicklung blieben aktuell, obendrauf kam noch die Energiethematik. Das im März 2022 abgelaufene Geschäftsjahr konnte die Rösler Oberflächentechnik GmbH zwar erfreulich mit einem unkonsolidierten Gruppenumsatz von rund 273,9 Mio. € und somit einem Gruppenplus von rund 16 Prozent abschließen und so die durch die Pandemie verursachte Umsatzdelle aus dem vorangegangenen Geschäftsjahr hinter sich lassen. Die Prognosen für das laufende Geschäftsjahr geben aber ein uneinheitliches Bild ab: So werden die Verfahrensmittel, Ersatzteil- und Serviceleistungen zwar weiterhin auf stabilem Niveau nachgefragt. Das Neumaschinengeschäft gestaltet sich allerdings schwieriger: Der russische Markt ist durch die Embargobestimmungen weggebrochen, außerdem ist durch die weltwirtschaftlichen Rahmenbedingungen insbesondere bei Großprojekten eine Zurückhaltung bei Investitionen festzustellen. Aus diesem Grund wird der Auftragseingang im Neumaschinenbereich zunächst unterhalb der Planungen liegen. Auch aufgrund einer Vielzahl getroffener Maßnahmen habe die Rösler Oberflächentechnik GmbH die zahlreichen Herausforderungen bisher aber „ganz gut bewältigt“, so Stephan Rösler weiter. An seiner langfristigen Ausrichtung gemäß der Firmenphilosophie Mission & Vision wolle das Unternehmen festhalten, zudem habe man 2022 trotz aller Schwierigkeiten einige wegweisende Projekte auf den Weg gebracht. Beispielsweise die Rösler Innowelt, ein umfassendes Konzept zur Umstrukturierung und Modernisierung fast des kompletten Bürobestandes am Standort Memmelsdorf / Untermerzbach. Langfristig erhoffe er sich auch durch zahlreiche Produktneu- und Weiterentwicklungen, die die Rösler Firmengruppe in den letzten Monaten auf den Weg gebracht habe, weitere Stärke, so Stephan Rösler. Im abgelaufenen Geschäftsjahr wurden ca. 5,6 Mio. € am Standort Memmelsdorf investiert und auch im laufenden Jahr werden weitere Investitionen in zukunftsorientierte Projekte an den deutschen Produktionsstandorten erfolgen. Seinen Mitarbeitern dankte der Geschäftsführende Gesellschafter für die tatkräftige Unterstützung und Loyalität im vergangenen Jahr. Trotz aller Schwierigkeiten konnte allen Beschäftigten das Weihnachtsgeld in voller Höhe ausgezahlt werden. Ein starkes Zeichen zum Ende eines Jahres, das aus vielerlei Gründen getrost als sehr schwierig bezeichnet werden darf.
wire mesh belt machine

Perfect de-flashing and dedusting of duroplast and thermoplast components at the production rate of the injection molding machine

Ever since ROS GmbH & Co KG was founded in 1926 the processing of plastic materials was always at the center of the company’s activities. Initially named Press plant ROS, the company now has a nearly 100 years old tradition in this field. Today the private business, managed by third generation family members, is a high-end partner for technically demanding injection molded components made from duroplast and thermoplast materials including polyphenylene sulfide (PPS). Product development, tool making, and production take place at the company’s headquarters in Coburg, Germany. An additional manufacturing plant is located in Ummerstadt in the German state of Thuringia. For removing the flashes on the components created by the manufacturing process the company has been working with Rösler shot blast equipment since 2006. Increase of the de-flashing shot blasting capacity Jürgen Bär, responsible for planning in the industrial engineering department at ROS in Coburg explains: „The demand for plastic components substituting metal parts, for example in thermo management systems for the automobile industry, has been rapidly growing. In 2021 this forced us to increase our shot blasting capacity at both our manufacturing locations. The plastic components reduce the overall weight of the cars and, therefore, help to reduce CO2 emissions. In addition, we received large orders for duroplast pre-formed components, among others from a leading manufacturer of garden tools“. After discussions with four suppliers of shot blast equipment the customer chose the wire mesh belt machine RSAB 470 and the swing satellite table machine RWS 1200 from Rösler. Jürgen Bär continues: „Deciding factors for choosing Rösler were our good experience with the shot blast machines we have been using for a long time, the compact, space-saving and sturdy equipment design and Rösler’s comprehensive knowledge in the field of plastic de-flashing. Moreover, we needed the continuous flow shot blast machine quickly. Rösler generously supplied a machine from their customer experience center within a few days“. Consistent and energy-efficient de-flashing in the tempering frame The flexible high-capacity shot blast machine RSAB 470 at the Coburg location is used for de-flashing of components made from duroplast and the high-performance thermoplast PPS-GF materials. After de-flashing the components undergo a tempering treatment. For this purpose, the components are placed on special frames. Normally the work pieces are placed individually on the wire mesh belt. To streamline the material handling operation and eliminate this time-consuming step, Rösler adapted the standard work piece transport system of the shot blast machine to the workflow at ROS. This re-design now allows placing the raw components on the tempering frames immediately after the injection molding process. The work pieces on the frames are then passing through the shot blast machine for the de-flashing operation and can, thus, be directly transferred to the tempering station. Four turbines, specially designed for plastic de-flashing and placed above and below the wire mesh belt, ensure consistent shot blasting results. This turbine arrangement allows throwing the media consisting of polyamide grains with a diameter of 1 mm onto the work pieces from above and below. Compared to the normally utilized suction air blast systems the turbines, equipped with electric drives, are considerably more energy efficient. Jürgen Bär adds: „Not only our certification per DIN EN 50001 demands a reduction of our energy consumption, but energy savings are also necessary to save costs and for reasons of sustainability“. A blast media flow control with automatic media replenishment ensures that there is always sufficient blast media available in optimal quality. The shot blast machine is equipped with numerous technical features such as the anti-static compound dosing system with automatic compound replenishment, the efficient air extraction from the blast chamber, the dual step parts cleaning system in the outlet zone and the effective blast media cleaning system with screen and air wash separator. All these features guarantee that the components coming out of the shot blast machine are perfectly de-flashed and absolutely clean. Since the plastic materials used at ROS and the polyamide blast media can cause explosive dust, the shot blast machines were equipped with special, ATEX-compliant filter systems. Fully automatic and sustainable de-flashing of single work pieces The swing satellite table machine RWS 1200 was installed to increase the shot blasting capacity at the plant in Ummerstadt. It is used for de-flashing components made from PPS-GF and outer dimensions of up to 163 mm. In line with the production cycle of the injection molding machine up to four work pieces are de-flashed simultaneously within a processing time of 40 seconds. The RWS 1200 has two chambers, equipped with four rotary satellite stations per chamber and each satellite holding one work piece. This clever design allows to unload/load work pieces in one chamber, while the work pieces in the other chamber are processed. Unproductive idle times are, therefore, minimized. One energy-efficient blast turbine throws the media onto the work pieces placed on the rotary satellite stations arranged in the shape of a diamond. The satellites are not only rotating but, depending on the work piece geometry, can also be stopped at a certain angle. Work piece areas that cannot be reached by the media thrown by the turbine, are cleaned with special air blast nozzles. This suction air blast system is equipped with pressure control and a vertically moveable nozzle holder ensuring precise de-flashing. In addition to the vertical movement a linear positioning system allows to place the nozzles precisely in front of the work pieces. The nozzles are working in either oscillating or static mode. „To minimize the usage of compressed air, we are working with work piece specific PLC processing programs“, concludes Jürgen Bär. The RWS 1200 is also equipped with automatic replenishment devices for the blast media and the anti-static compound, an air extraction unit for the blast chamber and a blast media cleaning system. The family enterprise ROS Since 1926 the family enterprise ROS GmbH & Co. KG has been known for precision in plastic components. For more than 90 years leading companies in the automotive, medical engineering, electrical and other industries have placed their trust in this specialist for plastic components and its products. With around 300 employees at two locations in Northern Bavaria and Southern Thuringia the company designs and builds high-precision tools for processing high-performance plastic materials in its own tool-making shop. This guarantees that the functional components produced with these tools are of an extremely high quality.

Mass Finishing Work Piece Handling Series, Part 3 – Maintaining Wear Linings

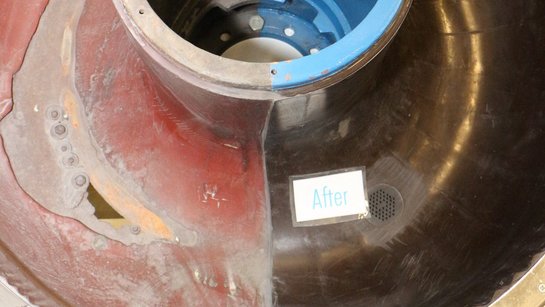
Adequate wear linings are an important factor in ensuring work pieces are efficiently handled in a mass finishing machine. Along with the method speed of transfer as well as the media selection and separation, the condition of a machine’s wear lining factors into the quality of process results. Thick linings assist with work piece handling by providing a cushioning effect, yet thin or damaged wear linings allow unwanted knicks, scratches, and dings. With more than 80 years of expertise in surface finishing, Rosler can assist with all aspects of your mass finishing process including proactively eliminating potential work piece handling issues. Observing Machine Conditions Regularly checking the lining of your work bowl(s) and trough(s) for wear is one way to ensure parts don’t get accidentally damaged during processing. Inspecting linings consistently will help identify repairable issues before permanent damage to the machine occurs. To effectively finish work pieces, media must be matched to the specific finishing task and the initial state of a work piece. For example, media used for deburring/edge radiusing and surface grinding can be very abrasive. If not properly protected by a suitable wear lining, the steel construction of a work bowl would be completely worn through in a few hours by contact with the media and work pieces. Polyurethane and, to a certain degree, rubber are excellent lining materials providing wear protection for thousands of operating hours. Even these materials wear through and must be periodically replaced with a new lining. Small areas can be temporarily patched with Polyurethane Repair Kits until the unit can be removed and professionally relined. If a reline is required, only use a qualified reline supplier such as the lining shop at Rosler. Relines are available in different degrees of hardness (shore A) and different qualities. Always make sure that the lining material is suitable for your specific mass finishing process. More information about specifying liner materials is available in a previous blog post . Side-by-side comparison of a vibratory bowl before and after relining Maintaining Process Stability Checking your work bowl lining for wear and replacing it in a timely manner is essential for the stability of your mass finishing process as a whole. In addition to worn work bowls, failure to ensure a proper protective lining can create other problems including: Work pieces getting stuck in the machine and, therefore, jeopardizing the integrity of different work piece batches. Media, water, and process chemicals can leak from the machine if the metal processing bowl is worn through and holes or cracks appear. Severe machine malfunction can occur when media or parts can get trapped in worn spots during the separation phase when the finished work pieces are separated from the media. Damage to the work bowl that is beyond repair, causing unnecessary downtime and requiring costly replacement parts. A weakened bowl can crack and make the entire machine unusable. Check your bowl lining at least monthly for wear or rips. The areas around drains, the parts loading chute, and around the unload areas will see the highest wear and are especially crucial. The “nail test” makes checking the liner thickness easy. Push a nail through the liner until you hit the base metal and record the thickness of the liner. Keep track of the liner thickness over time to predict when you will need to replace your liner. Most liners are between 5/8 and 1 in (15-25 mm) thick. Plan to get your machine relined when the thinnest part of your liner is less than 1/4 in (6 mm) thick. Just as optimal media mix must be regularly monitored, so must the condition of a work bowl. If not, the entire process and downstream operations may suffer. The Rosler Way Maintaining adequate wear linings protects your work pieces, equipment, and overall mass finishing process. Contact us for mass finishing expertise and insight. The complete Mass Finishing Work Piece Series includes: Part 1 – Selecting the Best Work Piece/Media Separation Method . Part 2 – Preventing Drop Height Damage . Part 3 – Maintaining Wear Linings .