Solution Finder
SOLUTION FINDER

Su guía a través del
mundo de productos Rösler

Con unos pocos clics encontrará la máquina adecuada a sus necesidades.

Resultados: 237 Artículo - 51 Productos

Custom-engineered roller conveyor blast machine brings about considerable capacity expansion

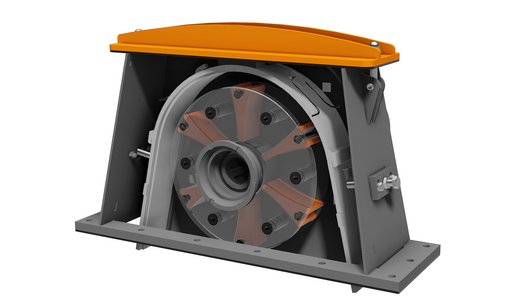
Heidemann Stahl- & Montagebau und BHS Sandstrahltechnik GdR zählen dank ihrer 30-jährigen Erfahrung auf dem Gebiet des Stahlbaus zu den absoluten Experten. Dabei realisiert das Unternehmen aus Volkmarsen bundesweit Projekte für Industrie, Handel, Gewerbe und Landwirtschaft. Ob Hallenbau, Bühnen- oder Brückenkonstruktionen, Geländer oder Tribünen - die individuellen Stahlbaulösungen müssen höchsten Ansprüchen an Wirtschaftlichkeit und Qualität genügen. Dementsprechend bemisst sich auch die Erwartungshaltung der Kunden an die konstante Qualität der Stahlprodukte. Kapazitätserweiterung beim Entzundern, Entrosten und Reinigen Um die stetig wachsende Nachfrage aus der Stahlindustrie bedienen zu können, reichen die Kapazitäten der bestehenden Strahlanlage nicht aus. „Unsere aktuelle Strahlanlage ist nur 2 Meter breit, mit der Kapazitätserweiterung auf 2,5 Meter erhoffen wir uns als Dienstleister eine deutliche Steigerung des Durchsatzes. Entscheidend für uns ist die Leistungsfähigkeit, Qualität und Langlebigkeit der Anlage“, fasst Peter Heidemann, Geschäftsführer von BHS Sandstrahltechnik, die Anforderungen zusammen. Die räumliche Begrenzung vor Ort war eine zusätzliche Herausforderung die Rösler mit langjähriger Erfahrung und Know-how löste. Kompakt, vielseitig, individuell – Rollenbahnstrahlanlage RRB 27/6-HD-So „ Rösler Rollenbahnstrahlanlage RRB 27/6-HD-SO wurde eigens auf unsere speziellen Anforderungen angepasst“, berichtet Peter Heidemann. Eine dieser Anpassungen ermöglichte die Realisation maßgeblich. Mit einer Gesamthöhe von nur 4.800 mm passte sich die Rollenbahnstrahlanlage, speziell konstruiert in Niedrigbauweise, optimal den räumlichen Gegebenheiten an. Um das geforderte Strahlergebnis des Reinheitsgrades SA 2,5 prozesssicher zu erzielen, ist die Strahlanlage mit insgesamt sechs Gamma 400 G Turbinen im Y-Design und einer Antriebsleistung von je 22 kW ausgestattet. Diese speziell, von Rösler entwickelte Turbinentechnik, zeichnet sich vor allem durch ihre Verschleißresistenz, Wartungsfreundlichkeit und Effizienz aus. Die Gamma Turbinen aus geschmiedetem Werkzeugstahl glänzen nicht nur mit dem Dreifachen an Standzeit, sondern erzielen im Vergleich zu herkömmlichen Turbinen eine bis zu 20 Prozent höhere Strahlleistung bei geringerem Energieverbrauch. Die strömungsoptimierten Wurfschaufeln im Y-Design können schnell und unkompliziert bei Verschleiß gedreht werden. Durch eine zweifache Verwendbarkeit bringen die Rösler-Turbinen ein enormes Einsparpotential im Hinblick auf Ersatzteilkosten mit sich, gleichzeitig reduziert sich der Maschinenstillstand. Eine, serienmäßig aus Manganstahl gefertigte Strahlkammer, mit zusätzlich auswechselbaren Manganstahl-Platten steigert die Anlagenverfügbarkeit um ein Weiteres. Durch die innovative Strahlkammergeometrie reduziert sich der Platzbedarf. Lediglich zwei, in der Strahlkammer angeordnete Rollen aus gehärtetem Werkzeugstahl sorgen für einen optimalen Werkstücktransport und senken die Verschleißkosten zusätzlich. Mit individuellem Konzept überzeugt „Mit dieser speziell für unsere Bedürfnisse ausgelegten Strahlanlage bin ich optimistisch, dass wir unsere Strahlqualität maßgeblich verbessern können, was letztendlich sowohl zu einer Qualitätssteigerung unserer Produkte sowie zu einer Erhöhung der Produktivität unseres Gesamtvolumens führen wird“, erklärt Peter Heidemann, Geschäftsführer von BHS Sandstrahltechnik und ergänzt: „Die Firma Rösler ist auch zukünftig unser erster Ansprechpartner für Strahltechnik. Wir schätzen in der guten Zusammenarbeit vor allem die technische Expertise und individuelle Beratung“.

Ausbildungsstart in Zeiten von Corona: Rösler Oberflächentechnik begrüßt 16 neue Auszubildende

Trotz der anhaltenden Corona-Pandemie und der damit einhergehenden wirtschaftlich angespannten Situation hält Rösler auch in diesem Jahr an seiner hohen Ausbildungsquote fest. „Das Prinzip der dualen Ausbildung ist eine der bedeutendsten Säulen für junge Berufseinsteiger“, betont Ausbildungsleiterin Anja Süppel und ergänzt „gerade in der aktuellen Situation ist eine zukunftsorientierte Ausbildung mit Qualität und Struktur gefragt“. Als inhabergeführtes Familienunternehmen ermöglicht Rösler den Berufsstartern einen professionellen Start ins Berufsleben und vermittelt während der Ausbildung sowohl fachliche Kenntnisse als auch die Möglichkeit, ihre Talente und Ideen zu entfalten sowie vielfältige Kompetenzen zu erlernen. Der Ausbildungsstart beginnt am 1. September 2020 wie immer mit einem Begrüßungstag in Memmelsdorf – dieses Jahr unter der Einhaltung der geltenden Hygiene- und Abstandsregeln. In den folgenden Tagen verschaffen die Projekttage den Berufsstartern erste Einblicke in die wichtigsten Geschäftsbereiche des Unternehmens und bieten zudem die Möglichkeit, sich untereinander besser kennenzulernen. Dabei treffen sie in Memmelsdorf und Hausen auf engagierte Kollegen und Fachausbilder sowie auf modern eingerichtete Schulungs- und Ausbildungsräume. Auch 2021 hat das Familienunternehmen Rösler wieder Ausbildungsplätze zu besetzen. Das vielfältige Ausbildungsangebot beim Spezialisten für Oberflächentechnik reicht von unterschiedlichen Berufen des technisch-gewerblichen über den kaufmännischen Bereich bis hin zu dualen Studienangeboten. Ein Indikator, dass sowohl die Qualität als auch die Rahmenbedingungen in der Ausbildung bei Rösler passen, sind die hervorragenden Ergebnisse bei den letztjährigen Abschlussprüfungen. Die Rösler-Gruppe bietet für das Jahr 2021 folgende Ausbildungsplätze an: Industriekaufleute, Chemielaboranten, Technische Produktdesigner, Konstruktionsmechaniker, Industriemechaniker, Fachkräfte für Metalltechnik, Mechatroniker, Elektroniker für Betriebstechnik, Fachkräfte für Lagerlogistik. Ein dualer Studiengang ist möglich im Bereich Wirtschaftsingenieurwesen, Wirtschaftsinformatik und Elektrotechnik.Die Partnerhochschule von Rösler ist die Duale Hochschule Mosbach in Baden-Württemberg. Online-Bewerbung sind möglich über die Internetseite: www.rosler.com Bei Fragen zu Ausbildung/Dualem Studium gibt Anja Süppel gerne Infos unter Tel.: +49 9533 / 924-442 oder per E-Mail an: a.sueppel@rosler.com

Forge & Foundry, Part 12 – Media and Compound Selection, Effluent Handling Drive Success

Regardless of the industry , the selection of media and compounds utilized in mass finishing can elevate or hinder finishing results. The handling of effluents – used process water – also factors into a process’ efficiency and end results. With more than 80 years of experience, Rosler understands the demands of the forge and foundry industries specifically and how to achieve precise and consistent finishing results by combining the latest technology, well-designed machines, and consumables . This installment of the Forge & Foundry Blog Series highlights how careful media and compound selection along with proactive handling of effluents assist in producing mass finishing efficiencies. Ingredients for Success Media and compounds are more than just “rocks” and “soap” thrown into a mass finishing machine. Instead, these consumables are sophisticated tools that can make a mass finishing process a success or a failure. Media choice with regard to shape, size, composition, and abrasiveness is as important as selecting the right machine. Selecting the wrong media could be detrimental to the process. The level of media in a machine is equally important. If not introduced in the prescribed ratio, even the best suited media will fail to deliver the desired results. For example, increasing the ratio of media relative to the work pieces has a cushioning effect and helps prevent unwanted work piece damage in the form of nicking. Conversely, skimping on media levels can produce ineffective finishing as well as work piece damage. Much like media, the compound selection must match the work piece material. For example, aluminum die-castings require a different compound than die-castings made from magnesium. Applying compounds in the prescribed dosage is also key to maintaining finishing results. For example, insufficient compound usage can cause foaming in the machine and discoloration of finished work pieces. Handled with Care Mass finishing produces an effluent containing media and metal fines, various chemicals from the compounds, and sometimes even chelated metals. At this point a decision must be made; will the effluent be cleaned and recirculated or discharged as waste? In either case, contaminants must be removed first. When discharging as waste, all contaminants must be removed to prevent pollution issues and discharge fines. Additional mass finishing process efficiency and greater ROI can be attained by cleaning effluent for reuse. The use of centrifugal filters is an excellent treatment method for effluent which factors in added benefits including reduced water usage and compound longevity. Rosler Centrifuge Technology By removing all solids in the form of media and metal fines from the mass finishing effluent, centrifuges allow the cleaned liquid, now free of any solids, to be reused by recycling it back to the mass finishing machine. This can result in water consumption savings of more than 90 percent. Since centrifuges do not degrade the compound in the process liquid, drastically reduced usage of compounds may also be achieved. The Rosler Way Whether you need help selecting a whole mass finishing system or the consumables used within it, the Rosler team can help. Our motto of “finding a better way…” applies to big picture thinking and day-to-day machine operations. Contact us to share your needs so we can develop a solution. The complete Forge & Foundry Series includes: Part 1 – Shot Blasting Systems. Part 2 – Efficient Recycling. Part 3 – Shot Blasting & Sand Castings. Part 4 – Selecting a Shot Blasting Machine for Sand Castings. Part 5 – Cleaning Features & Dust Precautions for Sand Castings. Part 6 – Selecting a Shot Blasting Machine for Die Castings. Part 7 – Selecting a Shot Blasting Machine for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 8 – Frequently Used Shot Blasting Machines for Sand Castings. Part 9 – Frequently Used Shot Blasting Machines for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 10 – Shot Blasting Machines Commonly Used for Die Castings. Part 11 – Top Mass Finishing machines for Cleaning Die Castings Part 12 – Media and Compound Selection, Effluent Handling Drive Success Sign up for enews alerts to be notified of all Rosler blog posts! https://vimeo.com/467660633
Mit dem neuen Dosiersystem von Rösler gesetzeskonform arbeiten

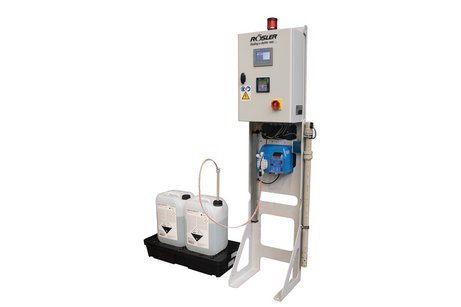
In der im August 2017 in Kraft getretenen 42. Bundesimmissionsschutzverordnung (42. BImSchV) werden vom Gesetzgeber Maßnahmen vorgeschrieben, um die Bildung von gesundheitsgefährdenden Legionellen-Stämmen zu verhindern. Dies betrifft auch das Betreiben von Nassfilter. Die Verordnung verpflichtet u. a. alle Betreiber von Nassabscheidern, regelmäßig aufwendige Prüfungen und Laboruntersuchungen auf Legionellen-Befall durchzuführen und zu dokumentieren. Bei Unterlassung drohen erhebliche Strafen. Unsere Lösung: Auf Grund unserer langjährigen Erfahrung im Umgang mit Prozesswasser, haben wir für alle Nassabscheider ein System entwickelt, dass die Entstehung von Legionellen gänzlich verhindert. Durch Einsatz unserer neuen Dosiereinheit RDS-pH 10/25 in Kombination mit unserem Verfahrensmittel Additiv RST-P1 wird der pH-Wert des Nutzwassers dauerhaft über 10 gehalten. Dies wird automatisch dokumentiert. Das Entstehen von Legionellen wird dadurch im Vorfeld verhindert, Laboruntersuchungen können entfallen und gesetzliche Vorgaben werden zu 100 % erfüllt. Ihr Nutzen: Das Entstehen von gesundheitsgefährdenden Legionellen-Stämmen wird auf einfache Weise verhindert Kosten und Aufwand für Laboruntersuchungen entfallen Vermeidung von hohen Ausfallkosten durch eine notwendige Anlagenreinigung nach einem möglichen Legionellen-Befall Automatische Protokollierung des pH-Wertes im Nutzwasser in ein Betriebstagebuch Geringer Überwachungs- und Wartungsaufwand Kein Aufwand bei Stilllegung zur Urlaubszeit sowie bei der Wiederinbetriebnahme danach Wir beraten Sie gerne weiter. Sie erreichen uns unter der +49 9533 924-333 oder per E-Mail: service-de@rosler.com .

Rösler cleaning centrifuge in the glass industry reduces costs by 90%

Easy operation thanks to fully automatic processing The automatic RZ 150 A is designed to handle a throughput of 150 liters per minute. In conventional systems the peeling knife, driven by a gear motor, is constantly rotating with the drum. In contrast to this the peeling knife of the Rösler RZ 150 A, located in the center of the sludge drum, is stationary. Only when the sludge deposits in the drum must be discharged, is the peeling knife moving towards the drum wall with a pneumatically actuated linear guide system. This allows peeling the sludge from the drum wall without placing any additional load on the drum bearings. After completion of the peeling cycle the drum is automatically rinsed to remove any residual sludge deposits. This prevents imbalances during the subsequent cleaning cycle, which could lead to premature wear of the drum bearing. The fully automatic process helps saving costs and reduces the consumption of valuable resources. Mr. Stepa, general manager of HART-SM, explains: „The new cleaning centrifuges helped us to reduce our energy consumption and achieve substantial cost savings. For example, we could reduce our idle machine times by 90 percent. And since only the water losses due to evaporation must be replenished, we could significantly reduce the costs for water exchanges. Last-but-not-least, we could reduce the monthly consumption of coolant from about 1,500 liters down to 150 liters, a reduction by nearly 90 percent. In addition to the considerable financial and technical benefits we also achieved a significant improvement of the water quality, an important factor for us as a progressive, future-oriented company. The water system is clean, because it is no longer overloaded with calcium. As a matter of fact, it is totally free of solid particles, which has an extremely positive effect on the overall quality of our products.” Mr. Stepa continues: “The cleaning centrifuge from Rösler represents an innovative solution that brings about a significant added value to our operation. And, of course, it is perfectly in line with our vision for a clean environment. We are pleased to have a company like Rösler as our reliable partner!” Rösler cleaning centrifuges – efficient and effective cleaning of industrial liquids Whether a company has to deal with coolants, sludge from paint processes, the water from industrial work piece cleaning operations or other process liquids, the treatment of the contaminated liquids always depends on the quality of the applied cleaning technology. No doubt the innovative, well-designed centrifugal filtering technology from Rösler offers excellent solutions. To achieve optimum cleaning results for the various industrial liquids, the centrifugal systems are specially adapted to the individual customer requirements. The Rösler centrifuges offer not only numerous technical and financial benefits, but through significant savings of water and other production materials they also help protect the environment. With decades of experience in the field of centrifuges Rösler is a competent, qualified partner for the efficient, energy-saving cleaning of all kinds of industrial liquids.

Mass Finishing Success Requires Constant Operational Focus

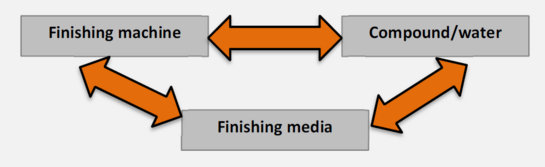
When most companies take on capital expenditure projects such as purchasing mass finishing equipment, very careful attention is paid to investing in the most productive, cost‐efficient equipment as possible to achieve the best possible quality. Operational efficiency is often another story. Once the equipment is up and running routine takes over and less attention is paid to keeping the equipment operating at its peak performance. Whether the machinery is never calibrated to reach its fullest potential or the on-going process is not carefully monitored once the process is dialed in, lacking operational focus can be costly and counterproductive. Figuratively speaking, poorly managed mass finishing operations are pouring money down the drain! Rosler works with its clients to ensure that our machinery delivers initial success and continues to provide precise, repeatable results long into the future by promoting operational attention and heading off costly mistakes. Consequences of Inattention For mass finishing processes, the lack of operational focus may take many forms individually or simultaneously, including: Reduced capacity because of processing times becoming unnecessarily longer. Overall poorer finishing qualities. Unstable processes with erratic finishing. Work pieces requiring additional reprocessing and higher rejection rates. Equipment not providing expected results and return on investment. Such operational deficiencies can cost a lot of money in the short-term when it comes to meeting client expectations and standards as well as the long-term life expectancy and usefulness of the process and machinery utilized. Identifying Issues and Opportunities Careful monitoring of the key process parameters, quick correction of any process abnormalities or “trouble shooting,” and regular preventive maintenance will ensure that a finishing process runs as intended in a cost‐efficient manner. Of course, this should not prevent a company from looking for further improvement and optimizing its current finishing operation. Technical upgrades or new, improved media and/or compounds may have become available for existing equipment which could help increase productivity, reduce costs, and improve the finishing quality. When working with a trusted partner and mass finishing expert such as Rosler, upgrades and advances can often be implemented without completely overhauling a process or purchasing entirely new systems. Optimizing Mass Finishing Operations Achieving the best results from a mass finishing process requires understanding the interaction between the various process components, including: The finishing machine itself. Compounds (liquids, recycling, powder, grinding, polishing, dry polishing, and cleaning/degreasing) and process water. Media – whether ceramic , plastic , or polishing and drying . The success of mass finishing depends on the successful pairing of machines, media, and compounds/water. The desired finishing results – deburring, edge radiusing, cleaning (de‐oiling, descaling) , and surface smoothing and/or polishing – can only be achieved if these process components are carefully calibrated with each other. More than a dozen factors are in play in a mass finishing process and enough complexity to warrant involving experts with experience. Process water from the finishing machine must also be addressed and monitored for optimum results. Depending upon the work piece’s material and original condition as well as the processes performed and consumables used, process water may be contaminated with media and metal fines, chemicals from the compounds, and even chelated metals. Before the process water can be discharged to drain or re‐used in the finishing process, it must be cleaned with a centrifuge . The Rosler Way With more than 80 years of experience, the Rosler team and worldwide Rosler Group have the knowledge and expertise to help you optimize your mass finishing process throughout the machine’s life cycle. Whether you have our equipment or a competitor’s, contact us for advice, sales, and service.

Automation Part 7 – The Top 3 Mass Finishing and Shot Blasting Machines

Rosler understands that automating aspects of your mass finishing and shot blasting processes has never been more critical. As we have learned during recent world events, outside factors can have a significant impact on your ability to maintain a largely manual process. Though automated mass finishing and shot blasting machinery does require some human intervention, it can often be operated with a minimal headcount and limited human contact. In previous blogs, we have explored how an automated-first posture can help you to gain significant efficiencies, lower costs, and increase your competitive advantage. We have also looked at the balance between automation and the environment and have discussed ways that you can mitigate environmental impacts of operating automated mass finishing and shot blasting machinery. We now conclude our Automation Blog Series with best practice examples of automated mass finishing and shot blasting machines Rosler offers and the associated accessories and components available to help in building your next-generation automated processes. Mass Finishing Automated Dual Rosler Drag Finishing Systems for Tool Bodies This drag finishing system is particularly useful for finishing of milling tool holders where work pieces are de-oiled, deburred, smoothed, and polished. Work stations equipped with drag finishing equipment feature special quick-connect couplings to expedite the work of robots to load and unload work pieces. Automated Dual Rosler Drag Finishing System pictogram As seen in the pictogram, a robot picks up the work pieces from a staging pallet and transfers them to the first R 6/1000 SF machine in a precise location with an accuracy of 4/1000 th of an inch (= 0.1 mm). Work pieces are then moved to a second R 6/1000 SF for smoothing and polishing before the robot moves pieces to a second staging pallet upon completion. Automated R 6/1000 SF Drag Finishing System This fully automated process is complemented by the Rosler Z1000 centrifuge for water cleaning and recycling. In order for precise finishing results, the work surface must be smooth, clean, and free of nicking and scratching. Walter Tools CNC milling cutter head processed by the Rosler Dual Drag Finishing System 2. Linked Dual Rosler Centrifugal Disk Finishing Systems Also known as the FKS 15.1 A2 , this system is used in the finishing of special stampings with a focus on the de-oiling, deburring, and edge radiusing of disk springs, rings, and washers. An example of work pieces processed by the Rosler Automated FKS System With a fully automated operation, the system handles the complete loading, unloading, transporting, washing, and drying of parts and media mixes – concluding with the backfilling of the finished parts into waiting bins. Linked Dual Rosler Centrifugal Disk Finishing System pictogram This process ensures batch integrity as long as individual batches are not mixed up in the screening machine and are completely oil-free with a defined edge radius prior to entering the machine. Automated FKS System also known as a Linked Dual Centrifugal Disk Finishing System 3. Rosler Linear Continuous Flow Vibratory Systems for Metal Parts Rosler’s linear continuous flow vibratory systems manage the de-oiling and deburring process for a wide variety of stampings. Work Pieces processed by a Rosler Linear Continuous Flow Vibratory System In the example below, parts are dumped en masse into the vibratory feed hopper by a forklift equipped with a fork rotator. The machine then places the empty part bin behind the hot air drier while the work pieces progress through the system in a fully automated manner. Rosler Linear Continuous Flow Vibratory System pictogram Batches must be processed separately, and parts must be free of oil for maximum throughput. Automated Rosler In-line DA System with parts loader and dryer Shot Blasting Rosler RROB Roboblaster for Cylinder Heads Rosler RROB Roboblaster with parts transportation system Able to precisely clean, de-sand, and deburr cast aluminum components, Rosler’s RROB Roboblaster is ideal for cylinder heads. Cylinder head processed by the Rosler RROB Roboblaster Its process begins when raw cylinder head castings are staged on two roller conveyors connected with a 90-degree turntable. Next, a robot equipped with a rotating device selects individual castings and suspends them into the machine. As the robot rotates the raw cylinder head, the blasting process takes place on all exposed surfaces. Finally, the robot places the finished cylinder heads into a screen drum for shaking out of residual blast media. Rosler RROB Roboblaster pictogram 2. Rosler RMBC 8.2 Tumblast Machine for Forged Components Part of Rosler’s Tumblast offerings, the RMBC 8.2 machine is particularly useful in descaling a wide variety of different forgings, including high volumes of bevel gears, in preparation for machining. Work pieces processed by the Rosler RMBC 8.2 Tumblast Machine An operator places two bins with raw parts into the skip loader after which empty bins are placed on a chain conveyor. Following shot blasting within the machine, finished parts are dumped onto a vibratory hopper, which tumbles, then automatically returns the finished parts into the waiting bins on the chain conveyor. Rosler RMBC 8.2 Tumblast Machine pictogram As with other automated machinery, it is critical to load distinct batches individually and to ensure the parts are free of scale. Rosler Automated RMBC 8.2 Tumble Belt Blast System with parts loading and unloading 3. Rosler RKWS 3 x 4 for Blast Cleaning of Crankshafts Rosler Automated RWKS 3 x 4 Cranksaft Blaster with robotic parts loading This particular model of the RKWS shot blast machine is equipped with three blast chambers arranged in a circle; each chamber is outfitted with four Gamma G blast turbines to accomplish the descaling process for crankshafts and other work pieces. Crankshafts before and after processing by RKWS A robot handles the loading and unloading of the parts, making this process fully automated. It’s important to note that piece weight is limited to a minimum of 14 lbs (6 kg) and maximum of 40 lbs (18 kg); after blasting the surface must be Sa 3 (white metal, no remaining traces of mill scale or rust allowed). Rosler Automated RWKS 3 x 4 Cranksaft Blaster with robotic parts loading https://vimeo.com/467660633 The Rosler Way By appropriately outfitting your operation with the right selection of automated mass finishing and shot blasting systems, you can be assured of gaining efficiencies and benefits that will help you maintain your competitive advantage. At Rosler, more than eight decades of experience and a constant drive to harness the latest advances allow us to design and manufacture innovative mass finishing and shot blasting solutions to fit your unique needs. Contact us today to learn how we can improve and automate your finishing system. The complete Automation Series includes: Part 1 – How Robots are Improving Mass Finishing and Shot Blasting Processes. Part 2 – Why Automation is Beneficial for Your Business. Part 3 – What Problems Do You Want to Solve? Part 4 – How Do I Select the Right Machine and Consumables? Part 5 – What Automation Hardware is Available? Part 6 – Environmental Considerations of Automation. Part 7 – The Top 3 Mass Finishing and Shot Blasting Machines. Sign up for enews alerts to be notified of all Rosler blog posts!

New Vibratory Finishing System Enhances Existing Material Handling & Drying Equipment

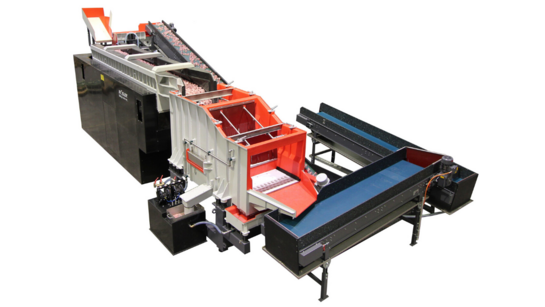
When it comes to high-volume production of complex aluminum die-castings, Kovolis Hedvikov a.s. (Kovolis) is a sought after partner by numerous car manufacturers and their suppliers. To expand its capacity and achieve more flexibility in the overall manufacturing process, the company purchased a continuous flow vibratory finishing system from Rosler designed to handle a wide work piece spectrum and custom engineered to fit into the available space at the customer’s premises. About Kovolis Founded in 1816 as an ironworking operation, Kovolis has focused entirely on aluminum die casting since 1945. Today, Kovolis produces components from nine different aluminum alloys weighing between 7 oz (200 grams) and 18 lbs (8 kg) with different casting technologies including vacuum investment casting and rheocasting. Their product range includes brakes, power steering systems, turbo chargers, and compressors for air conditioning systems. Kovolis customers are renowned car manufacturers and tier-1 suppliers that also utilize the company as an important partner for product development, machining, heat treatment, and surface finishing services. New Needs Call for a New System Jiri Buzek, manager of foundry III at Kovolis, explained the need for a new vibratory finishing system. “Our product portfolio underwent a drastic change in the past years. The trend goes more and more to larger and more delicate components, which require a vibratory finishing step after punch deburring for their downstream handling. Our existing finishing system was not designed for this and had also reached the end of its productive service life.” The new system not only had to cope with larger work pieces, but the finishing process also had to be a lot gentler. Additional customer requirements were high equipment uptimes and cost efficiency. And, above all, the new finishing system had to be integrated into the existing manufacturing operation, utilizing the existing work piece loading device and hot air belt drier. The planning engineers at Kovolis submitted these specifications to two German equipment suppliers. “We decided to go with the Rosler continuous feed vibratory finishing system, because it offers ample capacity, and Rosler met all our special technical requirements. Of course, the fact that our company has had excellent experience with other equipment from the same supplier certainly helped,” Buzek said. The single curve U-shaped cross section of the processing channel guarantees the optimum movement of the media and work pieces through the machine. Kovolis also appreciates that Rosler can supply the equipment as well as all compounds and finishing media needed. This allows the perfect adaptation of the finishing process to the customer’s work pieces. A Customized Solution The new finishing system consists of a linear continuous feed machine, type R 550/4600 DA, with a usable length of 15 ft (4.6 m). The functions of the existing work piece loading system and hot air belt drier were integrated into the overall system controls. “Rosler met all our technical requirements and provided valuable support in optimizing our finishing process,” Buzek said. The system offers a number of features and capabilities, including: Fully automatic feeding of the work pieces every 30 seconds. Accommodation of parts with diameters of up to 16 in (400mm). Adjustable processing times. Dual-stage separation with rinsing station. Process water cleaning with an automatic centrifuge. The processing bowl angle can be adjusted to change the processing time. Kovolis was especially impressed with the centrifuge technology Rosler offers. “In the past we cleaned our process water chemically or with a semi-automatic centrifuge. This was highly labor intensive and costly” Buzek said. “With respect to process water-cleaning, Rosler provided us again with the optimum solution. “We are certain that with the new equipment we will not only improve the quality of our finishing operation but, at the same time, will become more cost efficient.” The Rosler Way As the international market leader, Rosler offers total solutions in the field of mass finishing and shot blasting, painting and preservation systems, and mass finishing consumables. In addition, Rosler offers a broad spectrum of surface finishing technologies (deburring, descaling, desanding, polishing, surface grinding, etc.) for work pieces made from metal and other materials. Headquartered in Germany, the Rosler Group maintains sales and manufacturing branches in Great Britain, France, Italy, the Netherlands, Belgium, Austria, Serbia, Switzerland, Spain, Romania, Russia, Brazil, India, China, and the United States. Contact us to discuss how we can provide a customized solution to solve your unique challenges.

Forge & Foundry, Part 11 – Top Mass Finishing Machines for Cleaning Die Castings

Rosler Metal Finishing has decades of experience in the forge and foundry industries, especially when it comes to mass finishing for die-casted work pieces. Our Forge & Foundry Blog Series continues with an overview of our top five mass finishing machines for precise cleaning of die castings. Standard Rotary Vibrators Media and parts are placed into a circular processing bowl in standard rotary vibrators . The energy from a vibratory motor causes the media and parts to freely tumble over each other. Some models are equipped with an internal separation device for separating the finished work pieces from the media. Rotary vibrators can be used for batch and continuous feed processing. The R620 Euro is one of Rosler's standard rotary vibrator models Rosler’s standard rotary vibrator models include the models EC, Euro, A, and R. Ideal Work Pieces — Small to fist-sized die-castings such as shoe buckles, furniture fittings, gear shifter forks, electrical components Work pieces processed by one of Rosler's standard rotary vibrators Learn more about these machines in our Rotary Vibrator Guidebook (PDF) . Long Radius Rotary Vibrators Built upon the rotary vibrator technology, long radius machines feature much bigger overall diameter and larger processing bowls. The expanded processing area allows for considerably longer cycle times in continuous feed mode. Known as the LR models at Rosler, these machines allow for batch and continuous feed processing. Rosler's LR models are long radius rotary vibrator machines Ideal Work Pieces — Small- to mid-sized die-castings including small gear boxes, bearing housings, mirror frames for cars, all kinds of engine and transmission components Work pieces processed by one of Rosler's long radius rotary vibrators Learn more about Rosler’s LR capabilities in our Long Radius Guidebook (PDF) . Multi-Channel, Continuous Flow Rotary Vibrators The major difference between a multi-channel, continuous flow rotary vibrator and a standard rotary vibrator is the processing channel’s spiral arrangement to create extremely long processing channels of up to 31 ft (9.5 m). The unique channel design draws work pieces apart so they almost never touch each other during the finishing process and always features continuous feed processing. Rosler’s linear, continuous flow vibrators are known as the SE models. The Rosler SE model is a multi-channel rotary vibrator Ideal Work Pieces — Small to mid-sized somewhat delicate components, particularly parts with critical sealing areas that must not be damaged including parts for espresso machines and model train cars Model train cars processed by one of Rosler's Multi-channel continuous flow rotary vibrators machines More information is available in our Multi-Channel Continuous Flow Systems Guidebook (PDF) . Linear, Continuous Flow Vibrators Powerful vibratory drive systems are mounted underneath rectangular processing bowls in linear, continuous flow vibrators. They always feature continuous feed processing. Known as DA models at Rosler, these machines are the largest and most powerful mass finishing machines available. Rosler's linear continuous flow vibrator machine offerings include this DA 650 6600 Ideal Work Pieces — Mid-sized to large, somewhat sturdy, die-castings that are not damaged by tumbling over each other including power drill housings, cylinder head covers, oil pans, transmission housings, disks for automatic transmissions Impact wrench housings processed by one of Rosler's linear continuous-flow vibrators Learn about Rosler’s DA capabilities in our Linear, Continuous Feed Systems Guidebook (PDF) . Tub Vibrators Similar to linear, continuous flow vibrators, tub vibrators feature rectangular processing bowls with a powerful vibratory drive system mounted underneath. Tub vibrators are available in a wide range of sizes from very small to extra large, allowing the processing of a wide work piece spectrum, from small to very large, up to 10 ft (3 m) long and 5 ft (1.5 m) wide. Rosler offers several tub vibrator models including the TE, Compact TE, TSD, TU, TUD, TUM, and RMO, all of which feature batch processing. The Rosler TUM is one of Rosler's tub vibrator machine offerings Ideal Work Pieces — Large housings, large light casings, structural airframe parts, or smaller parts in low to medium production volumes A large die cast cover processed in one of Rosler's tub vibrators Learn more about Rosler’s various tub vibrator models and capabilities in our Tub Vibrators Guidebook (PDF) . The Rosler Way The Rosler team is uniquely capable to solve mass finishing challenges, especially when it comes to die castings. Contact us to share your needs so we can develop a solution. The complete Forge & Foundry Series includes: Part 1 – Shot Blasting Systems. Part 2 – Efficient Recycling. Part 3 – Shot Blasting & Sand Castings. Part 4 – Selecting a Shot Blasting Machine for Sand Castings. Part 5 – Cleaning Features & Dust Precautions for Sand Castings. Part 6 – Selecting a Shot Blasting Machine for Die Castings. Part 7 – Selecting a Shot Blasting Machine for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 8 – Frequently Used Shot Blasting Machines for Sand Castings. Part 9 – Frequently Used Shot Blasting Machines for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 10 – Shot Blasting Machines Commonly Used for Die Castings. Part 11 – Top Mass Finishing machines for Cleaning Die Castings Part 12 – Media and Compound Selection, Effluent Handling Drive Success Sign up for enews alerts to be notified of all Rosler blog posts!

Automation, Part 6—Environmental Considerations of Automation

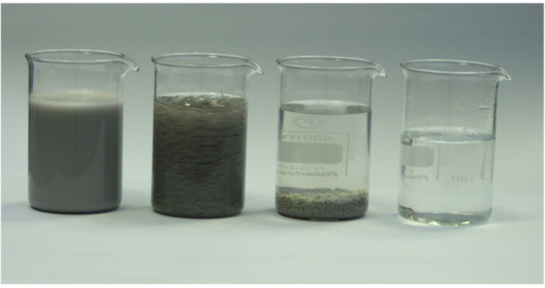
Technology has transformed almost every aspect of life and the shop floor is no exception. As explored in previous Automation Blog Series posts, Rosler Metal Finishing believes automation represents the new norm in mass finishing and shot blasting . In the face of increasing competition, manufacturing interests will continue to demand lower cost, higher efficiency, and greater flexibility from their chosen surface finishing partner. Though it would appear that any downsides of automation are outweighed by its benefits, there’s a delicate balance to be struck when it comes to a symbiotic relationship with the world outside of the machine. Having previously discussed how human effort and ingenuity will work in harmony with automated processes, we now turn our attention to environmental considerations—namely, how automated machines used in mass finishing and shot blasting can impact the earth’s resources, and how manufacturers can mitigate that impact. The International Institute for Sustainable Development notes that the rise of automation has thrust us into a “Fourth Industrial Revolution,” citing energy use, resource use, and ecosystems as the three most critical factors to watch as more automated processes are implemented. These are important considerations, given that manufacturers often are targeted in headlines about waterway pollution and even global warming, but responsible manufacturing practices can help avoid the most egregious impacts and keep manufacturing operations in compliance. Process Water Handling In the process of mass finishing and wet blasting, the biggest consideration is with regard to the process water discharged from the finishing machines. Often, this water is tinged with metal and media fines; at times, it can also contain oil and dissolved metal. Of course, process water will carry the compound being used in the specific finishing process. Mass finishing process water in different cleaning stages. So how can operators of automated mass finishing machinery take special consideration to limit the contamination of any process water discharged from the plant? There are two main ways to effectively curtail such constituents. Central Treatment The establishment of a protocol that includes a central wastewater treatment plant is quite effective in removing contaminants. Also, such facilities require fewer dedicated staff members, which adds to the efficiency of this approach. Centrifuges This universal cleaning system is deployed to separate, purify, extract, and wash various materials using centrifugal force to generate 2,000 times the earth’s normal gravity. These systems also require little operator attention, can be acquired in completely automated or semi-automated configurations, and can be used for most standard mass finishing applications. Rosler offers two centrifuge models; the semi-automatic Model Z 800 and the fully automatic Z 1000. Rosler's Z 800 centrifuge is semi-automatic. Rosler's z 1000 centrifuge is fully automatic. With the right approach to treating discharged process water, you can ensure you are a good steward of your environment, while also maximizing the efficiencies and benefits to be gained from automating your mass finishing and wet blasting operations. The Rosler Way The experts at Rosler are uniquely qualified to develop an automated finishing process for your surface finishing needs that is both effective and ecologically responsible. Contact us to get started today. In the next installment of the Automation Blog Series, we’ll look at the equipment that best positions your business for successful automation of your mass finishing and shot blasting operations. The complete Automation Series includes: Part 1 – How Robots are Improving Mass Finishing and Shot Blasting Processes. Part 2 – Why Automation is Beneficial for Your Business. Part 3 – What Problems Do You Want to Solve? Part 4 – How Do I Select the Right Machine and Consumables? Part 5 – What Automation Hardware is Available? Part 6 – Environmental Considerations of Automation. Part 7 – The Top 3 Mass Finishing and Shot Blasting Machines. Sign up for enews alerts to be notified of all Rosler blog posts!

Rosler & Lumag – Combining Multiple Solutions in a Single Finishing System

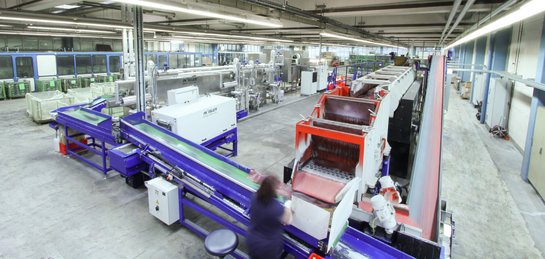
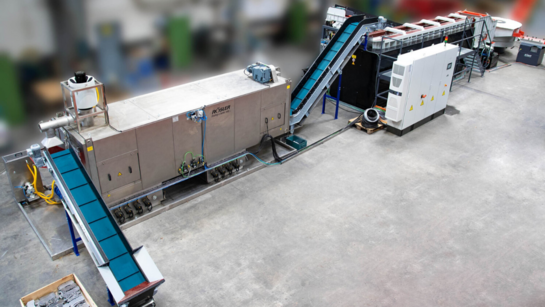
Finding a solution to our clients’ needs is nothing new for Rosler , nor is combining multiple solutions into a single finishing system. Take our work with Polish brake pad manufacturer Lumag Sp. z o.o. (Lumag) , for example. When they faced the challenge of de-oiling, deburring, and surface roughening brake pad carrier plates as part of their punch press process, they turned to us for a cleaning and mass finishing solution. The Situation Upon its founding in 1988 by Marek Zak, Lumag specialized in the production of brake linings. As the company implemented its own brake pad manufacturing technology, their products and offerings evolved. In addition to achieving enormous technological progress and applied engineering solutions, Lumag amassed a collection of machinery in need of constant upgrades and integration. In order to meet the continuous rise of quality and safety standards for its brake pads for drum and disk brakes for commercial vehicles as well as brake pads for passenger cars and motorcycles under the trade name Breck , Lumag needed a partner with automotive expertise who could combine multiple solutions in a single system. De-Oiling, Deburring, and Surface Roughening With the change of its production method for the brake pad carrier plates from casting to stamping , Lumag decided to install a new in-house manufacturing line for these products. The new system must allow for stamped carrier plates with lengths of 8-10 in (210-250 mm) and widths of 3-5 in (90-110 mm). The work pieces also have a slit or drilled hole to allow a sensor to monitor brake pad wear after installation and must undergo de-oiling, deburring, and surface roughening during the finishing process. These steps are necessary to ensure that the delicate stampings provide optimum adhesion characteristics for the subsequent bonding of the brake pads. Another requirement presented by the customer was to directly link the finishing equipment with the punch press while providing extremely gentle processing and the complete automation of the cleaning (de-oiling) and mass finishing stages in a continuous feed operation. In addition to an excellent reputation in the industry, Rosler’s ability to supply the equipment for both processes and the finishing media and compounds from one single source was a bonus for Lumag. Intelligent Media Selection Allows for Cleaning Without Drying After the stamping process, a conveyor belt transfers the work pieces to the drum washing machine equipped with an internal transport auger. In the drum the carrier plates initially pass through an un-perforated zone into which cleaning liquid is applied by spray nozzles. This creates an immersion bath for de-oiling. In the following perforated drum section, the cleaning liquid is drained, and in a secondary de-oiling step the work pieces are spray washed. This cleaning zone is followed by a drip-off section, a rinse station, and another drip-off section. Complete Rosler system with transport container Subsequently, a conveyor belt transfers the work pieces into the mass finishing machine. Replenishment of the cleaning liquid takes place with a Dosatron proportional dosing pump. Since the cleaning liquid and the compound for the mass finishing process have practically the same chemical characteristics—including the placement of a temporary corrosion protection—carryover of the cleaning liquid into the mass finishing machine presents no issue. This clever trick eliminated the need for a drying stage after the cleaning process, resulting in significant savings in the overall capital expenditure as well as reducing operating costs. For proper maintenance of the cleaning liquid the washing machine is equipped with filtration units and an oil separator. Gentle Mass Finishing Deburring and surface roughening of the work pieces takes place in a linear, continuous flow vibrator R 550/6600 DA with a specially adapted work piece loading system. Loading actually takes place at the rear end of the processing bowl instead of on the lateral bowl side with greatly reduced dropping heights. Similar gentle work piece transfers were incorporated in the vibratory screening unit and the drier filled with Supervelat drying media. After drying a certain work piece quantity based on precisely measured weight, components are discharged into a transport bin. The process water from the mass finishing machine is continuously cleaned in a fully automatic peeling centrifuge Z 1000 equipped with automatic sludge discharge. The Rosler Way Whatever challenges you face in surface finishing, Rosler is eager to find a better way both individually and as a whole. With more than 80 years of experience, we have the knowledge and drive to continually learn about, develop, and deliver precise solutions. Contact us to discuss your unique challenges and how we can innovate a solution for your needs and goals.

Forge & Foundry, Part 10 – Shot Blasting Machines Commonly Used for Die Castings

At Rosler Metal Finishing , we have more than 80 years of experience. In that time we have worked with numerous forge and foundry customers. One focus has been the development of shot blasting systems for different types and sizes of die castings. Our Forge & Foundry Blog Series continues with an overview of our top 10 shot blasting machines for precise, repeatable finishing results with die casted work pieces. Our shot blasting technology includes batch and continuous options. Continuous Shot Blasting Machines RMBD Continuous Tumble Belt Machine Rosler RMBD Continuous Tumble Belt Machine The high-capacity, continuous feed RMBD features an innovative tumble belt work piece transportation system that simultaneously processes and transports work pieces through the system. Small die cast parts Ideal Work Pieces — Large volumes of small- to mid-sized work pieces that can tumble over each other such housings, covers, brackets, frames, handles, and the like RHBD Continuous Spinner Hanger Machine Rosler RHBD Continuous Spinner Hanger Machine With an overhead monorail trolley transport system, the RHBD is capable of processing single, large and heavy work pieces in continuous feed mode while batches of mid-sized work pieces can be placed on a special work piece fixture shaped like a Christmas tree. The die cast version features a special screening system to remove flashes from the blast media. Large and complex die cast part ideal for a continuous or batch hanger type machine Ideal Work Pieces — Cylinder heads, engine blocks, transmission housings, turbocharger housings, large structural car parts with complex geometries RDGE Continuous Wire Mesh Belt Machine Rosler RDGE Continuous Wire Mesh Belt Machine Work pieces pass through the shot blast area on a wire mesh belt, never touching each other during the shot blast process within the RDGE . Mid-sized, less complex die cast part are ideal for wire mesh belt shot blast machines Ideal Work Pieces — Delicate mid-sized components such as cylinder head covers, chassis frame components for cars, transmission housings, oil pans, lighting components, etc. RMBD work pieces Batch Shot Blasting Machines RMT Multi-Tumbler Batch Shot Machine Rosler RMT Tumbler Bast Shot Blast Machine Barrel Batches of work pieces are placed in the RMT ’s specially shaped rotary drum for optimum work piece mixing. RMBC Batch Tumble Belt Blast Machine Rosler RMBC Batch Tumblast Machine The heart of the RMBC batch machine is an endless belt made from rubber or steel slats forming a trough on which work pieces tumble intensively. Ideal Work Pieces (For both RMT and RMBC machines) — Relatively small- and mid-sized, sturdy components that can tumble over each other like brackets, holders, clamps, semi-finished castings, small gears, etc. RHBE Batch Spinner Hanger Machine Rosler RHBE Spinner Hanger Machine An electric trolley running on an overhead rail, usually in the shape of a Y, drives the work pieces in and out of the RHBE shot blast machine. Larger work pieces are processed individually while smaller to mid-sized work pieces are placed on a fixture shaped like a Christmas tree for processing. Large complex die casting ideal for a spinner hanger blast machine application Ideal Work Pieces — medium to large work pieces including large transmission housings, large structural car parts, engine blocks, cylinder heads, large oil pans, dashboard frames, etc. RDT Rotary Table Machine Rosler RDT 250 Rotary Table Machine with an empty table Single, large components or small batches of smaller work pieces are placed on a rotary table within the RDT and blasted from above. A die-casting mold processed by Rosler's RDT Ideal Work Pieces — Small batches of mid-sized to large die castings; frequently used for cleaning of molds and auxiliary parts. RWK Turning Chamber Machine Rosler RWK Swing Chamber Machine The RWK is equipped with a circular chamber divided into two 180° sections with one section in the blast chamber and the other section at the load/unload station. After each cycle, the chamber rotates 180° to allow for simultaneous loading/unloading and processing. An automotive wheel processed by Rosler's RWK Ideal Work Pieces — Circular and semi-circular parts up to 48 in high such as drive shafts, automotive wheels, housings for electric motors when the blast operation is included in the manufacturing cell RWT Turning Table Machine Rosler RWT Turning Table Machine Much like the RWK, the RWT includes a circular chamber divided into two 180° sections with one section in the blast chamber and the other section at the load/unload station. After each cycle, the chamber rotates 180° to allow for simultaneous loading/unloading and processing. Differing from the RWK, the RWT is better suited for small- to mid-sized, delicate work pieces that must be protected from part-on-part contact during processing. This machine is always equipped with an air blast system for precise, targeted blasting. Ideal Work Pieces — Circular and semi-circular parts including small drive shafts, small pistons, fuel pump wheels RROB Roboblaster Machine Rosler RROB Roboblaster Machine The center of the RROB is a robot, which does the loading/unloading as well as the handling of the work pieces in the blast machine. The robot picks up one, single raw work piece from the staging system (e.g. a conveyor), holds the work piece into the blast chamber while constantly rotating it, and deposits it back on the conveyor. Cylinder head casting Ideal Work Pieces — Cylinder heads, engine blocks, cylinder blocks, crankcases, transmission housings The Rosler Way Whatever shot blasting challenge you face, trust Rosler to develop and deliver a solution. Contact us to learn how we can help you find a better way to process your die castings. The complete Forge & Foundry Series includes: Part 1 – Shot Blasting Systems. Part 2 – Efficient Recycling. Part 3 – Shot Blasting & Sand Castings. Part 4 – Selecting a Shot Blasting Machine for Sand Castings. Part 5 – Cleaning Features & Dust Precautions for Sand Castings. Part 6 – Selecting a Shot Blasting Machine for Die Castings. Part 7 – Selecting a Shot Blasting Machine for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 8 – Frequently Used Shot Blasting Machines for Sand Castings. Part 9 – Frequently Used Shot Blasting Machines for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 10 – Shot Blasting Machines Commonly Used for Die Castings. Part 11 – Top Mass Finishing machines for Cleaning Die Castings Part 12 – Media and Compound Selection, Effluent Handling Drive Success Sign up for enews alerts to be notified of all Rosler blog posts! https://vimeo.com/467660633
Automation, Part 5 – What Automation Hardware is Available?

As previously discussed in our Automation Blog Series, building a robotically assisted process requires evaluating your surface finishing system along with its problems and goals and selecting the right machine and consumables . Automating a mass finishing or shot blasting process also requires selecting the automated hardware that will best achieve your overall goals and provides the most efficiency in terms of time and manual labor. An experienced partner such as Rosler Metal Finishing can provide insight and advice on the numerous material handling tools specially designed or adapted to mass finishing and shot blasting process improvement. Work Piece Loading Systems Including skip loaders, lift and tip loaders, vibratory feed hoppers, and other tools, work piece loading systems are ideal for small- to mid-sized work pieces handled in bulk. A lift and tip loader with integrated vibratory hopper is included in this Rosler FKS mass finishing system. These loading systems can be movable—for example, on rails—to serve several machines. They can also be placed on weighing cells to determine the exact work piece quantity by weight and adjust machine loads accordingly. This RMBC Tumblast Machine from Rosler is equipped with a skip loader. Conveyor Belts Used for loading and intermediate transport, conveyor belts are commonly used for mid-sized to larger work pieces. These belts must be able to withstand moisture and sometimes harsher industrial conditions. They must also be well-sealed to prevent aggressive liquids or abrasive media from destroying their drive systems and bearings. This Rosler DA system is equipped with part and media conveyors on an inline vibratory machine. Part and media conveyors on an inline vibratory machine Roller Conveyors Commonly used to transport large, heavy work pieces such as large steel beams and plates, roller conveyors are also utilized for automatic staging of raw parts and backfilling finished parts into part bins. Roller conveyors on this Rosler FKS mass finishing system stage finished work pieces. Steel plates and beams are transported through this Rosler RRB shot blast machine via roller conveyors. Robots Increasingly utilized for work piece loading and unloading, robots are also used to manipulate work pieces in a mass finishing or shot blasting machine. In conjunction with robots, special quick-connect couplings and grippers allow for the automatic attachment and release of the work pieces to and from special workstations. This Rosler RROB Roboblaster includes robotic manipulation of work pieces. Additional examples of automated material handling equipment include: Gantry systems, which can handle very large work pieces. Walking beam cross conveyors for staging steel plates and beams in roller conveyor blast systems and preservation lines. Backfill systems, which gently return finished parts back into waiting part bins or buffer tables for intermediate storage of the finished work pieces. Robot attachment and removal of work pieces from the work station of this Rosler SF drag machine is achieve with quick connect couplings. Rosler Expertise With more than 80 years of expertise, Rosler has worldwide experience in finding solutions to challenging surface finishing solutions. Developing automated hardware and integrating robotic solutions is one of our many strengths. Contact us today to learn how we can improve and automate your finishing system. The complete Automation Series includes: Part 1 – How Robots are Improving Mass Finishing and Shot Blasting Processes. Part 2 – Why Automation is Beneficial for Your Business. Part 3 – What Problems Do You Want to Solve? Part 4 – How Do I Select the Right Machine and Consumables? Part 5 – What Automation Hardware is Available? Part 6 – Environmental Considerations of Automation. Part 7 – The Top 3 Mass Finishing and Shot Blasting Machines. Sign up for enews alerts to be notified of all Rosler blog posts!

Consumable Innovations Improve Finishing Outcomes

True to our mantra of “finding a better way…” Rosler Metal Finishing is constantly working to optimize our consumables . These improvements and additions to our offerings improve process stability, cost efficiency, and productivity of surface finishing processes. From media composition and compounds to wastewater handling, Rosler is dedicated to constant enhancement in the area of consumables as well as our mass finishing and shot blasting technology. Media One such example is Rosler’s development of a plastic media with the grinding and non-chip characteristics of ceramic media . Minimizing the risk of work piece damage, this range of high-density plastic media exactly achieves this frequently requested combination. High-density plastic media Through their special composition, these plastic grinding media have the same grinding and metal removal characteristics as their ceramic “siblings” yet demonstrate a higher elasticity. This media type also allows faster processing of delicate work pieces made from non-ferrous metals as well as parts that tend to bend during the finishing process. Liquid, Pumpable Pastes Another breakthrough are the liquid pastes in the RSP and RPP 8 range. These innovative KeramoFinish® pastes, even though relatively viscous, can be delivered into the machine through a pump and thus can be dosed more precisely in line with the given processing requirements. Liquid, pumpable paste in the RSP and RPP 8 range Automatic dosing systems allow further optimization of the overall process. The utilization of such sophisticated dosing systems helps improve process controls and has proven that the desired finishing results can be achieved with less personnel. Granulated Wastewater Cleaners New developments can also be reported from the field of wastewater cleaning with recycling systems. Granular pellets are replacing the powder products that were previously used for flocculation and improvement of the sludge consistency. Granualated flocculant Granulated flocculants have several advantages. They allow optimized handling without the risk of dust, thus contributing to improved workplace safety. Granular versions also prevent so-called “bridge building” in the dosing units, which can lead to a dosing fault. The new granulated flocculants can be dosed with existing dosing units and achieves more precise dosing. Precision is very important for processes where process water tends to foam. All these characteristics, in combination with the mechanical stability of the granules and short reaction times, ensure a significantly improved process stability. New development consumables The Rosler Way Finding a better way is more than a saying at Rosler; it’s our passion. We strive to outdo ourselves with each innovation and upgrade in order to offer our clients the most-advanced and best-suited finishing technologies and products. Contact us to discuss your unique challenges and how we can innovate a solution for your needs and goals.

Forge & Foundry, Part 9 – Frequently Used Shot Blasting Machines for Forgings, Non-Sand Castings, and Powdered Metal Components

Rosler Metal Finishing has worked in the forge and foundry industries for decades. With more than 80 years of experience, we have developed sophisticated shot blasting systems for countless work pieces including forgings, non-sand castings, and powdered metal components. Our Forge & Foundry Blog Series continues with an overview of our shot blasting machines most frequently used on these specific types of work pieces. It is important to understand your work piece and process requirements including whether components will be processed continuously or in batches. When it comes to finishing forgings, non-sand castings, and powdered metal components, our shot blasting machines are divided into three categories based on how the work pieces are fed into the machine: continuous, batch, and specially engineered shot blasting machines. Continuous Shot Blasting Machines RMBD Continuous Tumble Belt Machine Rosler RMBD Continuous Tumble Belt Machine The high-capacity, continuous feed RMBD is available in a heavy-duty version for large forgings and castings, which is equipped with 6 x 40 HP turbines, a steel-slatted work piece transport belt, and a magnetic separator. Work pieces processed by Rosler's RMBD Ideal Work Pieces — Large volumes of small- to mid-sized work pieces such as connecting rods, transverse car links, parts for automatic transmissions, locking systems, brake pads, oil pans, cylinder head covers RHBD Continuous Spinner Hanger Machine Rosler RHBD Continuous Spinner Hanger Machine With an overhead monorail trolley transport system, the RHBD is capable of processing single, large, and heavy work pieces in continuous feed mode while batches of small- to mid-sized work pieces can be placed on a special work piece fixture shaped like a Christmas tree. The special foundry version features extra wear-proof lining in the blast chamber and a magnetic separator. Work piece processed by Rosler's RHBD Ideal Work Pieces — Forged levers, crankshafts, impellers, large pistons RDGE Continuous Wire Mesh Belt Machine Rosler RDGE Continuous Wire Mesh Belt Machine Work pieces pass through the shot blast area on a wire mesh belt, never touching each other during the shot blast process within the RDGE . Work pieces processed by Rosler's RDGE Ideal Work Pieces — Delicate mid-sized components such as chassis frame components for cars, housings, all kinds of gears, door pillars for passenger cars Batch Shot Blasting Machines RMT Multi-Tumbler Batch Shot Machine Rosler RMT Tumbler Bast Shot Blast Machine Barrel The RMT’s specially shaped rotary drum optimizes work piece mixing. Work pieces processed by Rosler's RMT Ideal Work Pieces — Very small to mid-sized, sturdy components such as bushings, fittings, small shafts, chain links, levers RMBC Batch Tumble Belt Blast Machine Rosler RMBC Batch Tumblast Machine The heart of the RMBC batch machine is an endless belt made from rubber or steel slats forming a trough. Work pieces tumble intensively within the trough. Work pieces inside Rosler's RMBC Ideal Work Pieces — Relatively small and mid-sized, sturdy components including cast turbine blades, all kinds of fittings, small pump housings, shafts, small gears, springs RHBE Batch Spinner Hanger Machine Rosler RHBE Batch Spinner Hanger Machine with heavy-duty crane An electric trolley running on an overhead rail, usually in the shape of a Y, drives the work pieces in and out of the RHBE shot blast machine. Work piece processed by Rosler's RHBE Ideal Work Pieces — Mid-sized to very large and heavy work pieces weighing up to 15 tons including very large crankshafts, gears RDT Rotary Table Machine Rosler RDT 250 Rotary Table Machine with an empty table Single, large components or small batches of smaller work pieces are placed on a rotary table within the RDT and blasted from above. A mold cleaned by Rosler's RDT Ideal Work Pieces — Mid-sized to large, heavy components; frequently used for cleaning of forgings and other molds RWK Turning Chamber Machine Rosler RWK Swing Chamber Machine The RWK is equipped with a circular chamber divided into two 180° sections with one section in the blast chamber and the other section at the load/unload station. After each cycle the chamber rotates 180° to allow for simultaneous loading/unloading and processing. A bevel gear processed by Rosler's RWK Ideal Work Pieces — Circular and semi-circular parts up to 48 in high such as drive shafts, bevel gear components, automotive wheels RWT Turning Table Machine Rosler RWT Turning Table Machine Much like the RWK, the RWT includes a circular chamber divided into two 180° sections with one section in the blast chamber and the other section at the load/unload station. After each cycle the chamber rotates 180° to allow for simultaneous loading/unloading and processing. Differing from the RWK, the RWT is better suited for smaller, delicate work pieces. Work pieces processed by Rosler's RWT Ideal Work Pieces — Circular and semi-circular parts including sprockets, small drive shafts, small pistons, fuel pump wheels Specially Engineered Shot Blasting Machine RKWS Crankshaft Shot Blast Machine Rosler RKWS 3 x4 Crankshaft Shot Blast Machine Designed to blast clean various sizes of crankshafts, the RKWS features a carousel divided into three or four chambers to create multiple blast chambers and one load/unload station. Fully automatic operation is enabled with the use of robotic work piece handling. Crankshafts before and after processing by Rosler's RKWS Ideal Work Pieces — Crankshafts in lengths of 12-28 in and weights of 14-55 lbs The Rosler Way Backed by more than 80 years of experience, Rosler has the expertise to develop the right machine and process for your forgings, non-sand castings, and powdered metal components. Contact us today to learn how we can help improve your finishing processes and schedule a free sample processing in our test center . The complete Forge & Foundry Series includes: Part 1 – Shot Blasting Systems. Part 2 – Efficient Recycling. Part 3 – Shot Blasting & Sand Castings. Part 4 – Selecting a Shot Blasting Machine for Sand Castings. Part 5 – Cleaning Features & Dust Precautions for Sand Castings. Part 6 – Selecting a Shot Blasting Machine for Die Castings. Part 7 – Selecting a Shot Blasting Machine for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 8 – Frequently Used Shot Blasting Machines for Sand Castings. Part 9 – Frequently Used Shot Blasting Machines for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 10 – Shot Blasting Machines Commonly Used for Die Castings. Part 11 – Top Mass Finishing machines for Cleaning Die Castings Part 12 – Media and Compound Selection, Effluent Handling Drive Success Sign up for enews alerts to be notified of all Rosler blog posts! https://vimeo.com/467660633