Solution Finder
SOLUTION FINDER

Your guide through the
Rösler product world

With just a few clicks you will find the right machine for your needs!


Results: 237 Articles - 55 Products
HP Jet Fusion 5200 3D Printing System

HP and AM Solutions Present the Innovative HP Jet Fusion 5200 Series 3D Automatic Unpacking Station

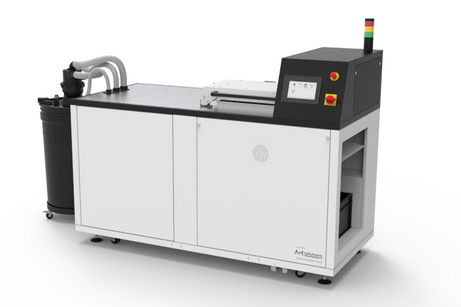
With the HP Jet Fusion 5200 Series 3D Automatic Unpacking Station, HP and the Rösler brand AM Solutions – 3D post processing technology, present their first product that was jointly developed on the basis of their cooperation agreement announced last year. This scalable, industrial post processing solution allows the fully automatic and consistent unpacking of AM parts made on the HP Jet Fusion 5200 3D Printing System in a continuous workflow. Compared to manual unpacking operations, the new solution offers not only a significant productivity increase and a greatly improved cost efficiency, but also a considerably higher powder reclaim rate for certain geometries. The Automatic Unpacking Station will be manufactured at the German location of the Rösler brand AM Solutions – 3D post processing technology. As a global leader in the field of industrial 3D printing solutions and digital manufacturing, HP recognized early on that the use of 3D printing on an industrial scale is only possible, if the printing and post processing operations can be combined into one automated, scalable process. About one year ago HP and AM Solutions – 3D post processing technology, a division of Rösler that specializes in post processing solutions for 3D printed parts, announced a cooperation agreement. This created the ideal foundation for developing such an integrated, industrial solution. The HP Multi Jet Fusion technology offers the possibility for volume production on an industrial scale. On the other hand, post processing still requires a great deal of manual operations. This is now changing with the innovative Automatic Unpacking Station for the HP Jet Fusion 5200 series. This unpacking station, the first result of the cooperation between HP and AM Solutions – 3D post processing technology, combines the full range of print, software and material knowhow at HP with more than 80 years of experience in the fields of surface treatment and equipment manufacturing for industrial applications at Rösler. Consistent, repeatable unpacking and a high powder reclaim rate The automatic unpacking process takes place immediately after the cooling of the build job in the HP Natural Cooling Unit. A lifting device is used to transfer the cooling unit to the Automatic Unpacking Station. There it is positioned, unlocked, and the entire build job is placed in the station. All relevant printing job data are transmitted to the unpacking station by means of its RFID reader. This ensures that the job- and process-related data can be tracked and the process monitored remotely by means of HP’s 3D Center software. Furthermore, the automated unpacking process, adapted to the individual work pieces, allows a considerably higher powder reclaim rate for certain geometries. An air suction system transfers the powder collected in the station continuously to a dedicated external tank. The printed parts are discharged into an unloading box. Once the external tank is full, it is replaced with an empty one, and the retrieved powder can be loaded back into an HP Build Unit after connecting the full tank to the Processing Station. The new Automatic Unpacking Station minimizes not only manual operations but also reduces the overall cycle time for certain applications, as the unpacking operation can start right after the recommended minimum cooling time is completed. Ramon Pastor, GM and Global Head of HP 3D Printing & Digital Manufacturing explains: “New solutions for the scalable, efficient post processing and automation of the entire workflow are the precondition for fully exploiting the advantages of Additive Manufacturing and making it suitable for industrial volume production.” Pastor continues: “With Rösler/AM Solutions we have found a partner who is intimately familiar with the standards of a broad range of industries and possesses the required knowhow in the field of surface treatment and equipment manufacturing.” Stephan Rösler, President & CEO of Rösler OberflĂ€chentechnik GmbH, adds: “The comprehensive knowledge of HP in the areas 3D printing, software and digitized manufacturing allows us to quickly develop innovative solutions for the 3D post processing and adapt these solutions to the demands of industrial users.” This premise is fully confirmed by Matteo Rigamonti, Founder at Weerg: “The HP 3D Automatic Unpacking Station has fully met our expectations for an automatic unpacking solution. With a growing fleet of HP Jet Fusion 5210 systems at high-volume production, the unpacking process requires a lot of time and resources. Thanks to this solution, our unpacking process became not only significantly faster, but we are also reclaiming more powder. The process is precise, and works well even for small and delicate parts.” The company, a leading industrial parts provider located in ScorzĂš, Italy, produces around 2,500 pieces per day and has thoroughly tested the new machine at their facilities during numerous trial runs. Matteo continues: “As we expand our business, these enhanced capabilities are designed to help us meet customer demand, and improve our turnaround times, for high volume production parts.”

Automotive Supplier Achieves Process Stability, High Cost Efficiency with Modular Shot Peening System

For transmission components like gears and shafts, shot peening has become an indispensable step in the overall manufacturing process. With the RWT swing table machine, Rosler developed a modular equipment concept that can be easily adapted to different technical requirements and offers a maximum in process stability paired with absolutely repeatable peening results and high cost efficiency. One of the numerous customers within the automotive industry utilizing the RWT is an Asian automotive supplier. The Need As part of a capacity expansion for minivan transmissions, this customer increased annual production to 40,000 units and decided to carry out the required shot peening operation in-house instead of subcontracting it to an external job shop. The specifications called for a system that can handle around 560,000 single work pieces per year, including 15 different types of gears and shafts. Each work piece type required the development of a specific peening program based on drawings and various work piece materials. Another requirement was the tight control of the entire peening process capable of handling gears and shafts with diameters of 12 in (300 mm), heights of 20 in (500 mm), and weights of up to 55 lb (25 kg). The Solution The customer chose the Rosler shot peening system RWT 13/4 So due to its capability and fully automatic processing. This pressure blast system includes a table with two 180° segments, each equipped with two satellite stations which allows two parts to be processed in one segment while another pair of parts is loaded/unloaded in the other segment. For complete coverage of the work pieces, the RWT is equipped with four blast nozzles – two for vertical and two for horizontal movement. Since some areas of the work pieces are completely finished before entering the machine, special wear-resistant masking is integrated into the work piece fixtures to protect the already finished surface area from being blasted. To meet all customer requirements, the system design allows the parallel use of two different blast media types or one type with different shot sizes. Rosler tested various work pieces during the course of the project. Rosler’s global test centers and the in-house X-ray diffraction measurement capabilities showed that the achieved compressive stress values were twice as high as the values stipulated by the customer. The in house X-ray diffractometer allowed Rosler to shorten the process development cycle for these transmission components. The measurement system can also be used for a variety of other parts besides gears and shafts. These can include valve and chassis springs, other chassis components, airplane turbines , and components for the energy generating industry. Rosler also offers x-ray diffraction measurements as a service . Developed for Success The RWT’s concept can easily be adapted to specific customer requirements since its swing table design is based on a modular concept developed for shot peening of rotationally symmetrical components. The RWT's blast chamber Compared to other peening systems on the market, the blast chamber contains considerably more wear protection and is easier to access for maintenance work. The pressure blast system requires a considerably lower amount of compressed air and, therefore, runs more efficiently. The RWT's monitoring and control system A comprehensive monitoring and control system measures the air volume to ensure the high process safety and consistency required for any shot peening operation. The RWT's blast nozzles The nozzles can be moved vertically and horizontally as well as pivoted at an angle from 0 to 90°. This guarantees complete coverage of all work piece surface areas over a large part size variety. The high efficiency of the pressure blast system results in significant savings in compressed air consumption. For controlling the overall peening process Rosler also uses standard components. These include the automatic control of the blast media throughput and the precise measurement of the media throwing speed directly at the nozzle exit. The Magna valves for precise dosing of the blast media as well as all media hoses can also be monitored. The RWT can be equipped with a spiral separator for discharging any broken-down blast media. The Rosler Way With more than 80 years of experience, Rosler has the knowledge and expertise to find the exact shot peening machine to meet your needs. Contact us to discuss your challenges and be sure to sign up for enews alerts to be notified of new posts! https://vimeo.com/142621047

Blast equipment modernization and upgrade – an efficient alternative to buying new

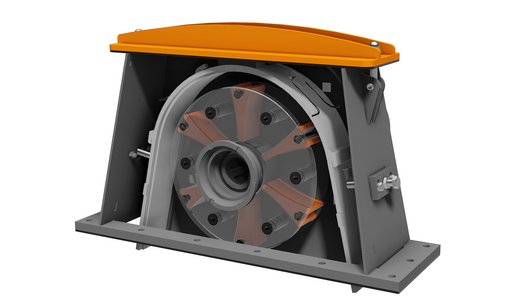
Turbine replacement results in a 45% higher blast performance and lowers operating costs by one third Growing maintenance and operating costs combined with a declining blast performance; these are usually good reasons for investing in a new shot blast machine. By taking advantage of the Rösler Retrofit program for a shot blast machine in its foundry division a leading company for drivetrain technology and electronic controls chose a significantly less expensive but highly effective alternative. The existing shot blast machine was upgraded with the foundry version of the Rösler Gamma 400G-8 high performance turbines. This turbine upgrade helped reduce the expenses for maintenance by two thirds and the overall operating costs by more than 34%. At the same time, the blast performance could be increased by 45 percent. This resulted in an amortization time of a little over one year. The turbines in shot blast machine must carry a heavy load and are exposed to a lot of stress. Over time this leads to ever increasing maintenance and operating costs along with a growing energy consumption. Frequently, the blast performance no longer meets the capacity and quality demands. In order to fulfill their shot blasting requirements in a cost-efficient and competitive manner companies usually invest in a new shot blasting system. A persuasive modernization solution with a quick amortization A renowned manufacturer of drivetrains and electronic controls was facing exactly this problem with a shot blast machine in its foundry. The responsible project managers at the company contacted TuneUp, a division of the Rösler OberflĂ€chentechnik GmbH, that specializes in the modernization of shot blast equipment . On this occasion they learnt that the Rösler modernization and upgrade service covers not only Rösler equipment but extends to third-party machinery as well. After a comprehensive analysis of the current equipment condition the Rösler Retrofit experts presented a suitable technical solution along with a realistic amortization calculation. The customer was impressed by the technical depth and short pay-back period of the proposed modernization concept. Turbine replacement increases productivity and lowers costs At the center of the modernization concept was the replacement of the two 22 kW turbines originally supplied with the shot blasting machine. The existing units were exchanged with high performance Gamma 400G-8 turbines in wear-resistant foundry version, also with a drive power of 22 kW each. They are equipped with eight curved throwing blades in „Y“-Design with a precisely calculated curvature. This generates an extremely high throwing speed along with a precise media guidance and results in an optimal efficiency. The unique characteristics of the Gamma turbines with a 45% higher blast performance allowed achieving the needed capacity increase. Another feature of the new high performance turbines is that they require a lot less energy. The energy savings were an important reason for the overall operating cost decrease of 34%. Expenses for maintenance reduced by over two thirds The unique design of the throwing blades produces not only a higher performance but allows using both blade sides by simply turning them around. Depending on the utilized blast media, this design feature, combined with the use of wear resistant blade material, for example, forged tool steel, results in a three times longer lifetime compared to conventional turbines. An innovative quick-change system allows easily and quickly changing the blades at the mounted turbine. The usually required time-consuming dismounting of impeller, control cage and infeed pipe is no longer necessary. Overall this reduces the expenses for maintenance by more than two thirds. Quick amortization produces a competitive edge Based on the capacity utilization to-date, the productivity increase achieved by the upgrade and the cost savings the Retrofit investment will have paid for itself already after 1.1 years. The technical features of the modernized shot blasting machine and the quick amortization allow the user to improve his profitability and consolidate and expand his competitive position in the market.

Mass Finishing Media, Part 1 – Don’t Navigate the Complex Selection Process Alone

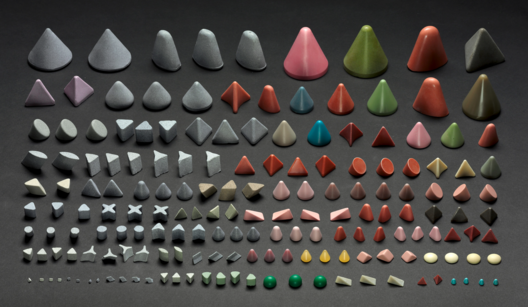
The importance of the media selection in any surface finishing process cannot be emphasized enough. These consumables are essential “precision tools” for achieving the specified finishing results. Selecting the right media is a complex task. That’s why you should consult an expert such as Rosler for guidance. Even after a mass finishing process has been established, the media status must be constantly monitored and, if necessary, corrected. When different work pieces are processed or finishing tasks are altered, exchanging the currently used media type with another may be required. Careful and collaborative media selection is crucial to a mass finishing success. Consider the Characteristics The work pieces should always be at the center of the media selection process and take into consideration its starting surface burr condition, material, shape, size, and desired surface finish. Media characteristics must complement the work piece as well as the machine being utilized. Media characteristics to consider in relation to work pieces and the machine utilized include: Bond – Ceramic media generally has a higher density than plastic media , making ceramic more aggressive. While typically more gentle, plastic media can sometimes produce unwanted foam known as “dirt foam.” Type/Abrasiveness – Deburring/edge radiusing and/or aggressive surface grinding require a more abrasive media than gentle surface smoothing. Shape – Media may have to reach very tight corners and internal passages. Choosing the right media shape is crucial for reaching all critical surface areas. Size – Always choose the largest possible media that fulfills the finishing tasks for the most efficient process. Lodging issues – Media lodged in the work piece can have disastrous consequences for downstream manufacturing. Selecting a media shape and size that prevents lodging is crucial. Color – Choosing a media color that differs from the work pieces helps identify lodging issues. Potential for damage – For delicate work pieces, gentle yet effective media must be selected to avoid bending thin walls or damaging critical sealing areas requiring a tight fit. Separation – Reliable media separation from the finished work pieces must be allowed by screens, inverse screens, magnetic separators, or, in extreme cases, manual separation. Intensity – More intensive machines such as centrifugal disc systems or drag finishers usually require smaller, less abrasive media than vibratory models such as rotary and tub vibrators . Analyze Ongoing Costs Since finishing media is a consumable that wears and must be regularly replenished, cost is an ongoing concern. In some finishing process, the expenses for media account for more than 50% of the total process costs. Therefore, it is important to select a media that is both economical and effective to maintain a viable mass finishing process. While media costs also play an important role in the selection process, media choice should never be determined by price per pound. Instead, the media cost per work piece should be a guiding factor. For example, a lower priced media might require much longer processing times or wears a lot faster and would therefore be less economical than a higher priced media that achieves the desired finishing results in less time and has a lower wear rate! Rosler Testing Center Partners in Testing Whether your process uses ceramic, plastic, or drying and polishing media , a crucial step in selecting media should always be contacting the experts, i.e. your supplier. Since a media change might require extended test trials, your supplier should partner with you to test prospective media with your specific work piece in their test lab. The Rosler Way With more than 80 years of experience in surface finishing, the Rosler team is well equipped to prove media selection guidance. We also offer FREE sample processing in our global test centers . Contact us for all of your mass finishing needs! The complete Mass Finishing Media Series includes: Part 1 – “Don't Navigate the Complex Selection Process Alone.” Part 2 – “Tips for Measuring Media-to-Work Piece Ratio.” Part 3 – “Why Discharging Undersized Media, Maintaining Media Levels are Crucial.” Sign up for enews alerts to be notified of new posts!

Custom-engineered roller conveyor blast machine brings about considerable capacity expansion

Heidemann Stahl- & Montagebau und BHS Sandstrahltechnik GdR zĂ€hlen dank ihrer 30-jĂ€hrigen Erfahrung auf dem Gebiet des Stahlbaus zu den absoluten Experten. Dabei realisiert das Unternehmen aus Volkmarsen bundesweit Projekte fĂŒr Industrie, Handel, Gewerbe und Landwirtschaft. Ob Hallenbau, BĂŒhnen- oder BrĂŒckenkonstruktionen, GelĂ€nder oder TribĂŒnen - die individuellen Stahlbaulösungen mĂŒssen höchsten AnsprĂŒchen an Wirtschaftlichkeit und QualitĂ€t genĂŒgen. Dementsprechend bemisst sich auch die Erwartungshaltung der Kunden an die konstante QualitĂ€t der Stahlprodukte. KapazitĂ€tserweiterung beim Entzundern, Entrosten und Reinigen Um die stetig wachsende Nachfrage aus der Stahlindustrie bedienen zu können, reichen die KapazitĂ€ten der bestehenden Strahlanlage nicht aus. „Unsere aktuelle Strahlanlage ist nur 2 Meter breit, mit der KapazitĂ€tserweiterung auf 2,5 Meter erhoffen wir uns als Dienstleister eine deutliche Steigerung des Durchsatzes. Entscheidend fĂŒr uns ist die LeistungsfĂ€higkeit, QualitĂ€t und Langlebigkeit der Anlage“, fasst Peter Heidemann, GeschĂ€ftsfĂŒhrer von BHS Sandstrahltechnik, die Anforderungen zusammen. Die rĂ€umliche Begrenzung vor Ort war eine zusĂ€tzliche Herausforderung die Rösler mit langjĂ€hriger Erfahrung und Know-how löste. Kompakt, vielseitig, individuell – Rollenbahnstrahlanlage RRB 27/6-HD-So „ Rösler Rollenbahnstrahlanlage RRB 27/6-HD-SO wurde eigens auf unsere speziellen Anforderungen angepasst“, berichtet Peter Heidemann. Eine dieser Anpassungen ermöglichte die Realisation maßgeblich. Mit einer Gesamthöhe von nur 4.800 mm passte sich die Rollenbahnstrahlanlage, speziell konstruiert in Niedrigbauweise, optimal den rĂ€umlichen Gegebenheiten an. Um das geforderte Strahlergebnis des Reinheitsgrades SA 2,5 prozesssicher zu erzielen, ist die Strahlanlage mit insgesamt sechs Gamma 400 G Turbinen im Y-Design und einer Antriebsleistung von je 22 kW ausgestattet. Diese speziell, von Rösler entwickelte Turbinentechnik, zeichnet sich vor allem durch ihre Verschleißresistenz, Wartungsfreundlichkeit und Effizienz aus. Die Gamma Turbinen aus geschmiedetem Werkzeugstahl glĂ€nzen nicht nur mit dem Dreifachen an Standzeit, sondern erzielen im Vergleich zu herkömmlichen Turbinen eine bis zu 20 Prozent höhere Strahlleistung bei geringerem Energieverbrauch. Die strömungsoptimierten Wurfschaufeln im Y-Design können schnell und unkompliziert bei Verschleiß gedreht werden. Durch eine zweifache Verwendbarkeit bringen die Rösler-Turbinen ein enormes Einsparpotential im Hinblick auf Ersatzteilkosten mit sich, gleichzeitig reduziert sich der Maschinenstillstand. Eine, serienmĂ€ĂŸig aus Manganstahl gefertigte Strahlkammer, mit zusĂ€tzlich auswechselbaren Manganstahl-Platten steigert die AnlagenverfĂŒgbarkeit um ein Weiteres. Durch die innovative Strahlkammergeometrie reduziert sich der Platzbedarf. Lediglich zwei, in der Strahlkammer angeordnete Rollen aus gehĂ€rtetem Werkzeugstahl sorgen fĂŒr einen optimalen WerkstĂŒcktransport und senken die Verschleißkosten zusĂ€tzlich. Mit individuellem Konzept ĂŒberzeugt „Mit dieser speziell fĂŒr unsere BedĂŒrfnisse ausgelegten Strahlanlage bin ich optimistisch, dass wir unsere StrahlqualitĂ€t maßgeblich verbessern können, was letztendlich sowohl zu einer QualitĂ€tssteigerung unserer Produkte sowie zu einer Erhöhung der ProduktivitĂ€t unseres Gesamtvolumens fĂŒhren wird“, erklĂ€rt Peter Heidemann, GeschĂ€ftsfĂŒhrer von BHS Sandstrahltechnik und ergĂ€nzt: „Die Firma Rösler ist auch zukĂŒnftig unser erster Ansprechpartner fĂŒr Strahltechnik. Wir schĂ€tzen in der guten Zusammenarbeit vor allem die technische Expertise und individuelle Beratung“.

Ausbildungsstart in Zeiten von Corona: Rösler OberflĂ€chentechnik begrĂŒĂŸt 16 neue Auszubildende

Trotz der anhaltenden Corona-Pandemie und der damit einhergehenden wirtschaftlich angespannten Situation hĂ€lt Rösler auch in diesem Jahr an seiner hohen Ausbildungsquote fest. „Das Prinzip der dualen Ausbildung ist eine der bedeutendsten SĂ€ulen fĂŒr junge Berufseinsteiger“, betont Ausbildungsleiterin Anja SĂŒppel und ergĂ€nzt „gerade in der aktuellen Situation ist eine zukunftsorientierte Ausbildung mit QualitĂ€t und Struktur gefragt“. Als inhabergefĂŒhrtes Familienunternehmen ermöglicht Rösler den Berufsstartern einen professionellen Start ins Berufsleben und vermittelt wĂ€hrend der Ausbildung sowohl fachliche Kenntnisse als auch die Möglichkeit, ihre Talente und Ideen zu entfalten sowie vielfĂ€ltige Kompetenzen zu erlernen. Der Ausbildungsstart beginnt am 1. September 2020 wie immer mit einem BegrĂŒĂŸungstag in Memmelsdorf – dieses Jahr unter der Einhaltung der geltenden Hygiene- und Abstandsregeln. In den folgenden Tagen verschaffen die Projekttage den Berufsstartern erste Einblicke in die wichtigsten GeschĂ€ftsbereiche des Unternehmens und bieten zudem die Möglichkeit, sich untereinander besser kennenzulernen. Dabei treffen sie in Memmelsdorf und Hausen auf engagierte Kollegen und Fachausbilder sowie auf modern eingerichtete Schulungs- und AusbildungsrĂ€ume. Auch 2021 hat das Familienunternehmen Rösler wieder AusbildungsplĂ€tze zu besetzen. Das vielfĂ€ltige Ausbildungsangebot beim Spezialisten fĂŒr OberflĂ€chentechnik reicht von unterschiedlichen Berufen des technisch-gewerblichen ĂŒber den kaufmĂ€nnischen Bereich bis hin zu dualen Studienangeboten. Ein Indikator, dass sowohl die QualitĂ€t als auch die Rahmenbedingungen in der Ausbildung bei Rösler passen, sind die hervorragenden Ergebnisse bei den letztjĂ€hrigen AbschlussprĂŒfungen. Die Rösler-Gruppe bietet fĂŒr das Jahr 2021 folgende AusbildungsplĂ€tze an: Industriekaufleute, Chemielaboranten, Technische Produktdesigner, Konstruktionsmechaniker, Industriemechaniker, FachkrĂ€fte fĂŒr Metalltechnik, Mechatroniker, Elektroniker fĂŒr Betriebstechnik, FachkrĂ€fte fĂŒr Lagerlogistik. Ein dualer Studiengang ist möglich im Bereich Wirtschaftsingenieurwesen, Wirtschaftsinformatik und Elektrotechnik.Die Partnerhochschule von Rösler ist die Duale Hochschule Mosbach in Baden-WĂŒrttemberg. Online-Bewerbung sind möglich ĂŒber die Internetseite: www.rosler.com Bei Fragen zu Ausbildung/Dualem Studium gibt Anja SĂŒppel gerne Infos unter Tel.: +49 9533 / 924-442 oder per E-Mail an: a.sueppel@rosler.com

Forge & Foundry, Part 12 – Media and Compound Selection, Effluent Handling Drive Success

Regardless of the industry , the selection of media and compounds utilized in mass finishing can elevate or hinder finishing results. The handling of effluents – used process water – also factors into a process’ efficiency and end results. With more than 80 years of experience, Rosler understands the demands of the forge and foundry industries specifically and how to achieve precise and consistent finishing results by combining the latest technology, well-designed machines, and consumables . This installment of the Forge & Foundry Blog Series highlights how careful media and compound selection along with proactive handling of effluents assist in producing mass finishing efficiencies. Ingredients for Success Media and compounds are more than just “rocks” and “soap” thrown into a mass finishing machine. Instead, these consumables are sophisticated tools that can make a mass finishing process a success or a failure. Media choice with regard to shape, size, composition, and abrasiveness is as important as selecting the right machine. Selecting the wrong media could be detrimental to the process. The level of media in a machine is equally important. If not introduced in the prescribed ratio, even the best suited media will fail to deliver the desired results. For example, increasing the ratio of media relative to the work pieces has a cushioning effect and helps prevent unwanted work piece damage in the form of nicking. Conversely, skimping on media levels can produce ineffective finishing as well as work piece damage. Much like media, the compound selection must match the work piece material. For example, aluminum die-castings require a different compound than die-castings made from magnesium. Applying compounds in the prescribed dosage is also key to maintaining finishing results. For example, insufficient compound usage can cause foaming in the machine and discoloration of finished work pieces. Handled with Care Mass finishing produces an effluent containing media and metal fines, various chemicals from the compounds, and sometimes even chelated metals. At this point a decision must be made; will the effluent be cleaned and recirculated or discharged as waste? In either case, contaminants must be removed first. When discharging as waste, all contaminants must be removed to prevent pollution issues and discharge fines. Additional mass finishing process efficiency and greater ROI can be attained by cleaning effluent for reuse. The use of centrifugal filters is an excellent treatment method for effluent which factors in added benefits including reduced water usage and compound longevity. Rosler Centrifuge Technology By removing all solids in the form of media and metal fines from the mass finishing effluent, centrifuges allow the cleaned liquid, now free of any solids, to be reused by recycling it back to the mass finishing machine. This can result in water consumption savings of more than 90 percent. Since centrifuges do not degrade the compound in the process liquid, drastically reduced usage of compounds may also be achieved. The Rosler Way Whether you need help selecting a whole mass finishing system or the consumables used within it, the Rosler team can help. Our motto of “finding a better way
” applies to big picture thinking and day-to-day machine operations. Contact us to share your needs so we can develop a solution. The complete Forge & Foundry Series includes: Part 1 – Shot Blasting Systems. Part 2 – Efficient Recycling. Part 3 – Shot Blasting & Sand Castings. Part 4 – Selecting a Shot Blasting Machine for Sand Castings. Part 5 – Cleaning Features & Dust Precautions for Sand Castings. Part 6 – Selecting a Shot Blasting Machine for Die Castings. Part 7 – Selecting a Shot Blasting Machine for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 8 – Frequently Used Shot Blasting Machines for Sand Castings. Part 9 – Frequently Used Shot Blasting Machines for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 10 – Shot Blasting Machines Commonly Used for Die Castings. Part 11 – Top Mass Finishing machines for Cleaning Die Castings Part 12 – Media and Compound Selection, Effluent Handling Drive Success Sign up for enews alerts to be notified of all Rosler blog posts! https://vimeo.com/467660633

Mit dem neuen Dosiersystem von Rösler gesetzeskonform arbeiten

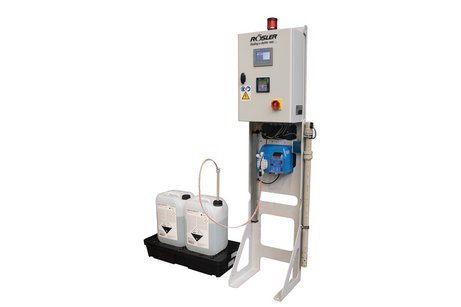
In der im August 2017 in Kraft getretenen 42. Bundesimmissionsschutzverordnung (42. BImSchV) werden vom Gesetzgeber Maßnahmen vorgeschrieben, um die Bildung von gesundheitsgefĂ€hrdenden Legionellen-StĂ€mmen zu verhindern. Dies betrifft auch das Betreiben von Nassfilter. Die Verordnung verpflichtet u. a. alle Betreiber von Nassabscheidern, regelmĂ€ĂŸig aufwendige PrĂŒfungen und Laboruntersuchungen auf Legionellen-Befall durchzufĂŒhren und zu dokumentieren. Bei Unterlassung drohen erhebliche Strafen. Unsere Lösung: Auf Grund unserer langjĂ€hrigen Erfahrung im Umgang mit Prozesswasser, haben wir fĂŒr alle Nassabscheider ein System entwickelt, dass die Entstehung von Legionellen gĂ€nzlich verhindert. Durch Einsatz unserer neuen Dosiereinheit RDS-pH 10/25 in Kombination mit unserem Verfahrensmittel Additiv RST-P1 wird der pH-Wert des Nutzwassers dauerhaft ĂŒber 10 gehalten. Dies wird automatisch dokumentiert. Das Entstehen von Legionellen wird dadurch im Vorfeld verhindert, Laboruntersuchungen können entfallen und gesetzliche Vorgaben werden zu 100 % erfĂŒllt. Ihr Nutzen: Das Entstehen von gesundheitsgefĂ€hrdenden Legionellen-StĂ€mmen wird auf einfache Weise verhindert Kosten und Aufwand fĂŒr Laboruntersuchungen entfallen Vermeidung von hohen Ausfallkosten durch eine notwendige Anlagenreinigung nach einem möglichen Legionellen-Befall Automatische Protokollierung des pH-Wertes im Nutzwasser in ein Betriebstagebuch Geringer Überwachungs- und Wartungsaufwand Kein Aufwand bei Stilllegung zur Urlaubszeit sowie bei der Wiederinbetriebnahme danach Wir beraten Sie gerne weiter. Sie erreichen uns unter der +49 9533 924-333 oder per E-Mail: service-de@rosler.com .

Rösler cleaning centrifuge in the glass industry reduces costs by 90%

Easy operation thanks to fully automatic processing The automatic RZ 150 A is designed to handle a throughput of 150 liters per minute. In conventional systems the peeling knife, driven by a gear motor, is constantly rotating with the drum. In contrast to this the peeling knife of the Rösler RZ 150 A, located in the center of the sludge drum, is stationary. Only when the sludge deposits in the drum must be discharged, is the peeling knife moving towards the drum wall with a pneumatically actuated linear guide system. This allows peeling the sludge from the drum wall without placing any additional load on the drum bearings. After completion of the peeling cycle the drum is automatically rinsed to remove any residual sludge deposits. This prevents imbalances during the subsequent cleaning cycle, which could lead to premature wear of the drum bearing. The fully automatic process helps saving costs and reduces the consumption of valuable resources. Mr. Stepa, general manager of HART-SM, explains: „The new cleaning centrifuges helped us to reduce our energy consumption and achieve substantial cost savings. For example, we could reduce our idle machine times by 90 percent. And since only the water losses due to evaporation must be replenished, we could significantly reduce the costs for water exchanges. Last-but-not-least, we could reduce the monthly consumption of coolant from about 1,500 liters down to 150 liters, a reduction by nearly 90 percent. In addition to the considerable financial and technical benefits we also achieved a significant improvement of the water quality, an important factor for us as a progressive, future-oriented company. The water system is clean, because it is no longer overloaded with calcium. As a matter of fact, it is totally free of solid particles, which has an extremely positive effect on the overall quality of our products.” Mr. Stepa continues: “The cleaning centrifuge from Rösler represents an innovative solution that brings about a significant added value to our operation. And, of course, it is perfectly in line with our vision for a clean environment. We are pleased to have a company like Rösler as our reliable partner!” Rösler cleaning centrifuges – efficient and effective cleaning of industrial liquids Whether a company has to deal with coolants, sludge from paint processes, the water from industrial work piece cleaning operations or other process liquids, the treatment of the contaminated liquids always depends on the quality of the applied cleaning technology. No doubt the innovative, well-designed centrifugal filtering technology from Rösler offers excellent solutions. To achieve optimum cleaning results for the various industrial liquids, the centrifugal systems are specially adapted to the individual customer requirements. The Rösler centrifuges offer not only numerous technical and financial benefits, but through significant savings of water and other production materials they also help protect the environment. With decades of experience in the field of centrifuges Rösler is a competent, qualified partner for the efficient, energy-saving cleaning of all kinds of industrial liquids.

Mass Finishing Success Requires Constant Operational Focus

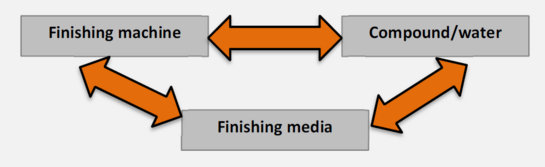
When most companies take on capital expenditure projects such as purchasing mass finishing equipment, very careful attention is paid to investing in the most productive, cost‐efficient equipment as possible to achieve the best possible quality. Operational efficiency is often another story. Once the equipment is up and running routine takes over and less attention is paid to keeping the equipment operating at its peak performance. Whether the machinery is never calibrated to reach its fullest potential or the on-going process is not carefully monitored once the process is dialed in, lacking operational focus can be costly and counterproductive. Figuratively speaking, poorly managed mass finishing operations are pouring money down the drain! Rosler works with its clients to ensure that our machinery delivers initial success and continues to provide precise, repeatable results long into the future by promoting operational attention and heading off costly mistakes. Consequences of Inattention For mass finishing processes, the lack of operational focus may take many forms individually or simultaneously, including: Reduced capacity because of processing times becoming unnecessarily longer. Overall poorer finishing qualities. Unstable processes with erratic finishing. Work pieces requiring additional reprocessing and higher rejection rates. Equipment not providing expected results and return on investment. Such operational deficiencies can cost a lot of money in the short-term when it comes to meeting client expectations and standards as well as the long-term life expectancy and usefulness of the process and machinery utilized. Identifying Issues and Opportunities Careful monitoring of the key process parameters, quick correction of any process abnormalities or “trouble shooting,” and regular preventive maintenance will ensure that a finishing process runs as intended in a cost‐efficient manner. Of course, this should not prevent a company from looking for further improvement and optimizing its current finishing operation. Technical upgrades or new, improved media and/or compounds may have become available for existing equipment which could help increase productivity, reduce costs, and improve the finishing quality. When working with a trusted partner and mass finishing expert such as Rosler, upgrades and advances can often be implemented without completely overhauling a process or purchasing entirely new systems. Optimizing Mass Finishing Operations Achieving the best results from a mass finishing process requires understanding the interaction between the various process components, including: The finishing machine itself. Compounds (liquids, recycling, powder, grinding, polishing, dry polishing, and cleaning/degreasing) and process water. Media – whether ceramic , plastic , or polishing and drying . The success of mass finishing depends on the successful pairing of machines, media, and compounds/water. The desired finishing results – deburring, edge radiusing, cleaning (de‐oiling, descaling) , and surface smoothing and/or polishing – can only be achieved if these process components are carefully calibrated with each other. More than a dozen factors are in play in a mass finishing process and enough complexity to warrant involving experts with experience. Process water from the finishing machine must also be addressed and monitored for optimum results. Depending upon the work piece’s material and original condition as well as the processes performed and consumables used, process water may be contaminated with media and metal fines, chemicals from the compounds, and even chelated metals. Before the process water can be discharged to drain or re‐used in the finishing process, it must be cleaned with a centrifuge . The Rosler Way With more than 80 years of experience, the Rosler team and worldwide Rosler Group have the knowledge and expertise to help you optimize your mass finishing process throughout the machine’s life cycle. Whether you have our equipment or a competitor’s, contact us for advice, sales, and service.

Automation Part 7 – The Top 3 Mass Finishing and Shot Blasting Machines

Rosler understands that automating aspects of your mass finishing and shot blasting processes has never been more critical. As we have learned during recent world events, outside factors can have a significant impact on your ability to maintain a largely manual process. Though automated mass finishing and shot blasting machinery does require some human intervention, it can often be operated with a minimal headcount and limited human contact. In previous blogs, we have explored how an automated-first posture can help you to gain significant efficiencies, lower costs, and increase your competitive advantage. We have also looked at the balance between automation and the environment and have discussed ways that you can mitigate environmental impacts of operating automated mass finishing and shot blasting machinery. We now conclude our Automation Blog Series with best practice examples of automated mass finishing and shot blasting machines Rosler offers and the associated accessories and components available to help in building your next-generation automated processes. Mass Finishing Automated Dual Rosler Drag Finishing Systems for Tool Bodies This drag finishing system is particularly useful for finishing of milling tool holders where work pieces are de-oiled, deburred, smoothed, and polished. Work stations equipped with drag finishing equipment feature special quick-connect couplings to expedite the work of robots to load and unload work pieces. Automated Dual Rosler Drag Finishing System pictogram As seen in the pictogram, a robot picks up the work pieces from a staging pallet and transfers them to the first R 6/1000 SF machine in a precise location with an accuracy of 4/1000 th of an inch (= 0.1 mm). Work pieces are then moved to a second R 6/1000 SF for smoothing and polishing before the robot moves pieces to a second staging pallet upon completion. Automated R 6/1000 SF Drag Finishing System This fully automated process is complemented by the Rosler Z1000 centrifuge for water cleaning and recycling. In order for precise finishing results, the work surface must be smooth, clean, and free of nicking and scratching. Walter Tools CNC milling cutter head processed by the Rosler Dual Drag Finishing System 2. Linked Dual Rosler Centrifugal Disk Finishing Systems Also known as the FKS 15.1 A2 , this system is used in the finishing of special stampings with a focus on the de-oiling, deburring, and edge radiusing of disk springs, rings, and washers. An example of work pieces processed by the Rosler Automated FKS System With a fully automated operation, the system handles the complete loading, unloading, transporting, washing, and drying of parts and media mixes – concluding with the backfilling of the finished parts into waiting bins. Linked Dual Rosler Centrifugal Disk Finishing System pictogram This process ensures batch integrity as long as individual batches are not mixed up in the screening machine and are completely oil-free with a defined edge radius prior to entering the machine. Automated FKS System also known as a Linked Dual Centrifugal Disk Finishing System 3. Rosler Linear Continuous Flow Vibratory Systems for Metal Parts Rosler’s linear continuous flow vibratory systems manage the de-oiling and deburring process for a wide variety of stampings. Work Pieces processed by a Rosler Linear Continuous Flow Vibratory System In the example below, parts are dumped en masse into the vibratory feed hopper by a forklift equipped with a fork rotator. The machine then places the empty part bin behind the hot air drier while the work pieces progress through the system in a fully automated manner. Rosler Linear Continuous Flow Vibratory System pictogram Batches must be processed separately, and parts must be free of oil for maximum throughput. Automated Rosler In-line DA System with parts loader and dryer Shot Blasting Rosler RROB Roboblaster for Cylinder Heads Rosler RROB Roboblaster with parts transportation system Able to precisely clean, de-sand, and deburr cast aluminum components, Rosler’s RROB Roboblaster is ideal for cylinder heads. Cylinder head processed by the Rosler RROB Roboblaster Its process begins when raw cylinder head castings are staged on two roller conveyors connected with a 90-degree turntable. Next, a robot equipped with a rotating device selects individual castings and suspends them into the machine. As the robot rotates the raw cylinder head, the blasting process takes place on all exposed surfaces. Finally, the robot places the finished cylinder heads into a screen drum for shaking out of residual blast media. Rosler RROB Roboblaster pictogram 2. Rosler RMBC 8.2 Tumblast Machine for Forged Components Part of Rosler’s Tumblast offerings, the RMBC 8.2 machine is particularly useful in descaling a wide variety of different forgings, including high volumes of bevel gears, in preparation for machining. Work pieces processed by the Rosler RMBC 8.2 Tumblast Machine An operator places two bins with raw parts into the skip loader after which empty bins are placed on a chain conveyor. Following shot blasting within the machine, finished parts are dumped onto a vibratory hopper, which tumbles, then automatically returns the finished parts into the waiting bins on the chain conveyor. Rosler RMBC 8.2 Tumblast Machine pictogram As with other automated machinery, it is critical to load distinct batches individually and to ensure the parts are free of scale. Rosler Automated RMBC 8.2 Tumble Belt Blast System with parts loading and unloading 3. Rosler RKWS 3 x 4 for Blast Cleaning of Crankshafts Rosler Automated RWKS 3 x 4 Cranksaft Blaster with robotic parts loading This particular model of the RKWS shot blast machine is equipped with three blast chambers arranged in a circle; each chamber is outfitted with four Gamma G blast turbines to accomplish the descaling process for crankshafts and other work pieces. Crankshafts before and after processing by RKWS A robot handles the loading and unloading of the parts, making this process fully automated. It’s important to note that piece weight is limited to a minimum of 14 lbs (6 kg) and maximum of 40 lbs (18 kg); after blasting the surface must be Sa 3 (white metal, no remaining traces of mill scale or rust allowed). Rosler Automated RWKS 3 x 4 Cranksaft Blaster with robotic parts loading https://vimeo.com/467660633 The Rosler Way By appropriately outfitting your operation with the right selection of automated mass finishing and shot blasting systems, you can be assured of gaining efficiencies and benefits that will help you maintain your competitive advantage. At Rosler, more than eight decades of experience and a constant drive to harness the latest advances allow us to design and manufacture innovative mass finishing and shot blasting solutions to fit your unique needs. Contact us today to learn how we can improve and automate your finishing system. The complete Automation Series includes: Part 1 – How Robots are Improving Mass Finishing and Shot Blasting Processes. Part 2 – Why Automation is Beneficial for Your Business. Part 3 – What Problems Do You Want to Solve? Part 4 – How Do I Select the Right Machine and Consumables? Part 5 – What Automation Hardware is Available? Part 6 – Environmental Considerations of Automation. Part 7 – The Top 3 Mass Finishing and Shot Blasting Machines. Sign up for enews alerts to be notified of all Rosler blog posts!

New Vibratory Finishing System Enhances Existing Material Handling & Drying Equipment

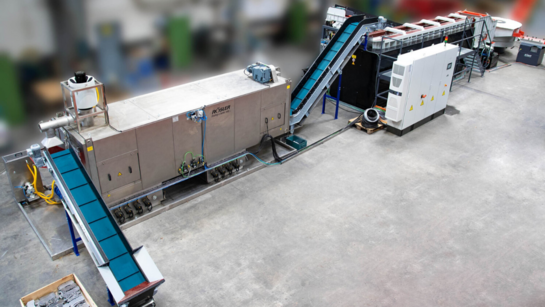
When it comes to high-volume production of complex aluminum die-castings, Kovolis Hedvikov a.s. (Kovolis) is a sought after partner by numerous car manufacturers and their suppliers. To expand its capacity and achieve more flexibility in the overall manufacturing process, the company purchased a continuous flow vibratory finishing system from Rosler designed to handle a wide work piece spectrum and custom engineered to fit into the available space at the customer’s premises. About Kovolis Founded in 1816 as an ironworking operation, Kovolis has focused entirely on aluminum die casting since 1945. Today, Kovolis produces components from nine different aluminum alloys weighing between 7 oz (200 grams) and 18 lbs (8 kg) with different casting technologies including vacuum investment casting and rheocasting. Their product range includes brakes, power steering systems, turbo chargers, and compressors for air conditioning systems. Kovolis customers are renowned car manufacturers and tier-1 suppliers that also utilize the company as an important partner for product development, machining, heat treatment, and surface finishing services. New Needs Call for a New System Jiri Buzek, manager of foundry III at Kovolis, explained the need for a new vibratory finishing system. “Our product portfolio underwent a drastic change in the past years. The trend goes more and more to larger and more delicate components, which require a vibratory finishing step after punch deburring for their downstream handling. Our existing finishing system was not designed for this and had also reached the end of its productive service life.” The new system not only had to cope with larger work pieces, but the finishing process also had to be a lot gentler. Additional customer requirements were high equipment uptimes and cost efficiency. And, above all, the new finishing system had to be integrated into the existing manufacturing operation, utilizing the existing work piece loading device and hot air belt drier. The planning engineers at Kovolis submitted these specifications to two German equipment suppliers. “We decided to go with the Rosler continuous feed vibratory finishing system, because it offers ample capacity, and Rosler met all our special technical requirements. Of course, the fact that our company has had excellent experience with other equipment from the same supplier certainly helped,” Buzek said. The single curve U-shaped cross section of the processing channel guarantees the optimum movement of the media and work pieces through the machine. Kovolis also appreciates that Rosler can supply the equipment as well as all compounds and finishing media needed. This allows the perfect adaptation of the finishing process to the customer’s work pieces. A Customized Solution The new finishing system consists of a linear continuous feed machine, type R 550/4600 DA, with a usable length of 15 ft (4.6 m). The functions of the existing work piece loading system and hot air belt drier were integrated into the overall system controls. “Rosler met all our technical requirements and provided valuable support in optimizing our finishing process,” Buzek said. The system offers a number of features and capabilities, including: Fully automatic feeding of the work pieces every 30 seconds. Accommodation of parts with diameters of up to 16 in (400mm). Adjustable processing times. Dual-stage separation with rinsing station. Process water cleaning with an automatic centrifuge. The processing bowl angle can be adjusted to change the processing time. Kovolis was especially impressed with the centrifuge technology Rosler offers. “In the past we cleaned our process water chemically or with a semi-automatic centrifuge. This was highly labor intensive and costly” Buzek said. “With respect to process water-cleaning, Rosler provided us again with the optimum solution. “We are certain that with the new equipment we will not only improve the quality of our finishing operation but, at the same time, will become more cost efficient.” The Rosler Way As the international market leader, Rosler offers total solutions in the field of mass finishing and shot blasting, painting and preservation systems, and mass finishing consumables. In addition, Rosler offers a broad spectrum of surface finishing technologies (deburring, descaling, desanding, polishing, surface grinding, etc.) for work pieces made from metal and other materials. Headquartered in Germany, the Rosler Group maintains sales and manufacturing branches in Great Britain, France, Italy, the Netherlands, Belgium, Austria, Serbia, Switzerland, Spain, Romania, Russia, Brazil, India, China, and the United States. Contact us to discuss how we can provide a customized solution to solve your unique challenges.
Forge & Foundry, Part 11 – Top Mass Finishing Machines for Cleaning Die Castings

Rosler Metal Finishing has decades of experience in the forge and foundry industries, especially when it comes to mass finishing for die-casted work pieces. Our Forge & Foundry Blog Series continues with an overview of our top five mass finishing machines for precise cleaning of die castings. Standard Rotary Vibrators Media and parts are placed into a circular processing bowl in standard rotary vibrators . The energy from a vibratory motor causes the media and parts to freely tumble over each other. Some models are equipped with an internal separation device for separating the finished work pieces from the media. Rotary vibrators can be used for batch and continuous feed processing. The R620 Euro is one of Rosler's standard rotary vibrator models Rosler’s standard rotary vibrator models include the models EC, Euro, A, and R. Ideal Work Pieces — Small to fist-sized die-castings such as shoe buckles, furniture fittings, gear shifter forks, electrical components Work pieces processed by one of Rosler's standard rotary vibrators Learn more about these machines in our Rotary Vibrator Guidebook (PDF) . Long Radius Rotary Vibrators Built upon the rotary vibrator technology, long radius machines feature much bigger overall diameter and larger processing bowls. The expanded processing area allows for considerably longer cycle times in continuous feed mode. Known as the LR models at Rosler, these machines allow for batch and continuous feed processing. Rosler's LR models are long radius rotary vibrator machines Ideal Work Pieces — Small- to mid-sized die-castings including small gear boxes, bearing housings, mirror frames for cars, all kinds of engine and transmission components Work pieces processed by one of Rosler's long radius rotary vibrators Learn more about Rosler’s LR capabilities in our Long Radius Guidebook (PDF) . Multi-Channel, Continuous Flow Rotary Vibrators The major difference between a multi-channel, continuous flow rotary vibrator and a standard rotary vibrator is the processing channel’s spiral arrangement to create extremely long processing channels of up to 31 ft (9.5 m). The unique channel design draws work pieces apart so they almost never touch each other during the finishing process and always features continuous feed processing. Rosler’s linear, continuous flow vibrators are known as the SE models. The Rosler SE model is a multi-channel rotary vibrator Ideal Work Pieces — Small to mid-sized somewhat delicate components, particularly parts with critical sealing areas that must not be damaged including parts for espresso machines and model train cars Model train cars processed by one of Rosler's Multi-channel continuous flow rotary vibrators machines More information is available in our Multi-Channel Continuous Flow Systems Guidebook (PDF) . Linear, Continuous Flow Vibrators Powerful vibratory drive systems are mounted underneath rectangular processing bowls in linear, continuous flow vibrators. They always feature continuous feed processing. Known as DA models at Rosler, these machines are the largest and most powerful mass finishing machines available. Rosler's linear continuous flow vibrator machine offerings include this DA 650 6600 Ideal Work Pieces — Mid-sized to large, somewhat sturdy, die-castings that are not damaged by tumbling over each other including power drill housings, cylinder head covers, oil pans, transmission housings, disks for automatic transmissions Impact wrench housings processed by one of Rosler's linear continuous-flow vibrators Learn about Rosler’s DA capabilities in our Linear, Continuous Feed Systems Guidebook (PDF) . Tub Vibrators Similar to linear, continuous flow vibrators, tub vibrators feature rectangular processing bowls with a powerful vibratory drive system mounted underneath. Tub vibrators are available in a wide range of sizes from very small to extra large, allowing the processing of a wide work piece spectrum, from small to very large, up to 10 ft (3 m) long and 5 ft (1.5 m) wide. Rosler offers several tub vibrator models including the TE, Compact TE, TSD, TU, TUD, TUM, and RMO, all of which feature batch processing. The Rosler TUM is one of Rosler's tub vibrator machine offerings Ideal Work Pieces — Large housings, large light casings, structural airframe parts, or smaller parts in low to medium production volumes A large die cast cover processed in one of Rosler's tub vibrators Learn more about Rosler’s various tub vibrator models and capabilities in our Tub Vibrators Guidebook (PDF) . The Rosler Way The Rosler team is uniquely capable to solve mass finishing challenges, especially when it comes to die castings. Contact us to share your needs so we can develop a solution. The complete Forge & Foundry Series includes: Part 1 – Shot Blasting Systems. Part 2 – Efficient Recycling. Part 3 – Shot Blasting & Sand Castings. Part 4 – Selecting a Shot Blasting Machine for Sand Castings. Part 5 – Cleaning Features & Dust Precautions for Sand Castings. Part 6 – Selecting a Shot Blasting Machine for Die Castings. Part 7 – Selecting a Shot Blasting Machine for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 8 – Frequently Used Shot Blasting Machines for Sand Castings. Part 9 – Frequently Used Shot Blasting Machines for Forgings, Non-Sand Castings, and Powdered Metal Components. Part 10 – Shot Blasting Machines Commonly Used for Die Castings. Part 11 – Top Mass Finishing machines for Cleaning Die Castings Part 12 – Media and Compound Selection, Effluent Handling Drive Success Sign up for enews alerts to be notified of all Rosler blog posts!

Automation, Part 6—Environmental Considerations of Automation

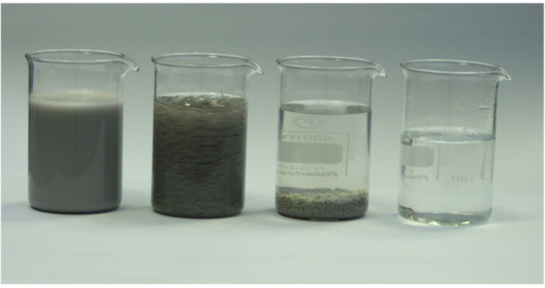
Technology has transformed almost every aspect of life and the shop floor is no exception. As explored in previous Automation Blog Series posts, Rosler Metal Finishing believes automation represents the new norm in mass finishing and shot blasting . In the face of increasing competition, manufacturing interests will continue to demand lower cost, higher efficiency, and greater flexibility from their chosen surface finishing partner. Though it would appear that any downsides of automation are outweighed by its benefits, there’s a delicate balance to be struck when it comes to a symbiotic relationship with the world outside of the machine. Having previously discussed how human effort and ingenuity will work in harmony with automated processes, we now turn our attention to environmental considerations—namely, how automated machines used in mass finishing and shot blasting can impact the earth’s resources, and how manufacturers can mitigate that impact. The International Institute for Sustainable Development notes that the rise of automation has thrust us into a “Fourth Industrial Revolution,” citing energy use, resource use, and ecosystems as the three most critical factors to watch as more automated processes are implemented. These are important considerations, given that manufacturers often are targeted in headlines about waterway pollution and even global warming, but responsible manufacturing practices can help avoid the most egregious impacts and keep manufacturing operations in compliance. Process Water Handling In the process of mass finishing and wet blasting, the biggest consideration is with regard to the process water discharged from the finishing machines. Often, this water is tinged with metal and media fines; at times, it can also contain oil and dissolved metal. Of course, process water will carry the compound being used in the specific finishing process. Mass finishing process water in different cleaning stages. So how can operators of automated mass finishing machinery take special consideration to limit the contamination of any process water discharged from the plant? There are two main ways to effectively curtail such constituents. Central Treatment The establishment of a protocol that includes a central wastewater treatment plant is quite effective in removing contaminants. Also, such facilities require fewer dedicated staff members, which adds to the efficiency of this approach. Centrifuges This universal cleaning system is deployed to separate, purify, extract, and wash various materials using centrifugal force to generate 2,000 times the earth’s normal gravity. These systems also require little operator attention, can be acquired in completely automated or semi-automated configurations, and can be used for most standard mass finishing applications. Rosler offers two centrifuge models; the semi-automatic Model Z 800 and the fully automatic Z 1000. Rosler's Z 800 centrifuge is semi-automatic. Rosler's z 1000 centrifuge is fully automatic. With the right approach to treating discharged process water, you can ensure you are a good steward of your environment, while also maximizing the efficiencies and benefits to be gained from automating your mass finishing and wet blasting operations. The Rosler Way The experts at Rosler are uniquely qualified to develop an automated finishing process for your surface finishing needs that is both effective and ecologically responsible. Contact us to get started today. In the next installment of the Automation Blog Series, we’ll look at the equipment that best positions your business for successful automation of your mass finishing and shot blasting operations. The complete Automation Series includes: Part 1 – How Robots are Improving Mass Finishing and Shot Blasting Processes. Part 2 – Why Automation is Beneficial for Your Business. Part 3 – What Problems Do You Want to Solve? Part 4 – How Do I Select the Right Machine and Consumables? Part 5 – What Automation Hardware is Available? Part 6 – Environmental Considerations of Automation. Part 7 – The Top 3 Mass Finishing and Shot Blasting Machines. Sign up for enews alerts to be notified of all Rosler blog posts!

Rosler & Lumag – Combining Multiple Solutions in a Single Finishing System

Finding a solution to our clients’ needs is nothing new for Rosler , nor is combining multiple solutions into a single finishing system. Take our work with Polish brake pad manufacturer Lumag Sp. z o.o. (Lumag) , for example. When they faced the challenge of de-oiling, deburring, and surface roughening brake pad carrier plates as part of their punch press process, they turned to us for a cleaning and mass finishing solution. The Situation Upon its founding in 1988 by Marek Zak, Lumag specialized in the production of brake linings. As the company implemented its own brake pad manufacturing technology, their products and offerings evolved. In addition to achieving enormous technological progress and applied engineering solutions, Lumag amassed a collection of machinery in need of constant upgrades and integration. In order to meet the continuous rise of quality and safety standards for its brake pads for drum and disk brakes for commercial vehicles as well as brake pads for passenger cars and motorcycles under the trade name Breck , Lumag needed a partner with automotive expertise who could combine multiple solutions in a single system. De-Oiling, Deburring, and Surface Roughening With the change of its production method for the brake pad carrier plates from casting to stamping , Lumag decided to install a new in-house manufacturing line for these products. The new system must allow for stamped carrier plates with lengths of 8-10 in (210-250 mm) and widths of 3-5 in (90-110 mm). The work pieces also have a slit or drilled hole to allow a sensor to monitor brake pad wear after installation and must undergo de-oiling, deburring, and surface roughening during the finishing process. These steps are necessary to ensure that the delicate stampings provide optimum adhesion characteristics for the subsequent bonding of the brake pads. Another requirement presented by the customer was to directly link the finishing equipment with the punch press while providing extremely gentle processing and the complete automation of the cleaning (de-oiling) and mass finishing stages in a continuous feed operation. In addition to an excellent reputation in the industry, Rosler’s ability to supply the equipment for both processes and the finishing media and compounds from one single source was a bonus for Lumag. Intelligent Media Selection Allows for Cleaning Without Drying After the stamping process, a conveyor belt transfers the work pieces to the drum washing machine equipped with an internal transport auger. In the drum the carrier plates initially pass through an un-perforated zone into which cleaning liquid is applied by spray nozzles. This creates an immersion bath for de-oiling. In the following perforated drum section, the cleaning liquid is drained, and in a secondary de-oiling step the work pieces are spray washed. This cleaning zone is followed by a drip-off section, a rinse station, and another drip-off section. Complete Rosler system with transport container Subsequently, a conveyor belt transfers the work pieces into the mass finishing machine. Replenishment of the cleaning liquid takes place with a Dosatron proportional dosing pump. Since the cleaning liquid and the compound for the mass finishing process have practically the same chemical characteristics—including the placement of a temporary corrosion protection—carryover of the cleaning liquid into the mass finishing machine presents no issue. This clever trick eliminated the need for a drying stage after the cleaning process, resulting in significant savings in the overall capital expenditure as well as reducing operating costs. For proper maintenance of the cleaning liquid the washing machine is equipped with filtration units and an oil separator. Gentle Mass Finishing Deburring and surface roughening of the work pieces takes place in a linear, continuous flow vibrator R 550/6600 DA with a specially adapted work piece loading system. Loading actually takes place at the rear end of the processing bowl instead of on the lateral bowl side with greatly reduced dropping heights. Similar gentle work piece transfers were incorporated in the vibratory screening unit and the drier filled with Supervelat drying media. After drying a certain work piece quantity based on precisely measured weight, components are discharged into a transport bin. The process water from the mass finishing machine is continuously cleaned in a fully automatic peeling centrifuge Z 1000 equipped with automatic sludge discharge. The Rosler Way Whatever challenges you face in surface finishing, Rosler is eager to find a better way both individually and as a whole. With more than 80 years of experience, we have the knowledge and drive to continually learn about, develop, and deliver precise solutions. Contact us to discuss your unique challenges and how we can innovate a solution for your needs and goals.